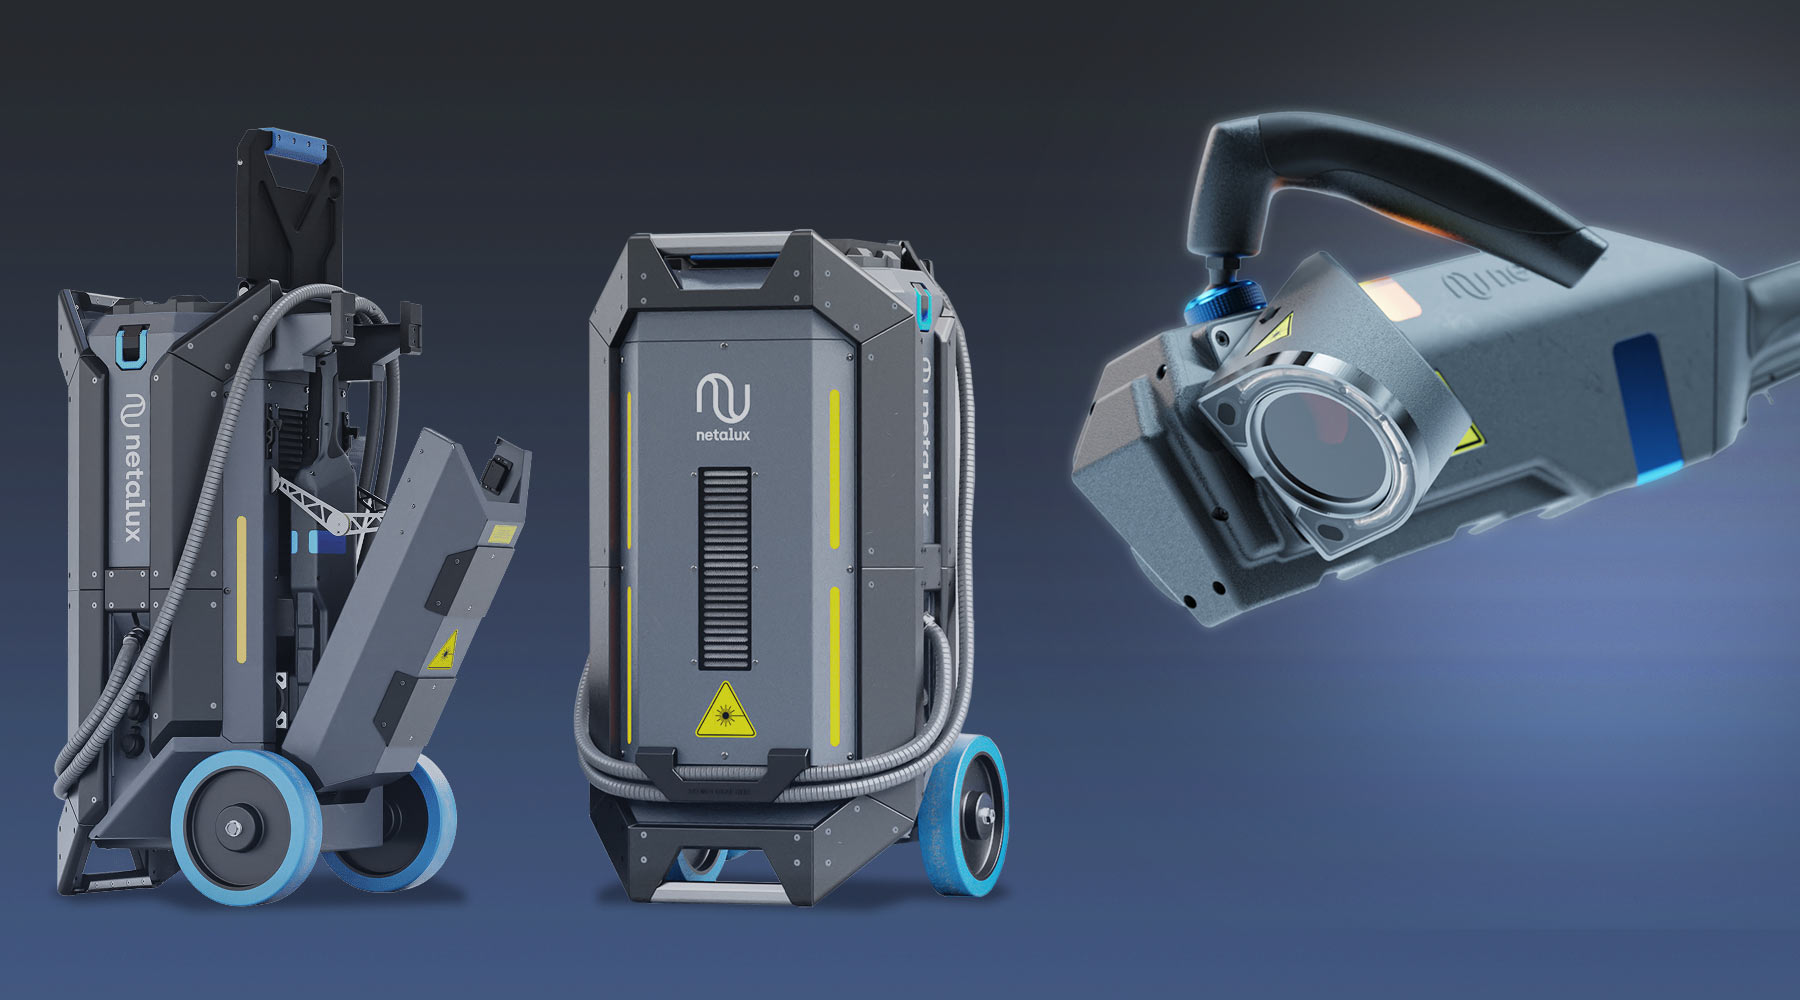
This is the machine for a home, a small shop, or a detailed part, including a tight space. Furniture, doors, rails, wood finishes, light automotive, weld prep, oxide and weld discoloration, selective paint, grease, and small molds or tools. The same pass can clean a part before inspection, coating, or bonding. You run it yourself after the lesson. It is a 300 W air-cooled top-hat pulsed laser, about 95 lb, with about 18 ft of fiber. Large industrial surfaces and heavy-duty automotive belong on the Dagger 4000.
Medium Duty rates for Rent the Kamino for the day, but use it all you want until pickup the next day
Rent the Kamino for the day, but use it all you want until pickup the next day
You pay for the reserved slot, not for each hour you run the laser. Machine use inside that window is unlimited, so you can take the time the part needs. Getting the project done right matters more to us than packing up early, and the extra hours are there so you can finish that way.
Wood
The carving stays sharp, and the grain is not sanded. Stain and varnish lift off a deck, door, table, or carved rail without a chemical stripper soaking in.
Illustration for workflow step: Wood. Teak with a laser-cleaned section beside the remaining finish
Illustration for workflow step: Masonry. Historic masonry cleaned by laser
Masonry
Tool marks and mortar lines stay. Paint and weather stains leave brick, granite, marble, and concrete without the wear blasting and grinding leave behind.
Rust
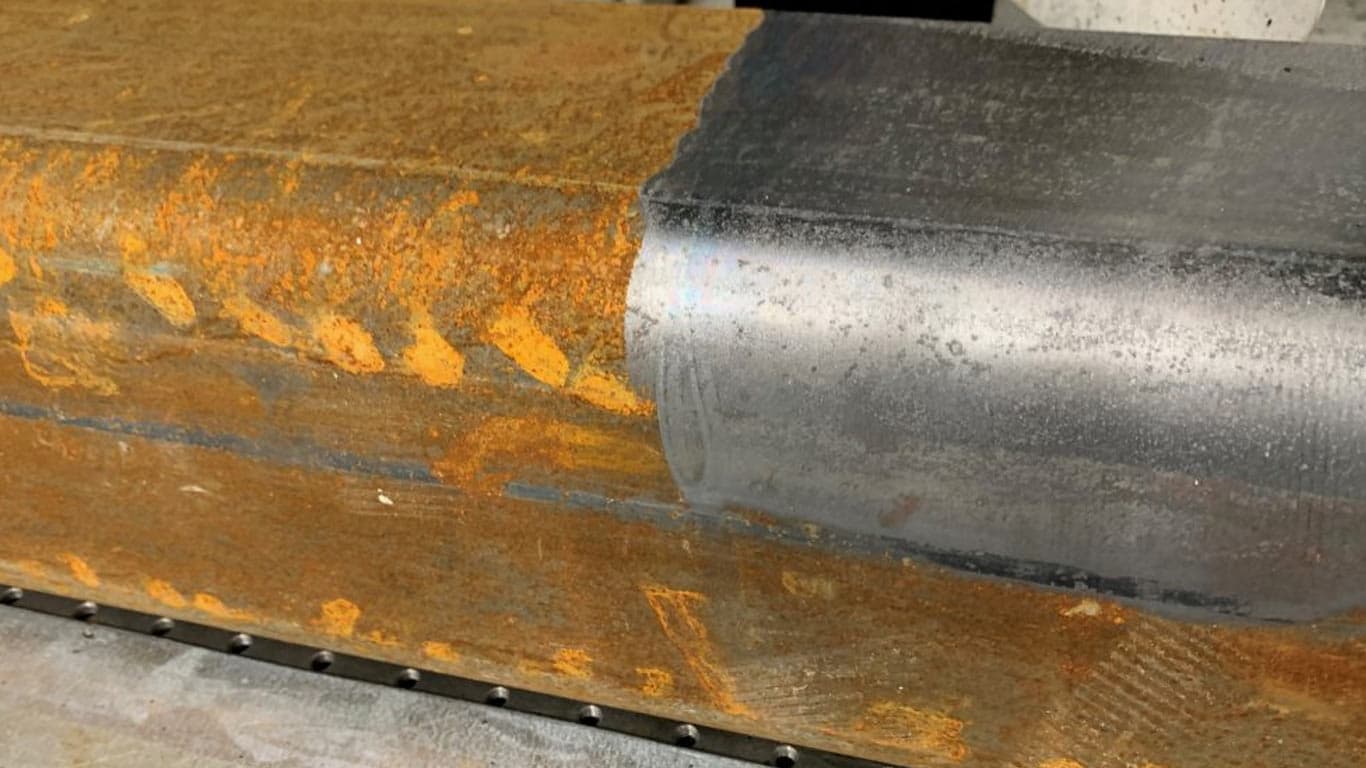
The steel stays ready to inspect, coat, or bond. Surface rust, mill scale, and weld discoloration leave doors, rails, hardware, and light automotive parts without a ground profile or blast media.
Illustration for workflow step: Rust. Steel after laser rust removal
Illustration for workflow step: Paint. Metal part during laser paint removal
Paint
Paint comes off without cutting into the metal. On a gate, railing, or metal part, the coating leaves without a ground profile or chemical stripper residue.
Compliance
Z-Beam runs this equipment under Cal/OSHA and OSHA with trained operators, eyewear, placards, and respirators for lead or chromate. ANSI Z136.1 sets Class 4 controls. California DTSC covers dust and filters. Source capture and BAAQMD confirmation come before Bay Area jobs. CARB covers generators. FDA CDRH interlocks stay on.
Wood finish tests
If the coating on the wood is unknown, run one test the day before. Water-based polyurethane and acrylic lacquer sit on the surface and reflect the beam, so the wood underneath can overheat before the coating lifts. Either test is enough.
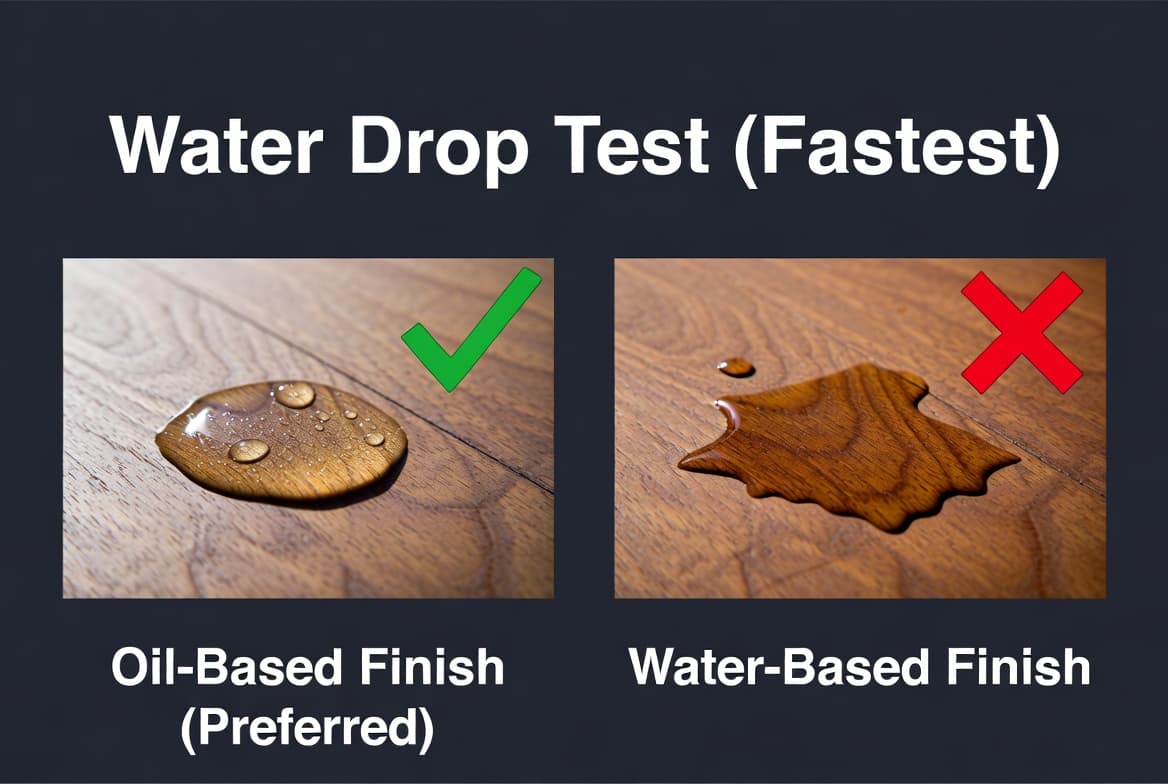
Water drop test
Place one small drop of water on an inconspicuous area and wait 60 seconds. A water-based finish (polyurethane, acrylic lacquer) will bead or sit on the surface. An oil-based finish or bare wood will absorb it quickly, darkening the grain.
Illustration for workflow step: Water drop test. Water drop test on wood to identify finish type
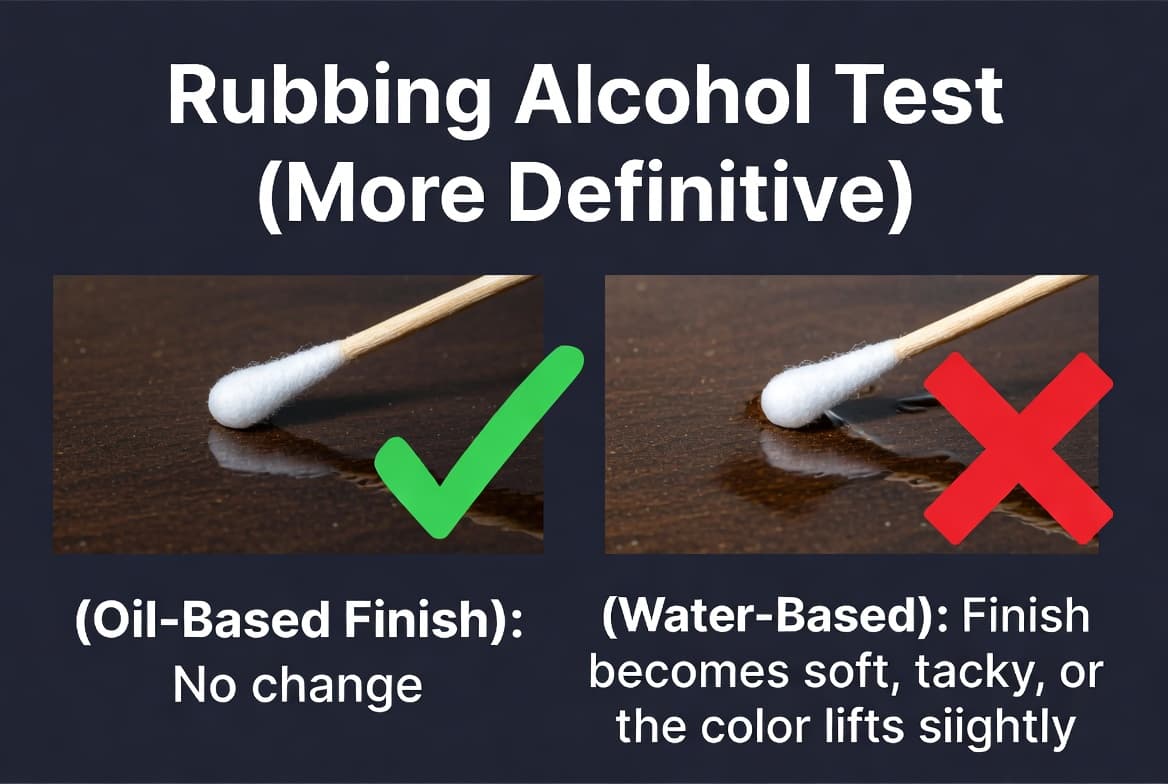
Illustration for workflow step: Alcohol swab test. Alcohol swab test on wood surface to identify shellac or lacquer finish
Alcohol swab test
Dampen a cotton swab with 91% or higher isopropyl alcohol and rub a small hidden area firmly for 10 seconds. Lacquer softens and smears. Polyurethane and conversion varnish show no effect.
Shellac and soft lacquer need the lowest energy of any wood finish. Naming them ahead of time keeps decorative and antique pieces from scorching.
Technical specifications
Figures below are from the Kamino UMHW V1 EN technical specifications section.
Laser source
Laser source
Laser type
Class 4 nano-second pulsed ytterbium fiber laser
Wavelength
1064 nm
Pulse frequency
2–4000 kHz
Pulse length
20–500 ns
Pulse shape
Top-Hat
Maximum pulse energy
10 mJ
Laser class
4
Average laser power
300 W
Average electrical power
1150 W
Cooling
air cooled
Display
hardened glass
Electrical supply
Electrical supply
Supply
1P + PE | 110–240 V | 50–60 Hz | 11 A–5 A
Plug
C13 IEC connector (local adapter as needed)
Dimensions and fiber
Dimensions and fiber
Total weight
about 43 kg / 95 lb
Laser unit
40 kg / 88 lb
Handset
2.5 kg / 5.51 lb
Laser unit
43.1 × 34.0 × 81.2 cm
Handset
57.1 × 17.9 × 10.8 cm
Fiber length
5.7 m / 18.37 ft
Protective hose diameter
25 mm
Minimum fiber bend radius
120 mm
Environment
Environment
Humidity
non-condensing
Ingress protection
IP44 (transport note: IP51 upright only)
Temperature
0–35 °C
—
No significant vibration
Before you start
Complete training before use. Keep this documentation available to every operator. Netalux Academy details are at netalux.com/academy.
Rules that apply every shift
Wear appropriate laser safety glasses whenever the laser can emit.
Read and understand the operating instructions and safety guidelines before powering on.
Netalux assumes no liability for unintended use or skipped safety instructions.
General safety
Netalux is not liable for damage to products or installations caused with the machine, or for injury to persons caused with the product.
Core warnings
Use only the controls and procedures in the manual. Other adjustments can cause hazardous radiation exposure.
Inspect for damage, unusual noise, or cracked cord or fiber before each use. Do not run a damaged machine; contact Netalux immediately.
Do not use in ATEX zones or under water. Clear highly flammable products before lasering.
Wear EN207 laser safety glasses matched to machine power.
Always aim at a surface. Do not fire into open air. Never irradiate people.
Do not leave the machine unattended. Power off fully and remove the key when leaving.
Complete a risk analysis before service, including door interlocks and safety curtains. Interlocks must be closed to reset and emit.
Maintain proper grounding and stable voltage. Spikes or ground faults can damage the laser source.
Do not crush the fiber protective hose. Report damage to Netalux Support.
Personal protection and work zone
Eyelids do not protect against laser light. Collective measures and PPE stay on until the machine is fully off.
PPE and clothing
Never remove laser safety glasses during laser work. Bystanders need the correct glasses too.
Never look directly into the beam, even with glasses on.
Wear safety shoes and clothing that the beam must not damage; avoid reflective jewelry and watches.
Gloves can heat and burn; check personal and collective PPE before emission and replace damaged gear.
Demarcation
Under European Directive 2006/25/EC, demarcate the laser cleaning zone with a laser safety screen, marking tape, and warning signs so only authorized people enter.
Laser safety
Class 4 laser products require a risk analysis and preventive measures before use (EU Directive 2006/25/EC). Incorrect use can cause permanent blindness, skin burns, short circuits, or uncontrolled emission.
Fiber and intended use
If the fiber protective hose is cracked or internal cables are visible, stop, power off, and contact Netalux Support.
Wear correct PPE at all times. Laser light harms eyes and skin.
Use only for the intended purpose. Incorrect use can permanently damage the machine and void the warranty.
Glasses must match power and at least EN207 at 1064 nm. Welding goggles do not qualify. Confirm with your supplier.
Extraction, room preparation, and operators
Extraction protects people, cleaning quality, the debris shield, and optics. Poor extraction can void the warranty.
People and fumes
Tell nearby people you are lasering; keep the safety zone clear unless authorized.
Anyone entering with permission wears PPE from the task risk analysis.
Know the contaminant; provide respiratory or chemical PPE as required.
Extract fumes and particles promptly. Dispose of collected particles per local law.
Room and operators
No mirrors or highly reflective surfaces; protect paintings and glass; use wavelength-safe window treatments.
Prefer fire-retardant curtains (EN 60825-1 when possible); keep the beam off paper and plastic.
Operators must be trained under Directive 2006/25/EC and in good physical and mental condition. Never allow untrained operators.
Emergencies
The emergency stop sits on top of the laser unit at the top left of the display. Push it to cut laser-source power and stop emission. Unit and handset lights turn red; the display shows e-stop active.
Restart and interlock
When safe, quarter-turn the e-stop to normal; the reset button goes green and lights return to green.
Never use the emergency stop as a normal power-off; repeated use can permanently damage electronics.
The external interlock at the bottom connector panel can act as an e-stop for site systems (line e-stop, light curtain, door). Open interlock interrupts emission; close it before reset.
Handset arm/disarm is not an emergency stop. It returns the laser to safe mode for a normal pause. Use the dedicated e-stop for a full shutdown.
Product overview
A pulsed laser source feeds the handset through fiber. Cleaning uses pulsed laser ablation: the pulse interacts with contaminant and substrate so the film releases.
Intended use
Derusting, paint stripping, degreasing, process contamination or coating removal, mould cleaning, and weld cleaning
Professional use only; Class 4 is not for private persons
Mobile multi-site setup, not a fixed installation
Main components
Main components
Laser unit
source, electronics, ventilation, HMI, alarms, and e-stop
Handset
where the beam exits
Fiber
connects unit and handset (do not crush)
Laser unit
Air-cooled with ventilation and filter. Do not unscrew the machine; call Netalux Support for internal problems. Lift only at both attachment points together with approved lifting gear.
Fiber support and fiber; connectors; emergency stop; display
LED indication lights; ventilation
Indicator lights
Indicator lights
White
booting
Green
ready to reset / ready to arm
Orange continuous
ready for emission
Orange flashing
emitting
Red
alarm (e-stop or interlock)
Connectors and service access
Connector panel at the laser unit. Service access is for Netalux technicians only.
Panel labels
a. AC in with LED indicator
b. Fuse
c. External lighting / external LED
d. External I/O
e. External interlock
f. Compressed air / air in
g. Service (technicians only)
h. USB interface
User interface
HMI on the laser unit controls power, jobs, and arming.
Controls
Controls
Emergency stop
immediate stop; lights red; quarter-turn release when safe
Key switch
quarter turn right on; left and remove off
Display
jobs; pulse energy, pattern size, pulse overlap; temperature and status
Slide control
fine parameter changes
Arm/disarm
green when booted; touch for ready-for-emission
Alarm symbols
General, Maintenance, Temperature, Power supply, Humidity (plus laser-danger labeling on the product diagram)
Handset
Indicator lights on the handset stay synced with the unit. Clean the debris shield (protective glass) regularly and after every job; dirt can seriously damage optics.
Parts and motion
Rotatable laser head (about 115° on the detail page; one optic-unlock diagram cites about 185° freedom)
Secondary handle 360°
Control screen; arm/disarm; selection buttons
Trigger with forward release; fiber (do not crush)
Improper use risks injury and uninsured machine damage. Netalux is not liable for incorrect use.
Do not
Treat textiles or other energy-absorbing or flammable surfaces
Irradiate any part of the human body or use for medical or cosmetic procedures
Use for household or private cleaning, under water, or in ATEX zones
Run without extraction, with covered air inlets, or on an unstable or unsecured elevated surface
Embed or modify the machine without written Netalux consent
Allow untrained operators (including children, elderly, or people with disabilities who are not trained operators)
Use as a heat gun, ignition source, cutter, or welder
Fire into thin air or onto translucent surfaces
Crush, run over, or stand on cables; skip guarding or a demarcated safety zone
Training
Only trained operators. Directive 2006/25/EC requires machine and safety training; local rules may add more. Netalux trains purchasers with safety emphasis; Netalux Academy covers deeper training. Appoint a Laser Safety Officer.
Turning on and using the machine
Complete safety training (Chapter 2) and prepare a demarcated zone with no mirrors, chrome, or textiles before these steps. Wear glasses while the machine is activated; never look into the laser head.
Startup steps 1–8
1. Remove from the transport case onto a stable surface.
2. Park the handset on the ground with the head safe (about 45°); not at ground, body, or flammables.
3–4. Connect power; the AC-in LED must light.
5. Key quarter turn right.
6. Wait for home; green lights and green reset when ready.
7. Confirm e-stop is in the normal position.
8. Put on laser safety glasses.
Emission steps 9–14
9. Touch reset/arm for ready-for-emission (button red; unit and handset orange; headlight on; default first job).
10. Aim at the surface with the correct distance, lens, and angle.
11. Unlock the trigger; first click shows the red aiming laser pattern.
12. Second click starts the IR cleaning laser; lights flash orange; hold distance.
13. Change job only after releasing the trigger (handset arrows or unit display).
14. Rotate the head via the lock only with people and flammables out of the new path.
Switching off, head angle, and lenses
Shut down in order. Do not unplug while the display is still on.
Shutdown steps
1. Release the control button.
2. Stop emission with the red reset/arm on the handset or unit.
3. When lights are green, turn the key off and remove it.
4. Wait until display and lights are fully off before unplugging.
5. Remove the power cord.
6. Clean protective glass if dirty.
7. Return unit and handset to the transport case.
Rotatable head
Slide the lock outward, hold, twist the head, release. This improves ergonomics and helps avoid direct back-reflection into the optic (can cause irreparable non-warranty damage).
Lenses
Available lenses: 240 mm, 285 mm, 415 mm, 650 mm
Shorter lens means tighter focus, higher energy density, and deeper heat; high power with a short lens can micromelt
Install lens ART01331 with the curved side to the back
Selected lens shows on the LED display; change with the handset lens control
Ergonomic handle and forced air
Knurled ring clockwise to unlock and position; anti-clockwise to tighten (use the key provided).
Forced air when optic temperature exceeds about 50 °C: 8 mm OD push-in; factory regulator about 4 bar; adjust 2–5 bar (max 5).
Dry oil-free air only; max 8 bar; depressurize before connect or disconnect; avoid tiny hot domestic compressors.
Maintenance
The second alarm symbol turns orange when maintenance is due; follow the display and Chapter 8. Advise at least a yearly Netalux Support visit (support@netalux.com, +32 11 661 882). No user repairs.
Protective glass and filters
Keep protective glass clean. Replace if deep scratches, cracks, or uncleared dirt remain. Do not laser through dirty glass.
Replace bottom ventilation filters when the display prompts.
Internal optics and disposal
Internal optics and disposal
Internal optics
check every six months by Netalux or certified service points.
Disposal
recycle per local law; not household waste.
Reception, storage, and transport
Inspect the shipment before first use. Power off before casing.
Included items
Manual
Laser unit, handset, and fiber
Transport box
Extra plugs and cord
Key
Cleaning kit
Laser safety glasses (2)
Storage and moves
Clean before store (damp cloth with mild soap; isopropanol on protective glass). Store non-condensing, about −10 °C to 50 °C. Use the transport case. IP51 applies upright only; protect openings if the unit is laid down.
Accessories
Extraction, PPE, and screens are part of safe operation.
Suction nozzle and vacuum
Fit adapter plates on the moving head and left shell; snap nozzle and hose; set the extendible tip close to the work.
Standard nozzle suits about 300–350 mm focal setups; shorter focus may need a custom length.
Remove via red quick-lock tabs.
Vacuum suggestion (non-binding): more than 3 kW and about 23 kPa underpressure; size filters to the contaminant risk analysis.
PPE and screens
Wear EN207/EN208 glasses matched to wavelength and power. Hearing protection is strongly recommended. Demarcate with a laser safety screen that meets EN 60825-4.
Troubleshooting alarms
Alarm families on the UI include General, Maintenance, Temperature, Power supply, and Humidity. Orange or blue is non-critical (laser may keep running). Red is critical until you clear the display steps. Unknown messages: contact Netalux Support ASAP.
Common meanings
Common meanings
General orange/red
explanation on screen; follow the screen or call Support
Maintenance orange
schedule maintenance with Support
Temperature blue
not warm enough, wait; orange: too warm, wait; red: critical rapid heat, call Support ASAP
Power supply red
supply not working, call Support ASAP
Humidity orange
approaching maximum; stop and move to a drier area
Message on screen with no lit symbol
follow the display or call Support
Related materials
Ranked by evidenced affinity (more stars = stronger fit for this machine).
What is the Netalux Kamino-300 laser cleaning system?
The Netalux Kamino 300 is an air-cooled Class 4 nano-second top-hat pulsed ytterbium fiber laser cleaner at 300 W average power and up to 10 mJ pulse energy (1064 nm). It is a mobile standalone tool with a fiber-fed handset for professional on-site cleaning. Z-Beam includes delivery, setup, and operator training with rental.
What are the key specifications of the Netalux Kamino-300?
300 W top-hat pulses; up to 10 mJ pulse energy; 2–4000 kHz; 20–500 ns; 1064 nm; air cooled; IP44; about 43 kg total; fiber about 5.7 m; supply 1P+PE 110–240 V 50–60 Hz with a C13 plug.
What materials and applications is the Kamino-300 best suited for?
The manual lists intended professional uses as derusting, paint stripping, degreasing, process contamination or coating removal, mould cleaning, and weld cleaning. Related materials and applications on this page are ranked by evidenced affinity, not as a claim that every substrate is equally easy.
What power requirements does the Kamino-300 need on job sites?
The Kamino 300 runs on single-phase 110–240 V (1P+PE, 50–60 Hz, C13). A normal grounded 110 V outlet is the usual rental setup.
How do I maintain the Netalux Kamino-300?
Keep the protective glass clean and replace it if scratched, cracked, or still dirty. Replace ventilation filters when the display prompts. Follow orange maintenance alarms on screen. Netalux advises at least a yearly support visit; users do not perform internal repairs. Internal optics need a Netalux or certified check every six months.
Is the Netalux Kamino-300 suitable for rentals and new users?
It is sized for mobile multi-site professional work on single-phase power. Only trained operators may run a Class 4 system. Z-Beam includes hands-on training with rental; untrained operators are prohibited by the manual.
What safety features and training are required for the Kamino-300?
Class 4 labeling, e-stop, key switch, arm/disarm, external interlock, and alarm symbols. Operators must wear EN207 glasses at 1064 nm, demarcate the zone under Directive 2006/25/EC, use extraction, and complete machine and safety training before emission.
How far in advance should I prepare for a Kamino rental?
Clear the work zone one day before when you can. Confirm a grounded single-phase outlet, 110–240 V, near the part. Open a walk path for the machine and extractor, and stage the parts you want cleaned.
When should I run the wood finish tests?
When the job includes wood with an unknown coating, run one test on this page before arrival. A water drop or a 91 percent isopropyl swab on a hidden spot tells whether the film is water-based, oil-based, or a soft lacquer. Either test is enough.