
Video
Semiconductor cleanroom tooling leaves the bay so a pulsed head can lift process film from open faces without throwing grit into ISO air. Stainless steel shields, aluminum kits, and titanium parts go back only after extraction and a real cleanliness check, not a bright-metal look. Wet recovery that still uses HF is a different job than injection-mold tooling.
| Final results | The laser pass clears polymer from the plasma and metallic contamination from anodized-aluminum and stainless chamber parts, and the part still has to be packaged before it returns to the cleanroom. |
| Speed and ease | The laser pass clears that polymer and metal contamination without the 8 to 16 hour wet-chemical downtime or the ultrapure-water rinse that cycle consumes. |
| Contaminants | The soil is polymer and metal film baked onto anodized-aluminum and stainless chamber parts by the plasma process. |
| Methods | Wet chemistry misses the heavy baked-on layer, so the heavy clean is a bead blast. |
| Challenges | Bead blasting drives media into the surface and destroys an anodized layer. |
Laser cleaning removes a contaminant film from a chamber part, but the fine particulate and vapor byproduct it throws off has to stay inside whatever particle budget the surrounding cleanroom class allows. ISO 14644-1 caps a Class 1 bay at 10 particles per cubic meter at the 0.1 micron size band, while a Class 5 bay allows up to 100,000 particles at that same size, so a laser head sitting next to a wafer stepper.
A dry oxygen plasma clean requires roughly 20 to 30 minutes every 10 rf-hours on etch tooling, while a full wet chemical opening of the chamber often stretches out to hundreds of rf-hours between cycles. Laser cleaning fits the same short, in place logic as the plasma step rather than the long wet clean interval.
Laser cleaning removes organic residue from a quartz or fused silica fixture without touching the substrate itself, since a mid infrared beam near 2.8 microns gets absorbed strongly by that contaminant film while the underlying glass stays largely transparent at that wavelength. That selectivity is why plants reach for a laser pass instead of the wet chemistry alternative, where clearing grit blast damage on high purity quartz calls for 10 to 20 minutes of ultrasonic.
Laser cleaning removes process films, oxides, and particles from chamber liners, showerheads, wafer handling parts, and quartzware without solvents, media blasting, or abrasion that wear those precision surfaces. The work happens off-line, because the laser plume carries whatever it removes and a live cleanroom cannot accept those particles. Parts come out to a service bay, get cleaned in controlled passes with extraction at the source, and go back only after inspection confirms the surface and particle levels meet the fab's acceptance criteria.[1][2][3][4][5]
Media blasting looks cheaper per job, but on semiconductor cleanroom tooling the cleaning bill is the small part of the cost. Sand, soda, and dustless media cut into anodized, ceramic-coated, and quartz surfaces a little more with every cycle, so precision parts drift out of tolerance and get replaced early. Those methods also leave dust and embedded media behind, which adds wipe-down and inspection time before a part can go back near a wafer. Dry ice blasting avoids media residue but moves slowly baked-on process films. Laser cleaning uses no media and no chemistry, so each cycle carries almost no consumable cost and the base material stays intact when the settings match the contaminant. The equipment costs more up front, and the per-clean cost keeps falling because the tooling survives more cleaning cycles.[1][2][3][4][5][6][7][8][9][10][11][12][13][14][15][16][17][18]
| Method | Cost per 100 sq ft | Hourly Rate | Consumables/hr | Setup Cost | Cleaning rate | Surface damage |
|---|---|---|---|---|---|---|
| Sandblasting / Abrasive Blast | 425 USD | 145 USD/hr[7] | 55 USD/hr[3] | 200 USD[8],[9] | 150 sq ft/hr[2],[3],[4] | High: Abrasive action creates measurable surface profile (1.5–4 mils anchor pattern on steel). Causes pitting, warping, or erosion on softer or delicate materials.[1] |
| Soda Blasting | 329 USD | 155 USD/hr | 90 USD/hr | 175 USD | 200 sq ft/hr | Low to moderate: Softer than sand or grit at Mohs 2.5. Does not create significant surface profile on steel. Can etch soft metals (aluminum, copper) or sensitize wood grain. |
| Dry Ice Blasting | 750 USD | 350 USD/hr[7],[11] | 150 USD/hr[11],[12],[13] | 550 USD | 200 sq ft/hr[10] | Low to minimal: Non-abrasive thermal shock mechanism; dry ice sublimates on impact with no surface profile or residue. Some thermal stress risk on heat-sensitive substrates. |
| Dustless Blasting | 641 USD | 375 USD/hr | 80 USD/hr | 250 USD[8] | 130 sq ft/hr | Moderate: Water suppression reduces abrasion heat and dust, but abrasive media still creates surface profile.[1] |
| Laser Cleaning | 500 USD | 400 USD/hr[16],[18] | 0 USD/hr | 0 USD | 80 sq ft/hr[15],[16] | Minimal to none: Non-contact ablation vaporizes contaminants without abrading or mechanically stressing the substrate. Parameter-controlled at 300W (Netalux Kamino class).[14] |
Semiconductor cleanroom tooling sits at the overlap of two rule sets. ISO 14644-1 sets the room's certified particle class, which the cleaning process has to preserve, and the laser and exposure rules govern the equipment doing the work. ANSI Z136.1 and FDA 21 CFR 1040.10 set how a Class 4 cleaning laser is built and run, OSHA Table Z-1 and Cal/OSHA Table AC-1 cap what operators can breathe while residue comes off, and SEMI F47 sets how the system rides through fab power sags. Each card names the standard and the limit that applies to this work.[7]
ISO 14644-1:2015 classifies cleanroom air from ISO Class 1 to 9 by particle concentration. Any cleaning done in the room has to hold the class it was certified at.[1]
SEMI F47-0706 requires semiconductor manufacturing equipment to ride through short voltage sags without tripping offline. A cleaning laser tied into fab power is held to the same immunity curve.[2]
ANSI Z136.1 (2022) is the base US standard for safe laser use. For Class 4 cleaning lasers it drives the controlled area, beam enclosures and interlocks, wavelength-rated eyewear, and a named laser safety officer.[3]
21 CFR 1040.10 is the federal performance standard for laser products sold in the US. It sets classification, labeling, protective housing, and safety interlock requirements, and industrial cleaning lasers fall in Class IV.[4]
29 CFR 1910.1000 Table Z-1 sets 8-hour TWA exposure limits for airborne contaminants. The limit that applies depends on the residue chemistry, so extraction and filtration get sized to the specific deposit being removed.[5]
8 CCR §5155 Table AC-1 is California's own airborne-contaminant PEL list, and for many substances it sets lower limits than federal Table Z-1. It governs cleaning work at California fabs.[6]
Most failures on cleanroom tooling come from too much energy on the part, or from the film not absorbing the pulse at all. Silicon carbide coatings and aluminum chamber hardware sit close to the energy that strips their process films, so a setting that cleans a flat witness area can still burn a coating at an edge or a hot spot. Films that stay transparent at the laser wavelength do not absorb the pulse, and extra passes only add heat to the part. Heat reaching elastomer seals and ablated debris that escapes capture cause the remaining trouble, and both are managed with fixturing and extraction rather than more energy.[1][2]
| Condition | Consequence |
|---|---|
| Aluminum chamber parts or end effectors cleaned above the alloy damage point[1],[2] | The surface melts or roughens, and the new texture traps particles and gives the next film more grip |
| Process film is transparent at the laser wavelength[1],[2] | The pulse passes through without lifting the film, and added passes only raise the heat load on the part |
| Energy set high enough to mark a silicon carbide coating on a chuck, susceptor, or edge ring[1],[2] | The coating ablates or micro-cracks along with the film, and the part loses the qualified surface |
| Beam or reflected energy reaches FKM O-rings or seals on the tool[1],[2] | The elastomer hardens, cracks, or outgasses, and the tool can lose vacuum integrity or shed particles |
| Ablated film material is not captured at the point of removal[1],[2] | Debris re-settles on the tool and nearby surfaces, so the part leaves cleaning contaminated in a new way |
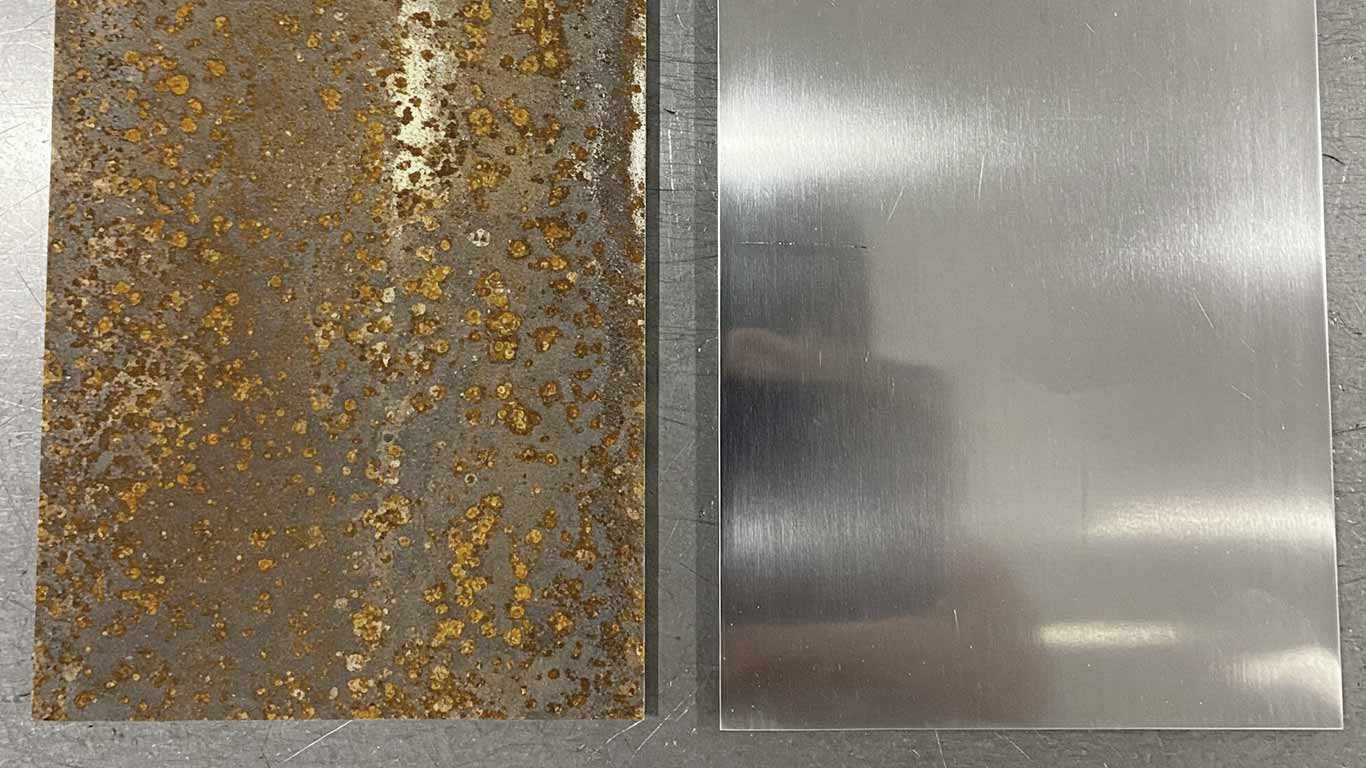
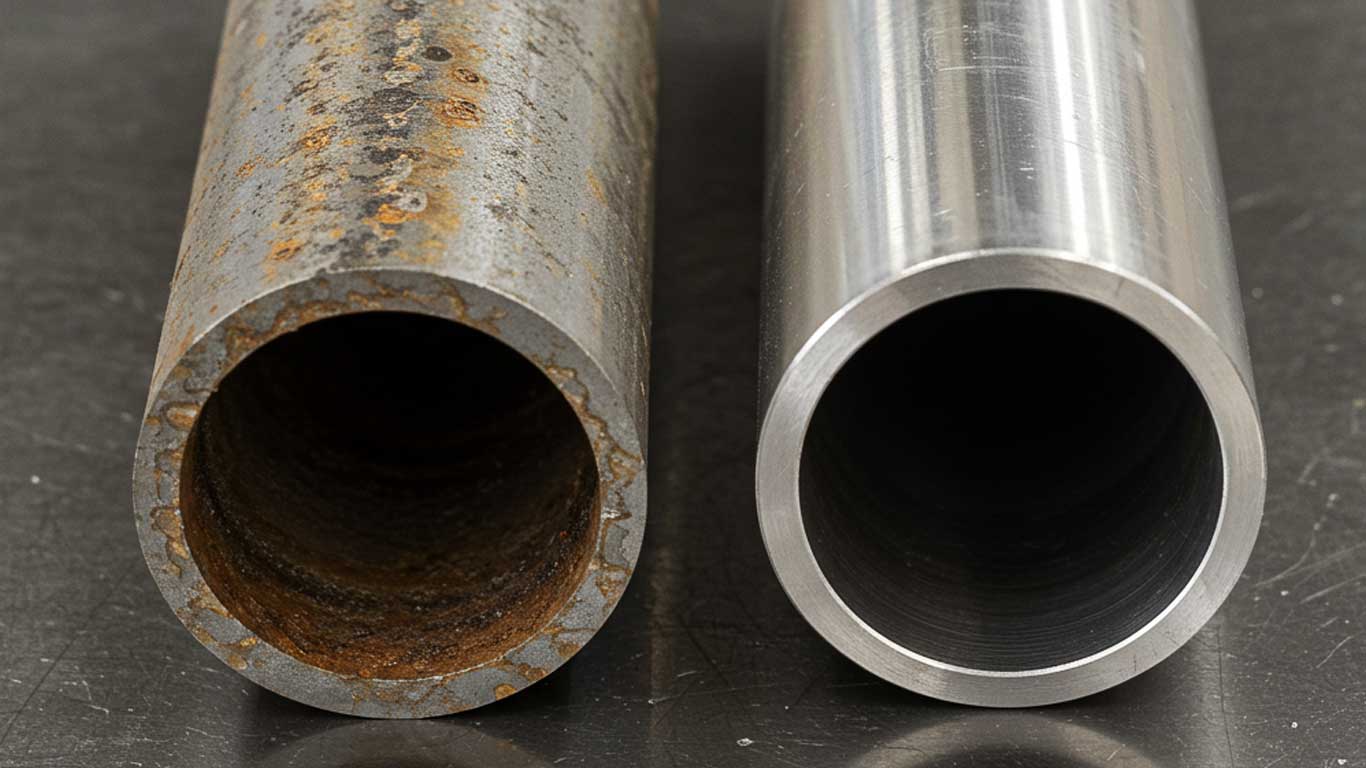
Stainless steel begins to ablate surface films near 0.41 J/cm² at 1064 nm, and that onset is far below where the base metal itself takes damage. The damage threshold runs 5 to 12 J/cm², so the wide margin between those two numbers hides a lot of room for a setting that looks clean but is still wrong for the job. A fabricator cleaning 304L before welding can hit a fluence inside that margin that looks clean to the eye while still stripping chromium from the surface layer, leaving a passive film that forms slower and corrodes sooner than an undamaged one. This page covers the shared ablation and thermal behavior across the austenitic, ferritic, and duplex families, and routes grade-specific parameters to [304 stainless](/materials/stainless-steel-304-laser-cleaning) and [316 stainless](/materials/stainless-steel-316-laser-cleaning), since those two see the most pre-weld and marine-service cleaning. It does not set one fluence for the whole family; molybdenum content, surface finish, and the operation (passivation, weld prep, or scale removal) each shift where that safe range sits. Readers doing weld prep should also check the [weld passivation](/applications/stainless-steel-weld-passivation-laser-cleaning) page for the chromium-depletion risk in more depth.
A nanosecond fiber laser removes aluminum oxide film starting at 0.33 J/cm2 fluence, with the full removal range extending through 1.09 J/cm2. Within that band the mechanism shifts from spallation to sublimation, so the correct setting depends on alloy and film thickness rather than one fixed number. The same physics shows up in [weld prep](/applications/weld-prep-laser-cleaning-applications), on [anodized aluminum](/contaminants/anodized-aluminum-laser-cleaning), and in [suspension-arm cleaning](/videos/porsche-911-upper-suspension-arm-laser-cleaned-bGLki9u3). Aluminum's high thermal conductivity and low melting point near 660 C narrow the margin between stripping the oxide and marking the base metal, and ANSI Z136 beam safety practices apply at every fluence in that range.
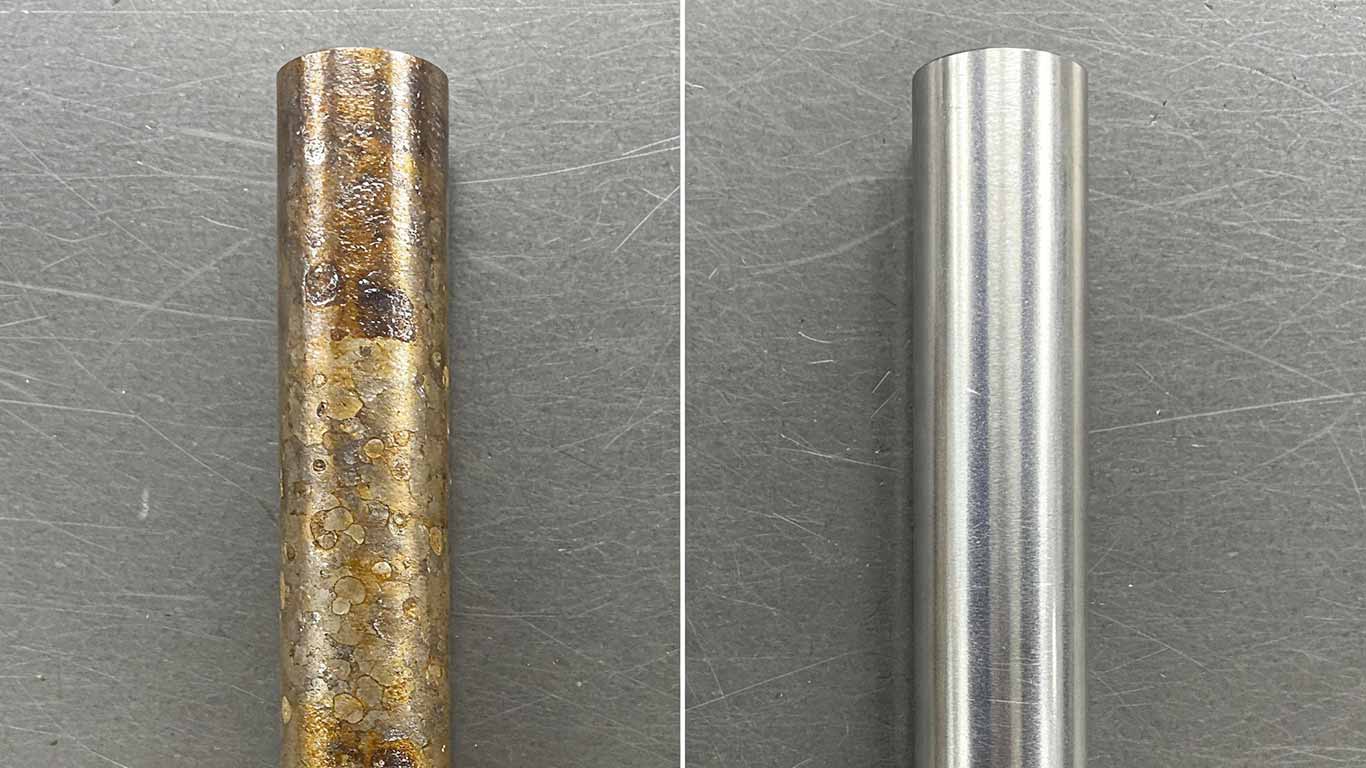
Commercially pure titanium carries a thin native oxide that a pulsed laser can take off without driving oxygen into the bulk. The issue that matters is staying below energy high enough to hurt the metal while still removing the oxide. Heat from short pulses stays at the surface. That is why this job is not the same as a long soak in a furnace. Commercially pure stock is not the same map as an alloy grade. Titanium dust capture belongs on.
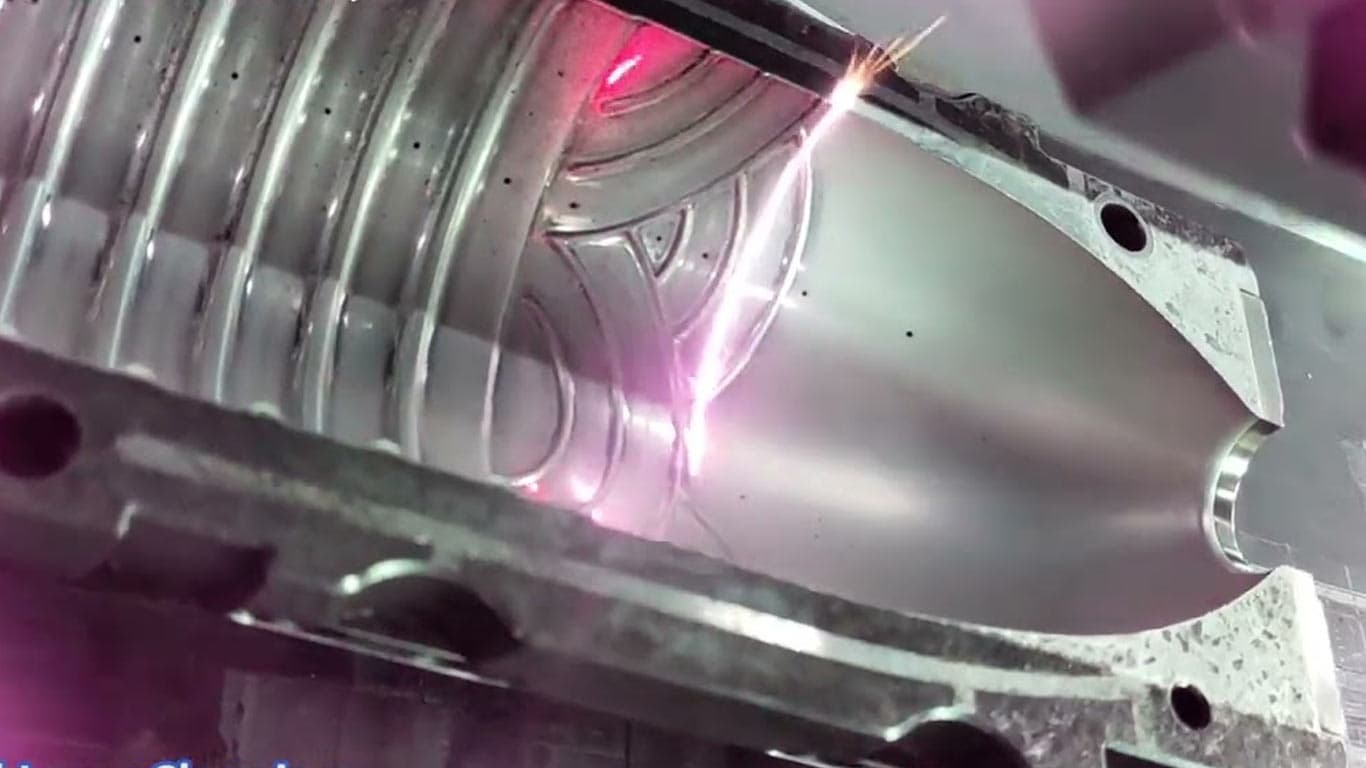
Precision surface work requires contact-free cleaning because gauge faces, optical flats, and polished tooling scratch under abrasive pads or chemical baths. Pulsed fiber sources remove fingerprint films, particulates, and thin oxide from these finishes without touching the substrate, but a continuous-wave fiber laser is not treated as a safe default here until a peer-reviewed study backs that claim. Semiconductor wafer chambers keep their own class-rated rules on [semiconductor cleanroom tooling laser cleaning](/applications/semiconductor-cleanroom-tooling-laser-cleaning), and release-layer mold work belongs on [mold and die laser cleaning](/applications/mold-die-laser-cleaning-applications) rather than here. Titanium implants and [stainless steel](/materials/stainless-steel-laser-cleaning) precision parts each need a shop-tested cleaning limit, since no single particulate count works across every polished substrate.
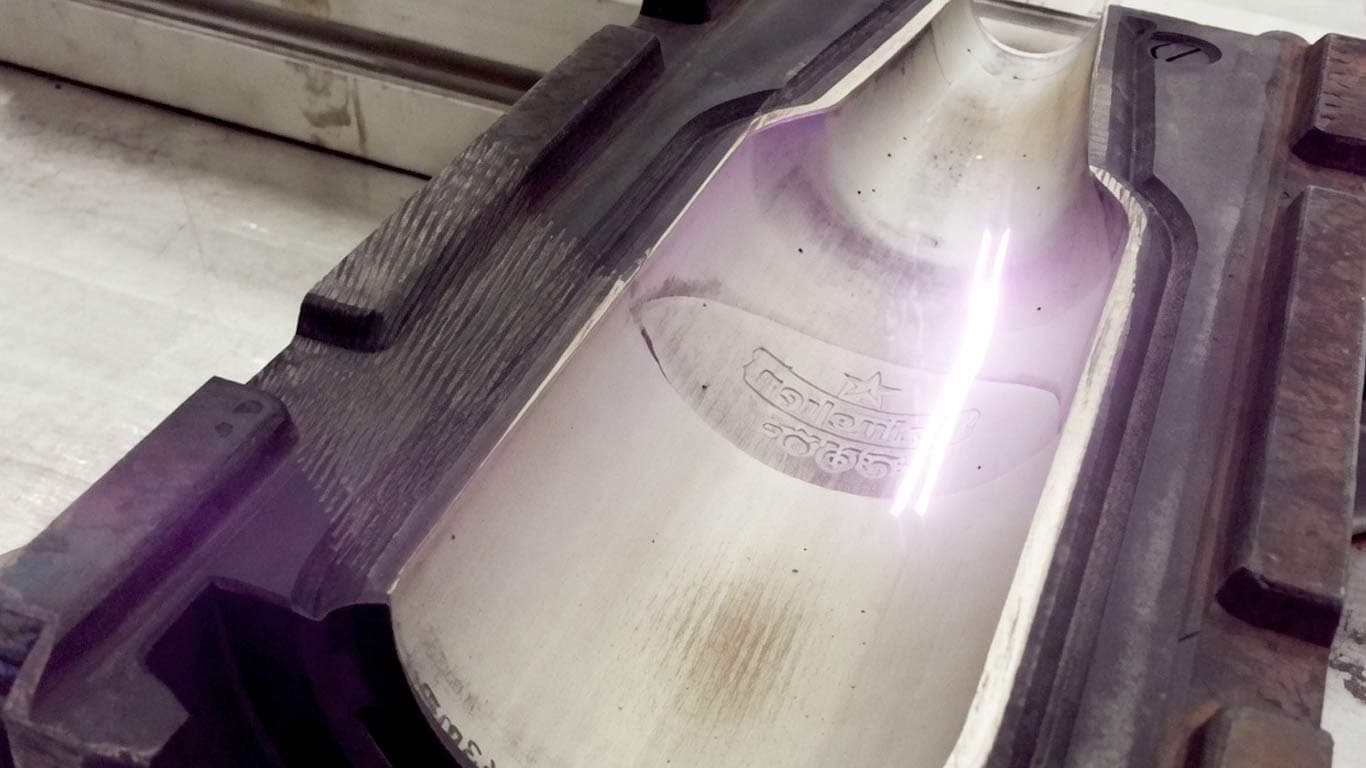
Laser cleaning removes polymer residue, release-agent film, and light oxidation from injection mold cavities and cores without abrasive blasting or solvent soak that can round vent edges or scar a polished finish. The method suits [tool steel](/materials/tool-steel-laser-cleaning) cavities and cores where mold release and carbon buildup need to come off between runs, and it fits the broader class of [mold and die cleaning](/applications/mold-die-laser-cleaning-applications) work where dimensional tolerances matter more than speed. It does not replace deep hot-runner tip service, which lives on the separate [hot-runner cleaning](/applications/hot-runner-laser-cleaning) page, and it does not treat die-cast aluminum tooling, since that metal responds differently to the same fluence. Downtime gains from switching to laser cleaning depend on mold complexity, residue type, and current cleaning method, so any comparison against manual teardown needs mold-specific timing rather than a blanket figure.
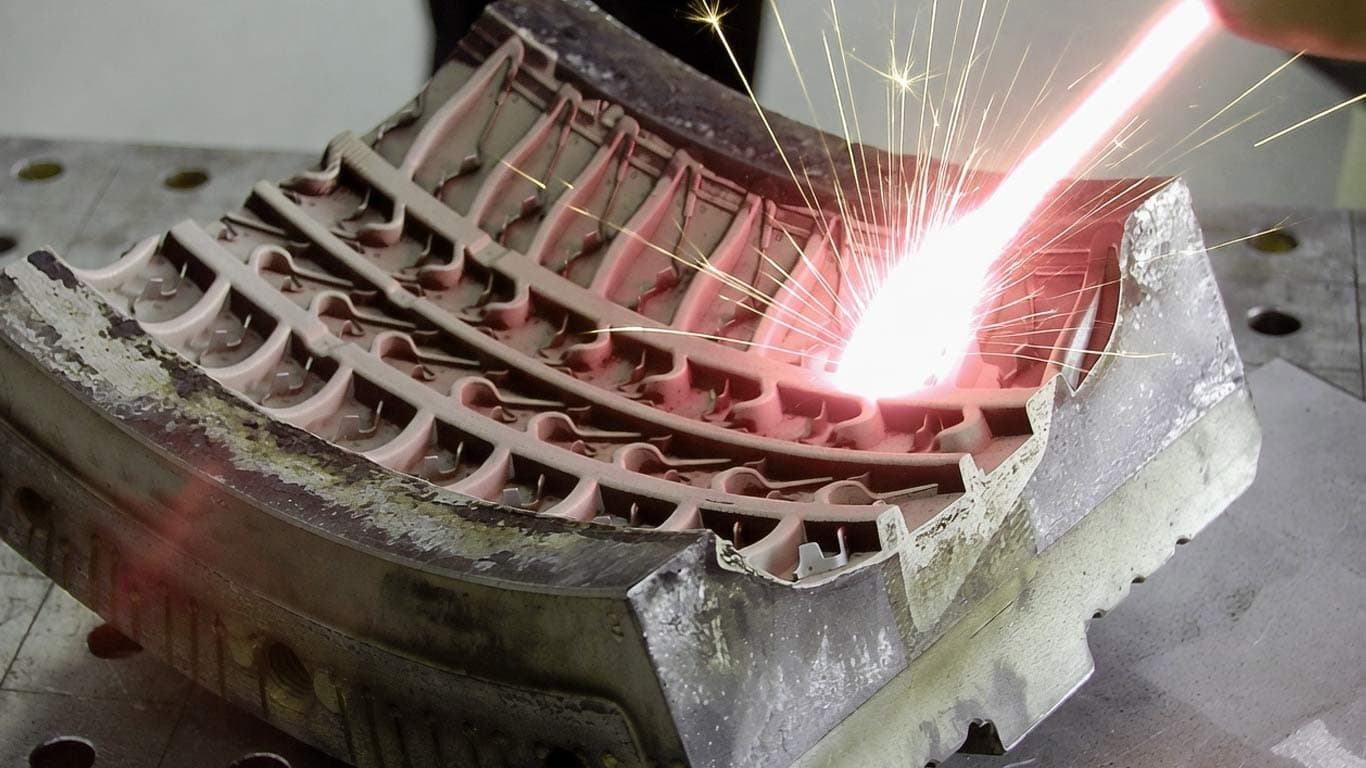
High-pressure die-casting tooling fails for a different reason than an [injection mold](/applications/injection-mold-tooling-laser-cleaning): molten [aluminum](/materials/aluminum-laser-cleaning) reacts with iron in [H13 cavity steel](/materials/tool-steel-laser-cleaning) to form a hard Fe-Al intermetallic layer that raises cavity roughness and locks a shot in place long before surface dirt alone would cause a reject. OSHA Table Z-1 caps total nuisance dust at 15 milligrams per cubic meter in an enclosed die-casting cell, and laser cleaning strips that intermetallic film and the carbonized release residue around it without the abrasive media that would raise roughness further. The process also leaves PVD and nitride anti-soldering coatings intact, where abrasive blasting cuts through them in one pass. It does not recoat a worn insert or re-cut a soldered cavity back to print dimensions.