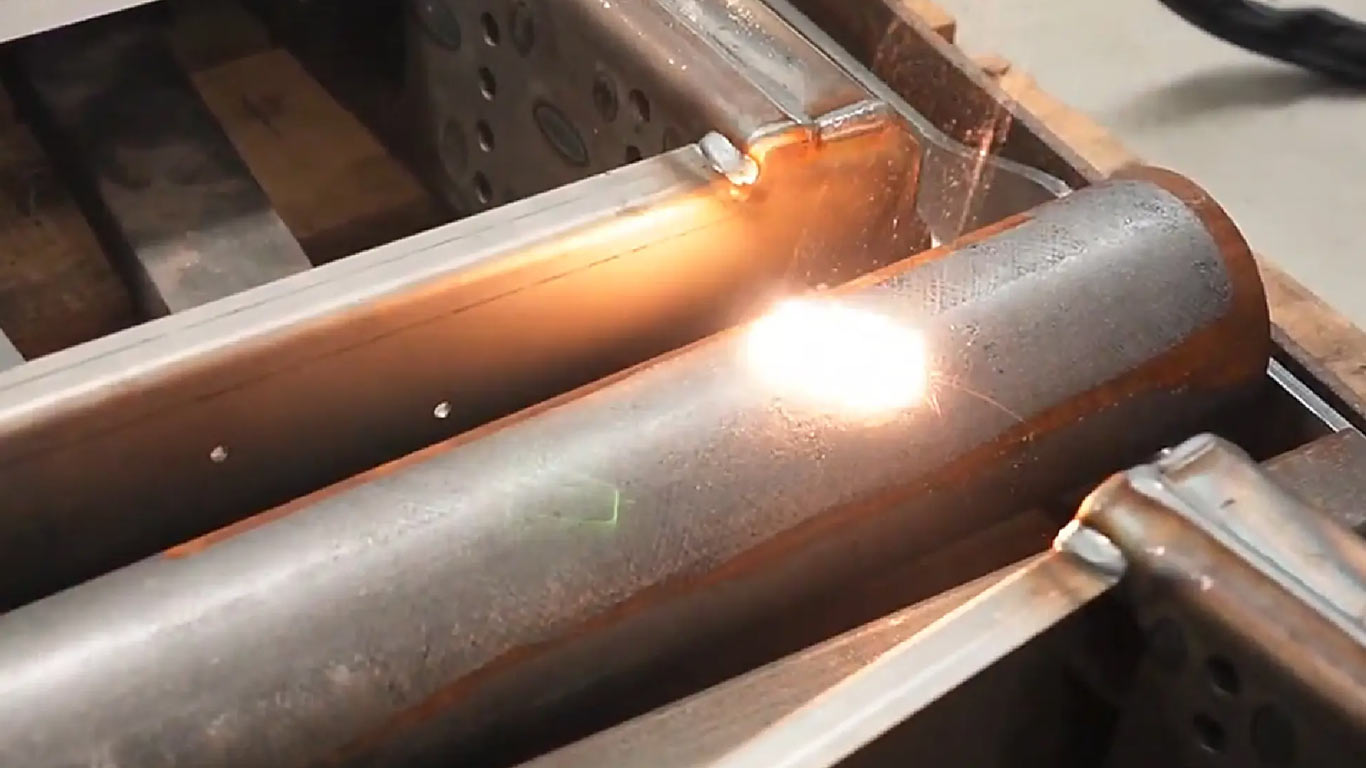
Pulsed fiber laser on a steel conveyor roller in a Bay Area plant
Ikmanda Roswati
Ikmanda RoswatiPh.D.Indonesia
Ultrafast photonics and laser-matter interaction
Published
Jun 26, 2026

Conveyor Belt Roller Laser Cleaning

Industrial conveyor roller maintenance picks laser when grease film and rust must leave bare steel shells without solvent waste or a blast enclosure on the line. A dry pulsed pass on steel and stainless idlers returns the roller the same shift after lockout, and it pairs with food-industry cleaning when the same cell cannot fund media cleanup. Prove a scrap piece of the same shell gauge before production rollers see a pass, and keep rubber lagging out of the beam.

What the pass leaves on Conveyor Belt Roller

What the pass leaves on Conveyor Belt Roller
Final resultsThe laser pass strips the pulley shell to bare metal, free of grease, rust, old lagging, and old adhesive, and the shell is ready for primer and new lagging.
Speed and easeThe laser pass clears that grease, rust, old lagging, and adhesive without the angle-grinder strip time, though that strip-only duration is not known.

What makes Conveyor Belt Roller hard to clean

What makes Conveyor Belt Roller hard to clean
ContaminantsThe contaminant is grease, rust, old cured-rubber lagging, and old adhesive on the pulley shell.
MethodsAn angle grinder with a tungsten-carbide buffing disc is the standard tool, but any oxide, rust, or grinding dust left behind stops the new adhesive from bonding, so the regrind has to reach bare metal everywhere the lagging will sit.
ChallengesGrinding is a known cause of rubber structure damage that the installation procedure is built to work around.

Conveyor Roller FAQ

  • How do you clean a conveyor belt roller with laser instead of solvents?

    Industrial conveyor rollers take a dry pulsed pass on bare steel after lockout, and lagging stays out of the beam. Grease film and rust are separate jobs so one setting does not burn the coating while chasing oxide.

  • Can conveyor chain cleaning use the same laser settings as rollers?

    Conveyor chain cleaning is a different geometry from roller shells. Prove a scrap link of the same alloy before production chain sees a pass, and keep lockout on the drive for the whole job under OSHA 1910.147.

  • How do ESS conveyor belt cleaners compare with laser on rollers?

    ESS-style belt cleaners scrape the belt face; laser targets bare steel roller shells after lockout. Use this page for roller soil decisions, not as a belt-cleaner product directory.

  • How do you clean conveyor rollers when grease and rust both sit on the face?

    Budget a grease-film pass and a rust pass as different jobs. Published conveyor-roll cleaning dropped from about 8 hours traditional to about 1 hour dry-ice on a competing case study (coldjet-roll-cycle); laser quotes compete on that same-shift return without media waste.

  • What types of conveyor belt cleaner compete with laser on rollers?

    Solvent wipe, abrasive blast, and dry-ice all show up on roller quotes. Laser wins when the cell must skip solvent waste and a blast enclosure after ANSI Z136 Class 4 controls are on the walkdown.

  • Where can I get a conveyor belt cleaning system?

    This page does not own local system-directory intent. See rental pages for hire geography; use this page to decide laser versus solvent or abrasive on bare steel rollers after lockout.

Plating Still Strips First

A roller that looks cleaner still fails when rust energy strips zinc or chrome plating faster than the contaminant leaves the face.

Condition
Energy set to remove rust or mill scale on bare steel is applied to a zinc or chrome plated roller shell.
A mixed face with rubber lagging and exposed hubs runs under one setting aimed at rust on the hub.

Sandblast Rate Versus Laser

Laser cleaning is quoted against published sandblasting shop rates so industrial conveyor roller work can weigh abrasive waste against a dry pulsed pass after lockout.[1][2][3][4][5][6][7][8][9][10][11][12][13][14][15][16][17][18]

MethodCost per 100 sq ftHourly RateConsumables/hrSetup CostCleaning rateSurface damage
Sandblasting / Abrasive Blast425 USD145 USD/hr[7]55 USD/hr[3]200 USD[8],[9]150 sq ft/hr[2],[3],[4]High: Abrasive action creates measurable surface profile (1.5–4 mils anchor pattern on steel). Causes pitting, warping, or erosion on softer or delicate materials.[1]
Soda Blasting329 USD155 USD/hr90 USD/hr175 USD200 sq ft/hrLow to moderate: Softer than sand or grit at Mohs 2.5. Does not create significant surface profile on steel. Can etch soft metals (aluminum, copper) or sensitize wood grain.
Dry Ice Blasting750 USD350 USD/hr[7],[11]150 USD/hr[11],[12],[13]550 USD200 sq ft/hr[10]Low to minimal: Non-abrasive thermal shock mechanism; dry ice sublimates on impact with no surface profile or residue. Some thermal stress risk on heat-sensitive substrates.
Dustless Blasting641 USD375 USD/hr80 USD/hr250 USD[8]130 sq ft/hrModerate: Water suppression reduces abrasion heat and dust, but abrasive media still creates surface profile.[1]
Laser Cleaning500 USD400 USD/hr[16],[18]0 USD/hr0 USD80 sq ft/hr[15],[16]Minimal to none: Non-contact ablation vaporizes contaminants without abrading or mechanically stressing the substrate. Parameter-controlled at 300W (Netalux Kamino class).[14]
Sources(18 references)
  1. SSPC-SP10 / ISO 8501-1 Sa 2.5 — Near-White Blast Cleaning surface-preparation standard sspc.org (opens in new tab)
  2. How to Bid on an Abrasive Blasting Project and Profit — Graco Contractor Guide graco.com (opens in new tab)
  3. Abrasive Blast Consumption, Production and Cleaning Rates — Technical Bulletin kleenblast.com (opens in new tab)
  4. AP42 Section 13.2.6: Abrasive Blasting — EPA Emissions Factor Documentation gaftp.epa.gov (opens in new tab)
  5. BAAQMD Regulation 12, Rule 4 — Sandblasting baaqmd.gov (opens in new tab)
  6. 8 CCR §1532.1 — Lead in Construction dir.ca.gov (opens in new tab)
  7. Dry Ice Blasting vs Sand Blasting vs Soda Blasting — 2026 Comparison dryicen.com (opens in new tab)
  8. How to Properly Contain a Site for Abrasive Blasting — Graco Contractor Guide graco.com (opens in new tab)
  9. Sandblasting Containment Methods: A Compliance Guide southernsandblastingandpainting.com (opens in new tab)
  10. Mold, Smoke & Fire Remediation with Dry Ice Blasting — Cold Jet Production Rates coldjet.com (opens in new tab)
  11. How Much Does Dry Ice Blasting Cost? 5 Key Factors to Consider aiolith.com (opens in new tab)
  12. The Definitive Guide to Dry Ice Blasting — Cold Jet info.coldjet.com (opens in new tab)
  13. Dry Ice Blasting Business | Revenue, Margins & Startup Cost bizbite.io (opens in new tab)
  14. ANSI Z136.1 — Safe Use of Lasers webstore.ansi.org (opens in new tab)
  15. Top 5 Industrial Laser Cleaning Machines for Rust Removal in 2026 arcuscnc.com (opens in new tab)
  16. Cost of Laser Rust Removal in 2026: $80-$300/hr Service | $0.50/hr to Operate fiberlaserclean.com (opens in new tab)
  17. BAAQMD Regulation 6 — Particulate Matter, Common Definitions and Test Methods baaqmd.gov (opens in new tab)
  18. Laser Cleaning Service Cost Per Square Foot 2026: The Ultimate Guide cklasersz.com (opens in new tab)

Lockout And Laser Duties

Conveyor roller laser work sits under OSHA lockout before guards open and ANSI Z136.1 Class 4 duties for the fiber laser on the roller face. Verify each rule on the walkdown before the first pulse on a bare steel shell.[1][2]

  • OSHA logo

    OSHA

    View official documentation (opens in new tab)

    29 CFR 1910.147 requires the conveyor drive motor and roller pinch points locked and tagged before guarding opens for a laser cleaning pass. Verify Occupational Safety and Health Administration lockout before the nip opens.[1]
  • ANSI logo

    ANSI

    View official documentation (opens in new tab)

    ANSI Z136.1 sets hazard classification, engineering controls, and laser safety officer duties for the industrial fiber laser on roller faces. Confirm American National Standards Institute controls before that unit fires.[2]

Sources(2 references)
  1. osha-147-conveyor osha.gov (opens in new tab) — OSHA 1910.147 lockout before conveyor service
  2. ansi-z136-conveyor webstore.ansi.org (opens in new tab) — ANSI Z136.1 Class 4 laser duties

Bare Steel Versus Lagging

Conveyor belt roller laser cleaning separates bare steel faces from rubber or urethane lagging before any production pass starts on the line.

1Stop when lagging covers the roller face
  • Do not run a laser pass on rubber or urethane lagging; that coating fails at a fraction of the energy used on exposed steel.
  • Separate bare-metal sections from lagged sections during inspection before setup.
2Lock out the drive before guards open
  • Lock and tag the conveyor drive motor and roller pinch points before guarding opens for a cleaning pass.
  • A re-energized roller can catch a hand or cable in the nip.
3Prove grease film and rust as separate jobs
  • Budget a grease-film pass and a rust pass as different jobs on the same roller when both soils sit on the face.
  • Prove a scrap piece of the same shell gauge before the production roller returns to the belt.