
Video
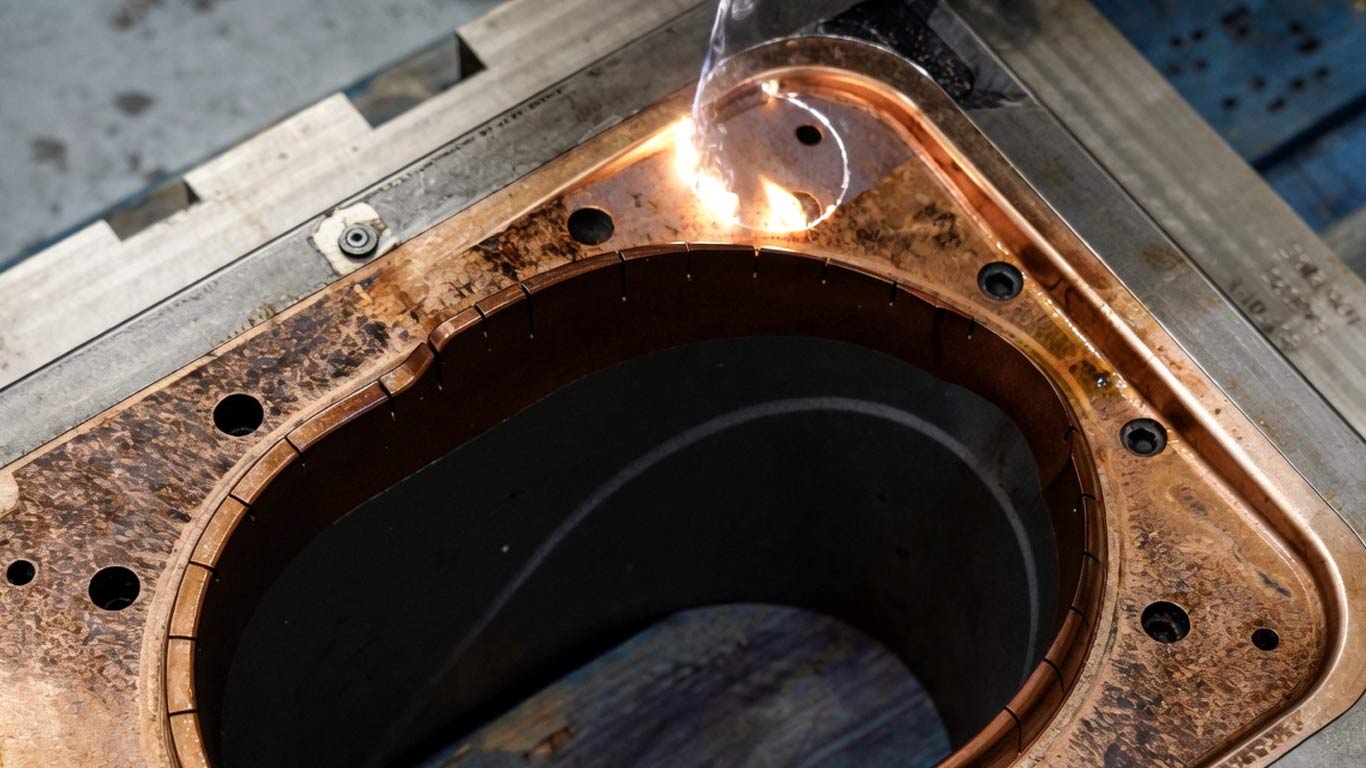
A compression mold cure film is sulfur bound to the cavity surface during vulcanization, a different residue than the release wax on top of it, and clearing it from tool steel cavities needs a narrower fluence band than an injection mold cavity does. Laser cleaning removes the cured rubber film and the wax layer together while holding cavity texture at ARPM Class A1 tolerance near 0.10 millimeter, where an abrasive blast would round the vent lands that let trapped air escape mid-cure. An inert gas assist keeps sulfur vapor from recombining on the warm steel behind the beam path. This does not reset a mold that has already lost its vent geometry to wear, and it does not replace a scheduled repolish once the cavity surface itself has pitted.
| Final results | The laser pass clears cured flash, release, and bloom from the chrome-plated cavity, and the chrome itself still has to stay intact. |
| Speed and ease | The laser pass runs that same 50 to 100 cycle maintenance cadence without the solvent it requires, and the clean's own duration is not known. |
| Contaminants | The contaminant is cured flash left on the face, release agent, and bloom migrating out of the compound. |
| Methods | An air blast alone does not fully clear the flash, so solvent is typically still needed to finish the job. |
| Challenges | A solvent that is wrong for chrome eats the plating. |
OSHA's hazard communication standard requires safety data sheets and labeling for the mold-release chemicals and cured-rubber residue this process burns off compression tooling. Cal/OSHA's airborne-contaminant table caps the smoke and particulate exposure from that ablation, and ANSI Z136.1 sets the beam-control rules for the laser itself.[1][2][3][4]
Title 8 Section 5155's Table AC-1 sets the airborne exposure limits for the mold-release and cured-rubber particulate this cleaning process generates.[1]
29 CFR 1910.1200 requires labeled safety data sheets for the release-agent chemicals and rubber residue handled during cleaning.[2]
Z136.1 sets the beam-control and eyewear requirements for running the laser near mold-plant personnel.[3]
Release agents and sulfur-rich byproducts from the rubber itself bake onto the cavity wall cycle after cycle, building a gray film a plain wipe almost never fully lifts. That controlled-area cleaning work follows ANSI Z136.1 regardless of which laser station runs it. Release chemistry is not one material; it splits into several distinct families, and each leaves a slightly different residue behind, which is the real reason a single solvent pass rarely clears the whole.
Automated systems clean compression mold cavities while the tool is still hot off the press, covering resin, release agent, and oxide at rates up to 22 square meters per hour without cutting into the steel. A chrome-plated die cavity study found cured rubber residue lifts cleanly up to about 0.97 J/cm²[7], the point where the plating itself starts to blister (Jia et al. 2019, ScienceDirect) and the same ceiling plated-insert jobs watch for on compression.
Research on laser-textured rubber surfaces found the beam reshapes surface topography without degrading the bulk polymer underneath, so a properly tuned pass resets the cavity texture rather than layering a new one on top that would change release behavior.
A compression mold tool can run well into six figures and clear more than a million parts before replacement, so solvent-dip or abrasive damage is the failure mode a cleaning method really has to avoid. A life-cycle assessment on laser cleaning in remanufacturing found it lowers total environmental impact by about 40% versus solvent-ultrasonic cleaning and about 83% versus sandblasting (Wang et al. 2025), impact that would otherwise land as disposal and handling cost on.
Vulcanization locks rubber polymer chains together with sulfur crosslinks under heat and pressure, turning soft uncured stock into the elastic part that comes out at cycle's end (Wikipedia vulcanization overview). That same sulfur chemistry drifts onto the cavity wall run after run, baking into a thin crust the steel surface does not shed on its own. Deep draft pockets and sharp corners build that crust fastest, since cure gas and release agent both pool there.
Every compression mold cleaning cell runs under the same ANSI Z136.1 safe-use-of-lasers practice as any other industrial beam work, covering enclosure, interlocks, and wavelength-rated eyewear no matter which rubber compound the mold produces.
What happens to the cavity finish and vent geometry governs the real cost of a rubber compression mold cleaning job, not just the hourly rate on an invoice. Vent channels in a compression mold stay open at a narrow width so trapped air and cure gas escape during the molding cycle, and a method that rounds or clogs that opening pushes the cost into scrap parts and a re-machining trip, not the cleaning bill. Wire brushing and manual scraping keep a low sticker price but leave sulfur bloom and cured flash in tight vent corners, so a technician repeats the pass more often than the quote assumed. Chemical solvent stripping adds tank dwell time, a waste manifest, and PPE, and that handling obligation runs alongside the solvent cost. Abrasive blasting clears buildup fast but wears vent edges with each pass, trading a lower per-job rate for a shorter mold service life. Laser cleaning needs no media or solvent, and a life-cycle study on laser cleaning in remanufacturing found roughly 40 percent lower environmental impact than solvent-ultrasonic cleaning and about 83 percent lower impact than sandblasting, impact that otherwise becomes disposal and handling cost.[1][2][3][4]
| Method | Cost per 100 sq ft | Hourly Rate | Consumables/hr | Setup Cost | Cleaning rate | Surface damage |
|---|---|---|---|---|---|---|
| Sandblasting / Abrasive Blast | 425 USD | 145 USD/hr | 55 USD/hr | 200 USD | 150 sq ft/hr | High: Abrasive action creates measurable surface profile (1.5–4 mils anchor pattern on steel). Causes pitting, warping, or erosion on softer or delicate materials.[3] |
| Soda Blasting | 329 USD | 155 USD/hr | 90 USD/hr | 175 USD | 200 sq ft/hr | Low to moderate: Softer than sand or grit at Mohs 2.5. Does not create significant surface profile on steel. Can etch soft metals (aluminum, copper) or sensitize wood grain. |
| Dry Ice Blasting | 750 USD | 350 USD/hr | 150 USD/hr | 550 USD | 200 sq ft/hr | Low to minimal: Non-abrasive thermal shock mechanism; dry ice sublimates on impact with no surface profile or residue. Some thermal stress risk on heat-sensitive substrates. |
| Dustless Blasting | 641 USD | 375 USD/hr | 80 USD/hr | 250 USD | 130 sq ft/hr | Moderate: Water suppression reduces abrasion heat and dust, but abrasive media still creates surface profile.[3] |
| Laser Cleaning | 500 USD | 400 USD/hr | 0 USD/hr | 0 USD | 80 sq ft/hr | Minimal to none: Non-contact ablation vaporizes contaminants without abrading or mechanically stressing the substrate. Parameter-controlled at 300W (Netalux Kamino class).[4] |
This rubber compression mold fails when laser cleaning pushes fluence past the chrome plating's tolerance or leaves release-agent film behind between cure cycles. Chrome-plated cavity slots blister above roughly 0.97 J/cm2[1] of pulsed energy on cured rubber residue, and film from any of the five common release-agent families changes how the beam couples to the surface on the next run. Vent channels, textured logo zones, and thin cavity walls each carry a separate risk that one fixed cleaning recipe cannot cover.[2]
| Condition |
|---|
| Vent channels stay packed with carbonized rubber because the beam angle cannot reach the full channel depth[1],[2] |
| Fluence on chrome-plated cavity slots climbs past roughly 0.97 J/cm2 while cured rubber residue is still on the surface[1],[2] |
| A release-agent film from any of the five common commercial families sits on the cavity wall before cleaning starts[1],[2] |
| Repeated full-power passes cross the same textured logo or knurl pattern on the cavity face[1],[2] |
| A thin cavity wall section heats up during cleaning without any surface temperature check[1],[2] |
A rubber compression mold requires careful cleaning between cycles because cured flash and release-agent residue collect in vent grooves and cavity detail. Left alone, that buildup changes cavity dimensions enough to distort the next part and clog vents that let trapped air and gas escape. A laser removes the bonded rubber and carbon layer from the tool steel without abrasive contact, so textured cavity surfaces and narrow vent channels keep their original geometry. Plants that replace bead blasting or solvent soak with laser cleaning report fewer scrapped parts and shorter changeover time between mold runs.[1][2]


