
OSHA
View official documentation (opens in new tab)OSHA Table Z-1 frames air-contaminant limits that cover polymer particulate when polypropylene laser cleaning runs without complete capture.[1]
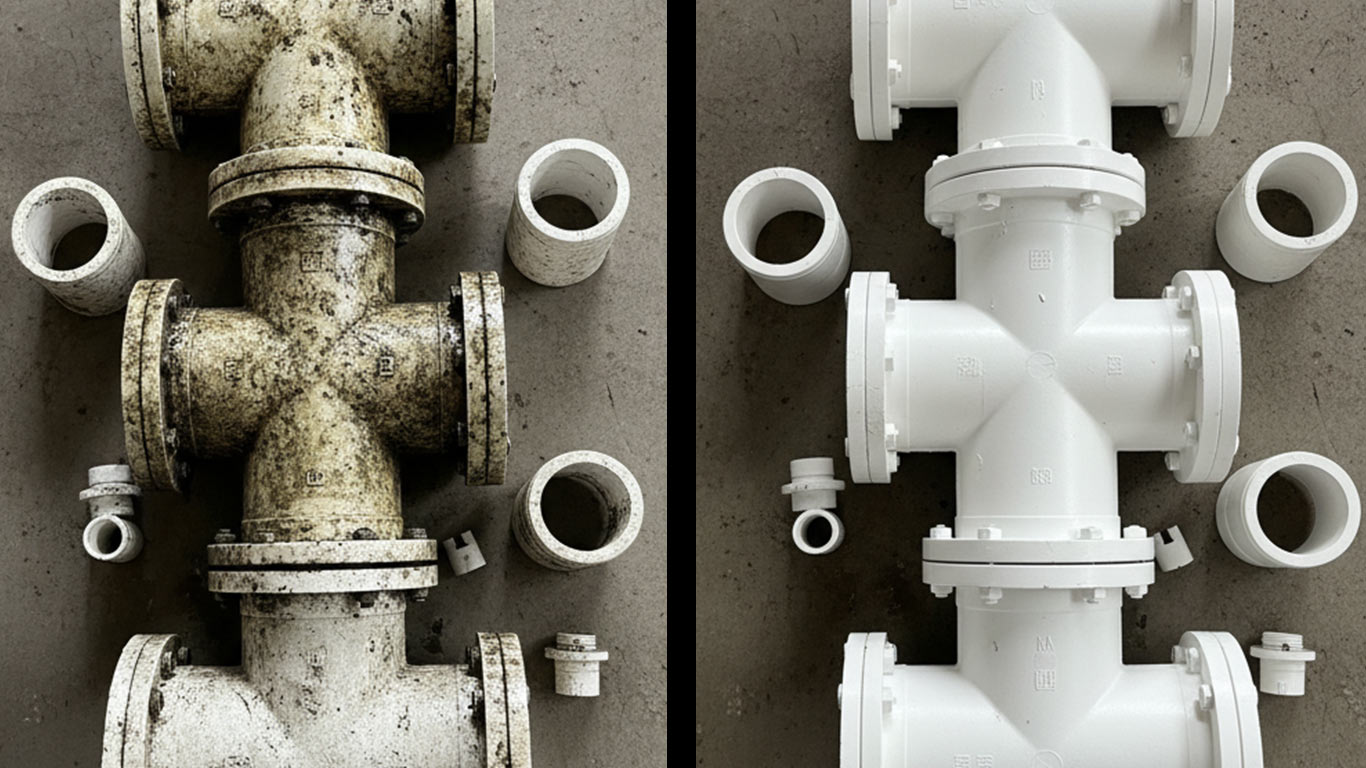
Polypropylene grade and fill selection governs how the surface responds before anyone sets particulate capture at the head. A homopolymer tote, a talc-filled bumper, and a mold-release residue skin each call for a different pass, and warp starts long before an edge scorches or a pigment shifts shade. This overview treats grade and pigment load as the deciding factor for a does-and-won't split, then stops short of resin-additive chemistry that belongs with a compounder, not an operator. It does not carry over the rigid-panel limits that guide acrylic-pmma-laser-cleaning work or the low-heat caution that governs polyvinyl-chloride-laser-cleaning profile, and it separates mold-release residue from the organic-grease-oil-laser-cleaning baseline. Confirm the grade and pigment tag first, then route particulate capture at the head before the pass runs, since warp shows up sooner than any color shift.
| Final results | Paint, grease and oil, manufacturing residue, and fire char are off the part, and the part stays the same shape. |
| Speed and ease | The duration is not known, but the laser clears the mold release without the legacy wash-scuff-wipe routine. |
| Contaminants | Paint, grease and oil, mold release, and soot. |
| Methods | If mold release is not fully removed, the primer or sealer applied afterward will fish-eye badly — a plain wipe can leave enough behind to fail. |
| Challenges | Left-behind mold-release contamination causes poor adhesion, fisheyes, peeling, and paint delamination. |
Polypropylene laser cleaning needs a grade call first. Prove a low energy scrap map before the production face. Homopolymer, copolymer, and filled stock melt and char at different rates because heat stays near the beam (Micro-texturing of polymer surfaces using lasers: a review). Keep dust capture on from the first coupon pass.
Dry polypropylene laser cleaning still produces polymer dust and char fragments that need capture. Federal Table Z-1 frames air contaminants. California Title 8 section 5155 covers airborne limits. Bay Area plumes still sit under Regulation 6 visible-emission rules (OSHA Table Z-1) (Cal/OSHA Title 8 §5155) (BAAQMD Regulation 6).
OSHA Table Z-1 frames air-contaminant limits that cover polymer particulate when polypropylene laser cleaning runs without complete capture.[1]

Cal/OSHA Title 8 section 5155 Table AC-1 sets California airborne contaminant limits that apply to polymer dust from dry laser cleaning.[2]
BAAQMD Regulation 6 covers visible particulate emissions when a polypropylene laser-cleaning plume leaves the booth or outdoor cell.[3]
Polypropylene requires a coupon test before full-pass cleaning because manufacturers have not published a laser highest safe energy for the material. Cleaning onset estimates for polypropylene sit near 0.3 to 1.0 J/cm² at 1064 nm in the nanosecond regime, though that range comes from a secondary estimate rather than a direct measurement. The material's melting point near 160°C and its thermal conductivity of only 0.17 W/m·K mean absorbed heat stays local instead of spreading into.
Polypropylene is a light, moderately strong thermoplastic, with a tensile strength near 33 MPa and a density of 907 kg/m³, that behaves nothing like the metals most laser-cleaning parameter tables assume. This thermal conductivity, only 0.17 W/m·K, keeps absorbed energy from spreading past the surface layer, so heat concentrates right where the residue sits. Because the polymer's melting point falls near 160°C, well below the melt point of aluminum or steel, the same fluence that.
Polypropylene keeps its cleaning settings lower than most metal jobs because its low thermal conductivity, 0.17 W/m·K, and melting point near 160°C leave little margin before the surface itself starts to deform under the beam.
OSHA's Title 8 Table Z-1 governs permissible exposure limits for airborne contaminants that can form when polypropylene decomposes under laser heating instead of simply vaporizing at low fluence. Because the material's melting point sits near 160°C, thermal decomposition byproducts can appear before the surface visibly changes. Ventilation and monitoring keep worker exposure inside those limits during cleaning passes on parts made from polypropylene.
The main risks on polypropylene are melt gloss and brown char. Copying a metal energy map onto this thermoplastic also fails because the bulk barely absorbs one thousand sixty-four nanometer light (IR and UV laser cleaning of polymers (PubMed 11900137)). Heat stays near the beam, so overlap and slow scans damage the face before the soil is gone.[1]
Commodity polypropylene takes little of a one thousand sixty-four nanometer beam in the bulk. Dark mold release, oil, and paint often take the energy first. Once the soil thins, leftover heat can melt or char the face because the melt point sits near one hundred sixty degrees Celsius (The role of absorption mechanism on the optimization of processing commercial polymers under high repetition rate femtosecond laser irradiation). Cleaning stays under a melt-limited ceiling near two joules per square centimeter.
Polypropylene facts on this chart cover tensile strength near thirty-three megapascals, density near nine hundred seven kilograms per cubic meter, and thermal conductivity near seventeen hundredths of a watt per meter-kelvin (MatWeb material property data). The stock melts near one hundred sixty degrees Celsius, so short low-energy passes beat metal-style single-scan recipes that assume a fast heat sink. See mold and die maintenance for shop contexts that work the same thermoplastic family.
| Parameter | Value |
|---|---|
| Canonical substrate | Isotactic polypropylene (homopolymer / copolymer) |
| Tensile strength | ~33 MPa |
| Thermal conductivity | ~0.17 W/m·K |
| Typical wavelength | 1064 nm, pulsed |
Polypropylene cleaning on the thermoplastic chart covers a three-tenths joule per square centimeter floor. The melt-limited ceiling sits near two joules per square centimeter. Bulk stock takes little of the one thousand sixty-four nanometer beam, so usable energy stays tied to the soil layer and to surface melt onset (Paint removal from thermoplastic materials (Schulz 2021)).

