OSHA
View official documentation (opens in new tab)Table Z-1 sets particulate and air-contaminant ceilings for general industry, so polycarbonate dust and char from heated passes need measured capture rather than open-booth exhaust alone.[1]
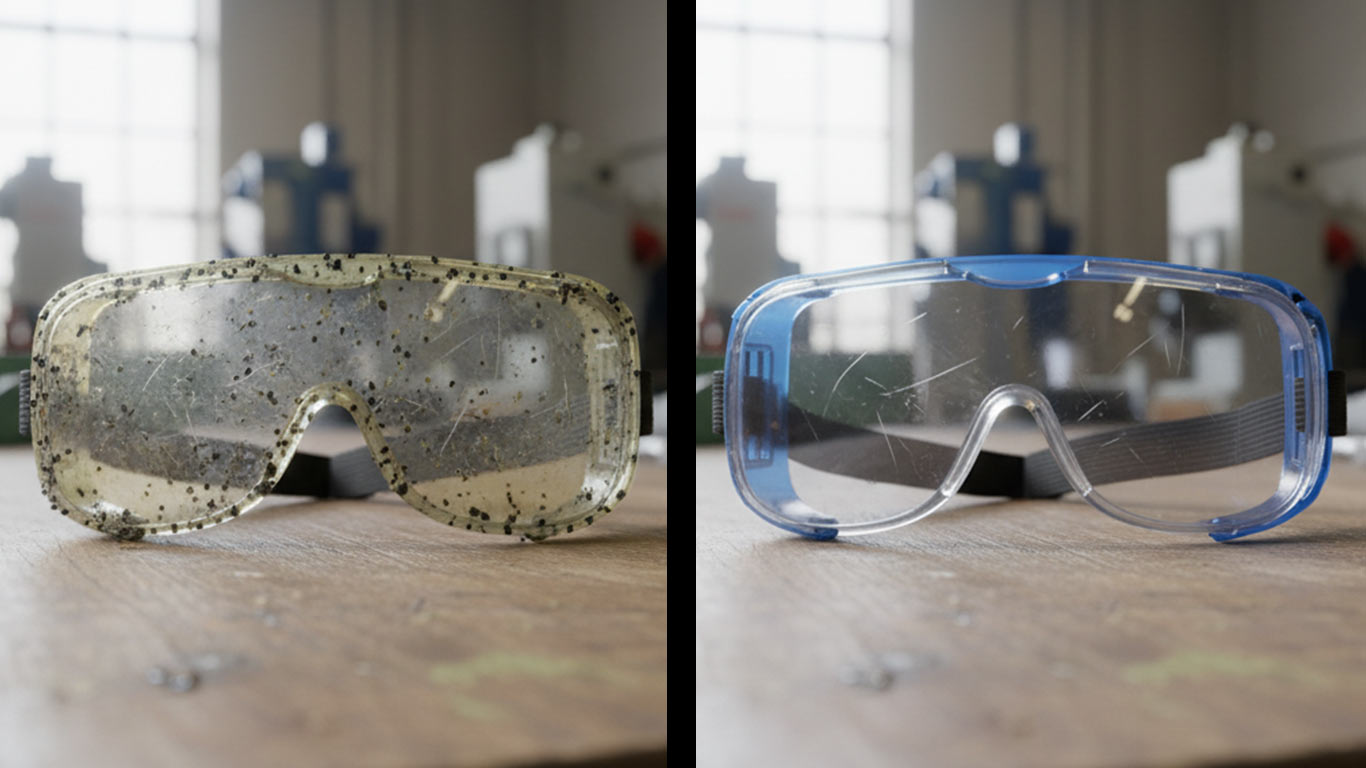
Polycarbonate guards and machine shields haze and yellow under too much laser heat, which is the main risk this page addresses, not the softening that shows up on acrylic sheet. Polycarbonate resists impact and tolerates more heat than acrylic before it deforms, but that same toughness means a haze layer can form on the surface without an obvious melt line, so operators can push power too far before they see damage. Coolant film, machining oil, and UV-degraded surface haze are the usual removal targets, and each needs a pass that clears the contaminant without dwelling long enough to cloud the clear substrate underneath. Because polycarbonate and acrylic look similar but respond to heat differently, settings proven on one plastic do not transfer to the other, and mixing them up is the most common cause of clouded guards after cleaning.
| Final results | Paint, grease and oil, manufacturing residue, and fire char are off the sheet, and the face is not clouded or crazed. |
| Speed and ease | The duration is not known, but the laser clears the residue without the legacy solvent-or-soap wipe. |
| Contaminants | Paint, grease and oil, mold release, and soot. |
| Methods | A solvent wipe left sitting too long instead of removed right away is the flagged risk, so the legacy method needs careful timing more than extra force. |
| Challenges | Solvent left on the surface instead of wiped off right away can haze or craze polycarbonate. |
Polycarbonate facts on this chart cover engineering thermoplastic sheet used for guards, glazing, and optical windows. Charted tensile strength sits near 66 megapascals with thermal conductivity near 0.2 watts per meter-kelvin, so heat stays local under the beam. Near-infrared absorption near ten percent at 1064 nanometers makes this polymer less responsive than acrylic peers in the same thermoplastics group. See precision surface cleaning for optical finish contexts (MatWeb Material Property Data).
| Parameter | Value |
|---|---|
| Canonical substrate | Bisphenol-A polycarbonate (PC) |
| Tensile strength | ~66 MPa |
| Thermal conductivity | ~0.2 W/m·K |
| Typical wavelength | 1064 nm, pulsed |
Polycarbonate cleaning fails when crews treat optical sheet like metal stock or when particulate capture is missing. Overlap that dwells on one spot can push past melt and char. Polymer cleaning work notes volatile release and surface injury once energy climbs, so exhaust and coupon pauses belong in the setup checklist (IR and UV laser cleaning of polymers (PubMed 11900137)).[1]
Yes. Once energy climbs past a careful cleaning band near 0.5 to 2.0 joules per square centimeter, polycarbonate can soften, edge-melt, or leave brown char on optical faces. Coupon in small steps and inspect under raking light before accepting a production map.
Clear polycarbonate absorbs less 1064 nanometer energy than acrylic on many grades, so heat builds more slowly, but melt and char still appear if overlap dwells. Do not copy acrylic maps onto polycarbonate without a fresh coupon on the actual grade and thickness.
Laser heating can release polymer particulate that must stay under OSHA Table Z-1 air-contaminant framing and California Title 8 airborne rules. Source capture at the head is part of setup, not an afterthought.
Paint and adhesive films often need a lighter first pass than bare polymer cleanup. Strip the foreign layer first, then address residue on the clear face instead of forcing one shared energy setting for both stages (Surface modification of bisphenol A polycarbonate by ultraviolet Nd:YVO4 laser (Parvin 2014)).
Clear polycarbonate absorbs roughly ten percent of 1064 nanometer energy, lower than acrylic on the same wavelength, so contamination often darkens and lifts before the bulk polymer sees deep heating. Melt and char still appear if fluence climbs past a careful cleaning band near 0.5 to 2.0 joules per square centimeter. Polymer laser reviews place polycarbonate among the most-studied substrates for controlled surface work when energy stays careful (Micro-texturing of polymer surfaces using lasers (Bratasz 2022)) (MatWeb Material Property Data).
Laser work on polycarbonate can throw polymer dust and char fragments that fall under federal and California air-contaminant tables. Stage local capture at the beam head before coupon work, because a room fan alone does not meet shop particulate limits (29 CFR 1910.1000 Table Z-1, Limits for Air Contaminants) (8 CCR §5155, Airborne Contaminants) (BAAQMD Regulation 6, Particulate Matter, Common Definitions and Test Methods).[3]
Table Z-1 sets particulate and air-contaminant ceilings for general industry, so polycarbonate dust and char from heated passes need measured capture rather than open-booth exhaust alone.[1]
Title 8 §5155 airborne-contaminant rules still apply in California shops, so Bay Area polycarbonate cleaning keeps hood placement at the head even when the soil looks light.[2]
Regulation 6 limits visible emissions from industrial plumes, so outdoor polycarbonate restoration or booth exhaust must stay within Ringelmann No. 1 for no more than three minutes per hour when particulate leaves the capture zone.[3]
Before any energy raise on polycarbonate, name sheet grade, thickness, and any hard-coat or tint because those notes change how fast a near-infrared pass heats a coupon. Particulate capture must sit on the bench under federal air-contaminant limits, and metal-class recipes stay off this polymer path until a scrap face proves a map inside the careful 0.5 to 2.0 joules per square centimeter cleaning band (Compact Disc Laser Cleaning for Polycarbonate Recovering (Barletta 2013)).
Among thermoplastics on the chart, polycarbonate still needs careful fluence even when clear faces absorb less near-infrared energy than acrylic. The practical cleaning band sits near 0.5 to 2.0 joules per square centimeter on engineering grades, with melt and char watched as the hard stop. Coupon work usually proves a working map near the lower half of that band before full-panel overlap scans run (Micro-texturing of polymer surfaces using lasers (Bratasz 2022)).

Industrial aerospace and tooling lines pick laser cleaning when precision metal must skip grit embedment without crossing the Al-Mg oxidation risk band. That same industrial precision cell skips solvent waste next to [mold die work](/applications/mold-die-laser-cleaning-applications), [injection mold tooling](/applications/injection-mold-tooling-laser-cleaning), and [semiconductor tooling](/applications/semiconductor-cleanroom-tooling-laser-cleaning) when the beam can sight the film. Stay inside the researched band instead of treating higher energy as a free upgrade.

Industrial metal recoat and marine coating strip pick laser paint removal when topcoats on [steel](/materials/steel-laser-cleaning) and [aluminum](/materials/aluminum-laser-cleaning) must leave without solvent baths or a blast enclosure. A dry pulsed pass removes the stack into the dust vacuum so panels are recoat-ready the same shift, and it pairs with [lead paint removal](/applications/lead-paint-laser-removal-bay-area) and [chemical-stripping comparisons](/applications/laser-cleaning-vs-chemical-stripping) when methylene chloride is already off the table. Check each layer on a scrap piece so keep primers are not scorched before the production face starts.

Industrial mold lines pick laser cavity cleaning when carbonized resin and release-agent film must leave vents and polished steel without a solvent soak cooldown. A pulsed station keeps changeovers short next to [mold and die work](/applications/mold-die-laser-cleaning-applications), [hot-runner tip cleaning](/applications/hot-runner-laser-cleaning), and [rubber compression molds](/applications/rubber-compression-mold-laser-cleaning) when first shots still show haze after a wipe-only clean. Accept the cavity by Fe/EDS or gloss and haze on those first shots, not by solvent smell on a cloth.

Industrial landmark facade restoration picks laser when black crust and graffiti must clear without sandblast etching or acid-cleaner waste that soft stone cannot take. A dry pulsed pass on [marble](/materials/marble-laser-cleaning), [limestone](/materials/limestone-laser-cleaning), and [brick](/materials/brick-laser-cleaning) leaves the elevation review-ready after a hidden patch under consistent light, and it pairs with [historic masonry restoration](/applications/historic-masonry-restoration-laser-cleaning) on designated buildings that cannot fund a blast enclosure. Prove that patch before full-facade work when crust thickness changes across a single course.


