


Brass Laser Cleaning
The biggest risk in brass laser cleaning is dezincification — when surface temperature hits 907°C, [zinc](/materials/zinc-laser-cleaning) preferentially evaporates and leaves behin...


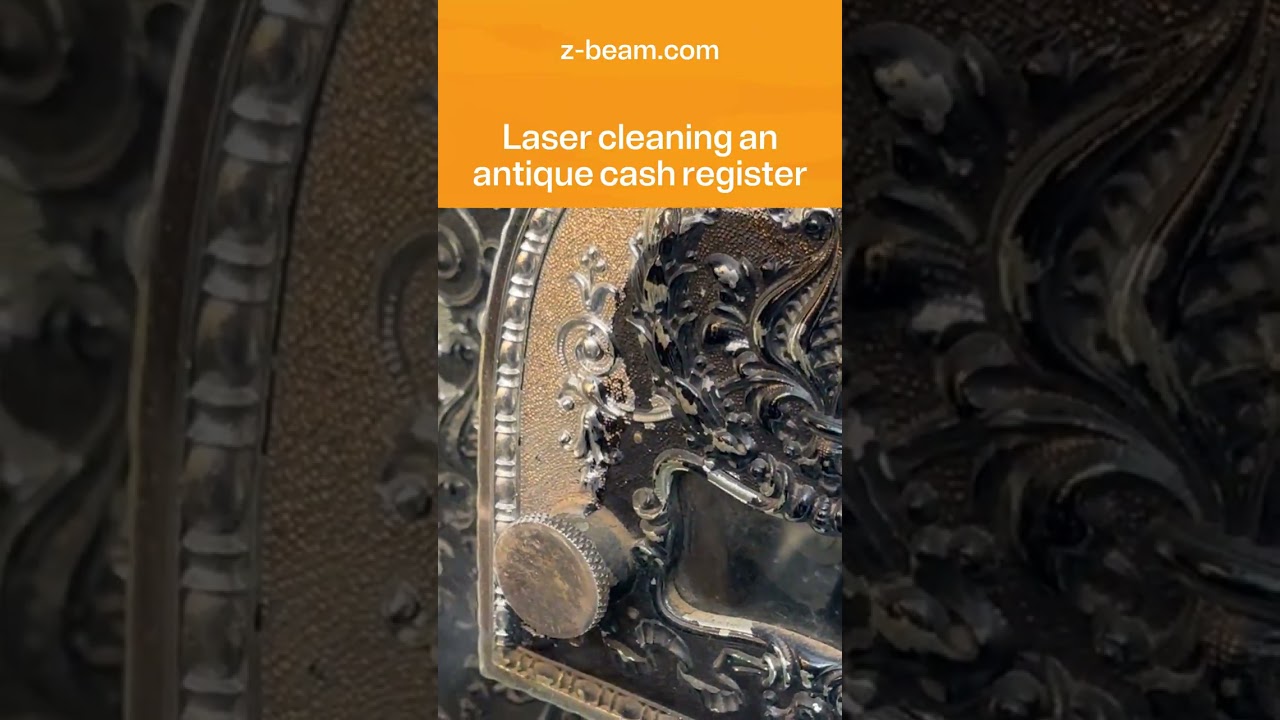
An antique cash register finish is restored when later dirt comes off and the factory color stays. A full strip to bare brass misses that stop. Heritage architectural cleaning treats the original coat as the layer that remains.
Short 9xuN5gDFC4Y shows pulsed laser lifting paint, rust, and grime from an antique cash register finish without abrasive scrubbing of brass detail.
The crew Raman-scans the [copper](/materials/copper-laser-cleaning) first so they know whether they are lifting black soot and reactive chloride crust or stripping the green verdigris brochantite patina the owner wants kept. On heritage bronze they bracket pulse energy on a reference coupon and stop when cuprite still blankets the metal, because a single heavy pass melts through the noble oxide skin. HEPA capture has to beat California copper fume and patina dust limits, and anything cleaned in open air re-tarnishes unless wax or lacquer goes on before the truck leaves.
Bridge crews reach for HEPA before solvent when lead or chromate primers hide under aged topcoats, because BAAQMD cold-cleaner rules cap stripper VOC well below what commercial products carry. A pulsed 1064 nm pass removes organic films without a liquid hazmat stream, yet [oak](/materials/oak-laser-cleaning) and [concrete](/materials/concrete-laser-cleaning) test coupons on the same job do not inherit plate-[steel](/materials/steel-laser-cleaning) damage margins. Grit-profile recoats that demand ISO 8503 anchor tooth stay out of scope even when the visible coat is gone.
The crew inspects the rake face under magnification, then runs the pulsed 1064 nm beam across the cold-welded aluminum buildup until the pressure-welded chip spalls off the [carbide](/materials/tungsten-carbide-laser-cleaning) insert without eroding the cutting edge. Homogeneous [tool-steel](/materials/tool-steel-laser-cleaning) galling on the same die steel gets rejected because there is no absorption window to separate deposit from substrate. HEPA extraction keeps respirable aluminum dust under California's five-milligram respirable limit, and the tool goes back into the cut before built-up edge re-forms on the next pass.
Greasy steel and aluminum weld coupons need extraction bracketed before the pulsed pass. Cutting-fluid residue pyrolyzes at the lowest degrease energy band of any contaminant family on those joint faces, coupon work, not a production shell throughput claim.

Exterior cleaning of San Francisco City Landmarks and Mills Act properties must satisfy the Secretary of the Interior's Standards. The "gentlest means possible" mandate under 36 CF...

Contaminated optics and precision surfaces fail. Coating delamination starts when LIDT drops. LIDT is the power level at which optical coatings fail. It drops measurably at just 6...
