ISO
View official documentation (opens in new tab)ISO 14644-1's cleanroom classification defines nine numbered classes by particle count, the benchmark many precision-surface facilities test their workspace against before parts move through it.[1]
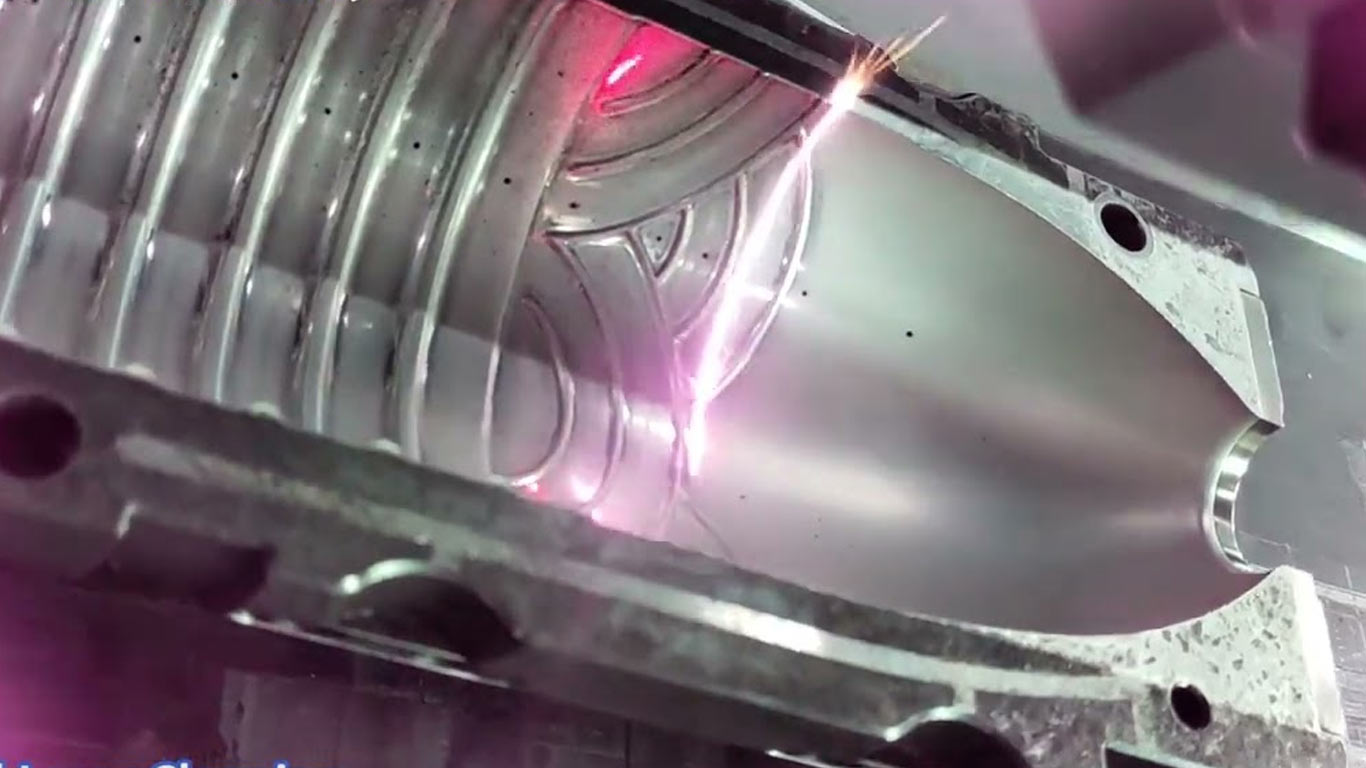
Precision surface work requires contact-free cleaning because gauge faces, optical flats, and polished tooling scratch under abrasive pads or chemical baths. Pulsed fiber sources remove fingerprint films, particulates, and thin oxide from these finishes without touching the substrate, but a continuous-wave fiber laser is not treated as a safe default here until a peer-reviewed study backs that claim. Semiconductor wafer chambers keep their own class-rated rules on semiconductor cleanroom tooling laser cleaning, and release-layer mold work belongs on mold and die laser cleaning rather than here. Titanium implants and stainless steel precision parts each need a shop-tested cleaning limit, since no single particulate count works across every polished substrate.
| Final results | The laser pass clears fingerprint contaminant, oil, and loose dust from a gauge face or optic, and the face stays free of the grit-wipe scratch a solvent clean can leave. |
| Speed and ease | The laser pass clears that contaminant and dust without forcing the several-hour thermal-wait clock NIST requires after a solvent-and-alcohol clean. |
| Contaminants | The soil is oil, fingerprints, and polishing residue on the face that is the measurement. |
| Methods | Solvent takes the oil but also upsets the block's temperature. |
| Challenges | Any grit in the bath or under the wipe cuts a scratch, which is the error the gauge or optic exists to prevent. |
Laser cleaning removes films, oxide, and residue from precision surfaces such as gauge blocks, optical mounts, and calibration masters without water or abrasive media, but the same beam that clears a monolayer of oil can also roughen a lapped face, resettle ablated debris on a reference edge, or push a substrate past its own damage threshold before anyone sees a visible change. That same beam can start pitting a stainless surface at a fluence near 2 J/cm², and holding fluence just above the point where the surface itself starts to come off turns a flat, lapped face into a rippled one instead of clearing it.[1][2]
| Condition | Consequence |
|---|---|
| Repeated passes hold fluence just above the point where the surface itself starts to come off instead of well below it[1],[2] | The surface grows a periodic ripple pattern instead of staying flat, and a face that needs a specific roughness or reflectance spec no longer matches it even after every contaminant is gone |
| Pulse fluence sits near the alloy's own single-pulse damage threshold[1],[2] | Stainless surfaces pit at a fluence near 2 J/cm² and a lapped or ground face fails a flatness or wear check even though it still looks clean to the eye |
| Ablated debris resettles on the cleaned face or an adjacent reference edge before airflow clears it[1],[2] | The part reads clean under a quick look but fails a particle count or contact inspection, and it has to go back through cleaning or a manual wipe |
| Operators back fluence off to protect the substrate and land below the removal threshold for oil or oxide trapped in low features[1],[2] | A halo of clean and unclean surface shows up on inspection, and the residue left behind changes friction, adhesion, or an optical reading downstream |
| A freshly cleaned surface sits exposed to ambient air before the next process step[1],[2] | A thin new oxide layer forms on the bare metal and reflectance, wear rating, or bonding behavior drifts from spec before the part reaches final inspection |
A precision surface requires more protection during laser cleaning than a general metal part does. On a gauge block, an optical flat, or a machined reference tool, heat buildup from a continuous-wave beam can shift the surface enough to fail its own calibration, even when the contamination comes off cleanly. A pulsed fiber laser, run at low average power with a short dwell time per spot, removes oxide film, handling residue, and light particulate without holding enough heat in the part to move its geometry. The steps below walk from inspection through setup, execution, and a verification pass that checks the part against its original tolerance and finish, not only against visible cleanliness.[1][2][3]
Choosing a cleaning method for precision surfaces requires more than comparing sticker prices. Abrasive and chemical methods add ongoing costs that never show up on a machine's price tag: consumable media or solvent, protective masking reapplied part by part, and rework when contact removes more material than intended. A non-contact method changes that equation, trading consumables and disposal for electricity and a beam that never touches the surface it cleans. A life-cycle comparison of laser cleaning against solvent-ultrasonic cleaning and sandblasting on complex precision parts found laser cleaning cut total environmental impact by about 40%[1] against the solvent method and by roughly 83% against sandblasting, mostly by removing waste streams that used to carry their own handling cost. For a shop weighing the next line for precision surfaces, that shift in where the dollars go matters more than the number stamped on either machine.[2][3][4][5]
| Method | Cost per 100 sq ft | Hourly Rate | Consumables/hr | Setup Cost | Cleaning rate | Surface damage |
|---|---|---|---|---|---|---|
| Sandblasting / Abrasive Blast | 425 USD | 145 USD/hr | 55 USD/hr | 200 USD | 150 sq ft/hr | High: Abrasive action creates measurable surface profile (1.5–4 mils anchor pattern on steel). Causes pitting, warping, or erosion on softer or delicate materials. |
| Soda Blasting | 329 USD | 155 USD/hr | 90 USD/hr | 175 USD | 200 sq ft/hr | Low to moderate: Softer than sand or grit at Mohs 2.5. Does not create significant surface profile on steel. Can etch soft metals (aluminum, copper) or sensitize wood grain. |
| Dry Ice Blasting | 750 USD | 350 USD/hr | 150 USD/hr | 550 USD | 200 sq ft/hr | Low to minimal: Non-abrasive thermal shock mechanism; dry ice sublimates on impact with no surface profile or residue. Some thermal stress risk on heat-sensitive substrates. |
| Dustless Blasting | 641 USD | 375 USD/hr | 80 USD/hr | 250 USD | 130 sq ft/hr | Moderate: Water suppression reduces abrasion heat and dust, but abrasive media still creates surface profile. |
| Laser Cleaning | 500 USD | 400 USD/hr | 0 USD/hr | 0 USD | 80 sq ft/hr | Minimal to none: Non-contact ablation vaporizes contaminants without abrading or mechanically stressing the substrate. Parameter-controlled at 300W (Netalux Kamino class). |
Precision-surface work such as optics, semiconductor components, and medical-device parts requires cleanroom discipline and laser-safety rules from more than one agency. ISO 14644-1 sets the particle-count classes that many of those cleanrooms qualify against, ANSI Z136.1 covers how operators run a laser cleaning system around people, FDA rules under 21 CFR 1040.10 govern the equipment itself, and Cal/OSHA's airborne-contaminant limits under 8 CCR Section 5155 keep the dust the process throws into the air within a breathable range.[1][3][4][5]
ISO 14644-1's cleanroom classification defines nine numbered classes by particle count, the benchmark many precision-surface facilities test their workspace against before parts move through it.[1]
21 CFR 1040.10 sets the FDA performance and labeling standard a laser cleaning system has to meet before it can be sold or operated in the United States, including the hazard class printed on the housing.[2]
ANSI Z136.1 lays out the hazard classes and control measures operators follow around a Class 4 industrial cleaning laser, from beam enclosures to eyewear rated for the wavelength in use.[3]
8 CCR Section 5155 sets the airborne-contaminant exposure limits under Table AC-1 that a facility's fume extraction has to meet for the particulate cleaning throws into the air near precision parts.[4]

Stainless steel begins to ablate surface films near 0.41 J/cm² at 1064 nm, and that onset is far below where the base metal itself takes damage. The damage threshold runs 5 to 12 J/cm², so the wide margin between those two numbers hides a lot of room for a setting that looks clean but is still wrong for the job. A fabricator cleaning 304L before welding can hit a fluence inside that margin that looks clean to the eye while still stripping chromium from the surface layer, leaving a passive film that forms slower and corrodes sooner than an undamaged one. This page covers the shared ablation and thermal behavior across the austenitic, ferritic, and duplex families, and routes grade-specific parameters to [304 stainless](/materials/stainless-steel-304-laser-cleaning) and [316 stainless](/materials/stainless-steel-316-laser-cleaning), since those two see the most pre-weld and marine-service cleaning. It does not set one fluence for the whole family; molybdenum content, surface finish, and the operation (passivation, weld prep, or scale removal) each shift where that safe range sits. Readers doing weld prep should also check the [weld passivation](/applications/stainless-steel-weld-passivation-laser-cleaning) page for the chromium-depletion risk in more depth.

A nanosecond fiber laser removes aluminum oxide film starting at 0.33 J/cm2 fluence, with the full removal range extending through 1.09 J/cm2. Within that band the mechanism shifts from spallation to sublimation, so the correct setting depends on alloy and film thickness rather than one fixed number. The same physics shows up in [weld prep](/applications/weld-prep-laser-cleaning-applications), on [anodized aluminum](/contaminants/anodized-aluminum-laser-cleaning), and in [suspension-arm cleaning](/videos/porsche-911-upper-suspension-arm-laser-cleaned-bGLki9u3). Aluminum's high thermal conductivity and low melting point near 660 C narrow the margin between stripping the oxide and marking the base metal, and ANSI Z136 beam safety practices apply at every fluence in that range.

Laser cleaning removes rust, mill scale, and weld discoloration from steel without media, holding fluence near a 1.5 J/cm² cleaning floor and stopping short of the 4.5 J/cm² mark that scars bare metal. Intact mill scale still needs mechanical pre-treatment under AMPP SP21511-1 first. Compare with [stainless steel](/materials/stainless-steel-laser-cleaning) or [cast iron](/materials/cast-iron-laser-cleaning) laser cleaning when the substrate is mixed, and see [weld prep](/applications/weld-prep-laser-cleaning-applications) for the fabrication step this feeds.

Requires reading the anodize class before setting energy, because thin dyed [Type II anodize](/materials/aluminum-laser-cleaning) clears near a few joules per square centimeter in the near infrared while thick Type III hardcoat pushes energy close to where the [aluminum alloy](/materials/aluminum-laser-cleaning) itself starts to melt before the last film is gone. The film is grown [alumina](/materials/alumina-laser-cleaning), not a corrosion product, so a matching offcut decides which side of that line a given part sits on rather than a fleet-wide default setting. Laser surface work on 7075 aluminum shows how alloy-specific energy bands matter once the oxide land has to clear without melting the metal under it (Shao et al. 2022).

Laser cleaning strips copper patina, the greenish or brown corrosion film copper and bronze build over years outdoors, without the wire brushing or acid dips that scratch or stain the metal underneath. The beam ablates the oxide and carbonate layers in place, so a roof panel, statue, or busbar keeps its original surface profile through the pass. It will not reverse a deep pit already etched into the metal, match a patina shade a conservator wants kept, or clear a large surface in one blanket setting; patina thickness and age both change how many passes a job needs before the copper is ready for inspection.

A pulsed fiber laser strips PVD and CVD hard coatings, CrN, TiN, TiAlN, CrTiAlN, and DLC, from tool steel and cemented carbide without a hot alkaline bath or media blast, and the same beam clears Type III hardcoat anodize from aluminum. Removal fluence is coating and substrate specific, not a single fleet number, and a separate study clearing titanium oxide needed its own coupon-proven band near 5 to 7 J/cm², with residue remaining below it and cracking above it, the same chemistry-and-substrate sensitivity a hard-coating strip job has to respect before running a full tool through the cell.

Laser cleaning removes mill scale, oxide layers, and weld residue from fabricated metal parts without abrasive media or chemical strippers. Shops handling [steel](/materials/steel-laser-cleaning), [aluminum](/materials/aluminum-laser-cleaning), and [stainless steel](/materials/stainless-steel-laser-cleaning) stock use the process ahead of [weld prep](/applications/weld-prep-laser-cleaning-applications) to strip [mill scale](/contaminants/mill-scale-magnetite-laser-cleaning) and [oxide scale](/contaminants/oxide-scale-laser-cleaning) before joints go together. The method suits selective cleaning on formed parts, brackets, and structural members where masking or dust containment would slow a chemical line. It does not replace bulk shot blasting on large flat stock, and it does not strip thick paint or coatings in one pass the way a grinder does. Fabricators pair laser cleaning with existing surface prep steps rather than swapping out an entire finishing line.

Semiconductor cleanroom tooling leaves the bay so a pulsed head can lift process film from open faces without throwing grit into ISO air. [Stainless steel](/materials/stainless-steel-laser-cleaning) shields, [aluminum](/materials/aluminum-laser-cleaning) kits, and [titanium](/materials/titanium-laser-cleaning) parts go back only after extraction and a real cleanliness check, not a bright-metal look. Wet recovery that still uses HF is a different job than [injection-mold tooling](/applications/injection-mold-tooling-laser-cleaning).

High-pressure die-casting tooling fails for a different reason than an [injection mold](/applications/injection-mold-tooling-laser-cleaning): molten [aluminum](/materials/aluminum-laser-cleaning) reacts with iron in [H13 cavity steel](/materials/tool-steel-laser-cleaning) to form a hard Fe-Al intermetallic layer that raises cavity roughness and locks a shot in place long before surface dirt alone would cause a reject. OSHA Table Z-1 caps total nuisance dust at 15 milligrams per cubic meter in an enclosed die-casting cell, and laser cleaning strips that intermetallic film and the carbonized release residue around it without the abrasive media that would raise roughness further. The process also leaves PVD and nitride anti-soldering coatings intact, where abrasive blasting cuts through them in one pass. It does not recoat a worn insert or re-cut a soldered cavity back to print dimensions.
Glass bead blasting caps its blast pressure near 60 psi and still throws dust that needs collection, while a laser line skips both the media bill and the collection line entirely. That pressure ceiling also decides how many times a batch of beads survives before it fractures and stops giving an even peened finish, a tradeoff that matters most on cosmetic work bound for [stainless steel](/materials/stainless-steel-laser-cleaning) or [aluminum](/materials/aluminum-laser-cleaning) panels. A facility weighing glass bead blasting against other legacy methods, such as [sandblasting](/applications/laser-cleaning-vs-sandblasting) or [dry ice blasting](/applications/laser-cleaning-vs-dry-ice-blasting), usually finds the same split. A laser line holds dimension and skips consumables. It will not reproduce the uniform satin texture glass bead media leaves on its own. Facilities that need that specific cosmetic finish keep the glass bead step for the finish itself, even after a laser handles the contamination work.
Steam-assisted laser cleaning removes better than 90%[6] of particles once they are 60 nm or larger, while staying below the point where the silicon substrate begins to melt. That combination lets a precision shop clear sub-micron debris from a wafer or optic without opening a thermal risk on the surface underneath.
A 1 µm[7] aluminum-oxide particle sits well inside the range that dual-beam laser-cleaning trials have tested against silicon damage thresholds, and published results report removal as high as 97.8% while leaving the surface at roughly 0.027 µm in local roughness (Sz), close to the pre-clean baseline. Matching the pulse pairing to that particle size is what keeps the removal number high without also raising the roughness reading afterward.
Oil-film contamination on a precision optic changes the damage threshold well before any residue is visible to the eye. Testing on the input face of fused-silica optics at 355 nm[8] found that a 4 ng/mm² oil film already cuts transmissivity by about 1%, and by 6 ng/mm² the laser-induced damage threshold drops roughly 10% from the clean baseline. A fingerprint-level film, not a visible smear, is enough to change how much energy the coating can.
Photoacoustic cleaning on silicon wafers and precision metals runs on a pulsed Nd:YAG laser at 1064 nm, the wavelength published trials confirm for that particle-removal mechanism. The pulse builds a brief pressure wave above the surface that pops particles loose without the beam ever touching the coating underneath.