OSHA
View official documentation (opens in new tab)Requires labels and safety data sheets for mold release agents and resin additives so shop staff know what fumes a laser pass on residue-coated tooling could release.[1]
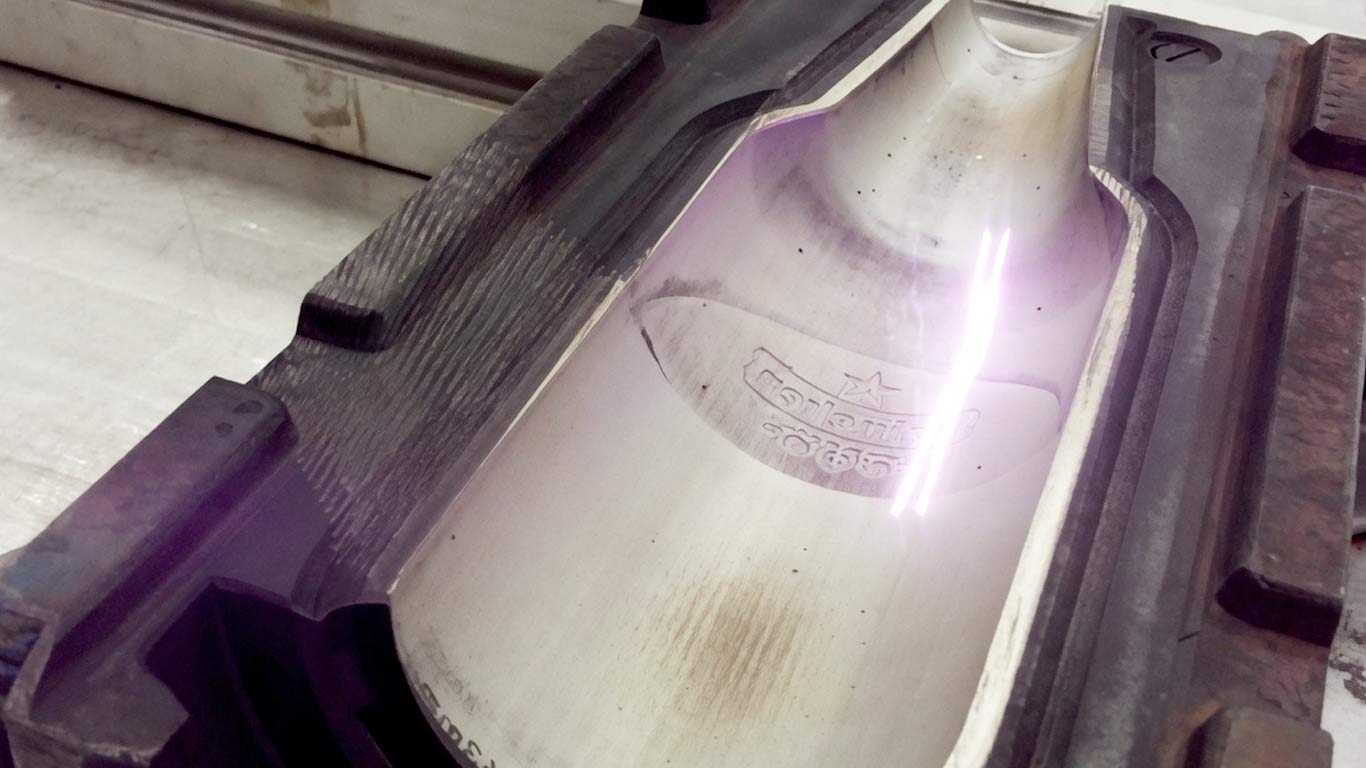
Laser cleaning removes polymer residue, release-agent film, and light oxidation from injection mold cavities and cores without abrasive blasting or solvent soak that can round vent edges or scar a polished finish. The method suits tool steel cavities and cores where mold release and carbon buildup need to come off between runs, and it fits the broader class of mold and die cleaning work where dimensional tolerances matter more than speed. It does not replace deep hot-runner tip service, which lives on the separate hot-runner cleaning page, and it does not treat die-cast aluminum tooling, since that metal responds differently to the same fluence. Downtime gains from switching to laser cleaning depend on mold complexity, residue type, and current cleaning method, so any comparison against manual teardown needs mold-specific timing rather than a blanket figure.
| Final results | The laser pass clears tool-steel cavities and cores of mold release, plate-out, pigment, and burnt resin, and vents and polish stay as machined. |
| Speed and ease | The in-press laser pass clears that release, plate-out, pigment, and resin without the 2 to 3 hour hand-cleaning pull-and-cooldown step. |
| Contaminants | The soil is mold release, plate-out, pigment, and burnt resin in the cavity and vents, plus grease, waxy film, color-pigment staining, and surface rust. |
| Methods | Reaching that residue usually means scrubbing or blasting it loose by hand, and even an ultrasonic bath still requires the mold to come apart first. |
| Challenges | A steel wire brush permanently increases surface roughness on polished cavities, and once that damage is introduced it needs full mechanical re-polishing from 400 grit through 2000 grit plus diamond paste to fix. |
Injection mold tooling needs cleaning because mold release agents, resin off-gas, and carbonized residue build a thin film on the cavity, core, and vent channels with every shot, while the open mold is still run under ANSI Z136 safe-use practice for the laser class in service. Laser cleaning removes that film below the threshold that would mark the steel (Ahn 2012), through thermal ablation and the plasma shock the beam generates at the surface (Zhu.
Laser cleaning removes the contaminant film and stops at bare steel, so it does not take measurable material off the cavity or core. Dimensions and texture stay inside the tolerance band the tool was built to hold.
A PVD or CrN coating requires careful fluence control, since laser cleaning strips it once settings match bulk steel instead of a coating only a few microns thick. The same selective ablation that strips TiAlN coating from cutting tools for reuse (Proc. IMechE 2011) also works against mold coatings when power runs too hot for the layer thickness, a tradeoff a vendor case study confirms across several coating systems (Adapt Laser, PVD removal). Technicians qualify.
Mold tooling typically requires a cleaning check every 5,000 to 10,000 shots, though the right interval depends on the release agent system in use, since release agents split into several distinct chemical families with different buildup rates (Explore Composites release-systems guide). A tool running a heavily filled or glass filled resin can show a visible haze on the cavity in a single shift, while a smooth cavity running an unfilled polypropylene part may run for.
Fiber delivery runs the beam around obstacles a blasting nozzle cannot approach at the correct angle, reaching ejector pin bores, vent channels, and shallow texture directly. A technician runs the head by hand or on a small fixture for repeat jobs, working the hardest to reach spots first while the tool is still warm.
Cleaning removes carbon buildup and release agent residue from the cavity surface of injection mold tooling without disturbing the finish underneath. That same cleaning pass crosses cavity walls, plating, texture, and hardened steel in one pass, and a setting that clears residue safely in one area can wash out a texture pattern or crack a hardened edge in another. Plants that skip witness block testing or run the same power across pins, ribs, and cavity walls risk turning a routine cleaning pass into a re-texturing or re-plating job. Vents, gates, and thin ejector pins are especially heat sensitive because their mass cannot absorb energy the way a thick cavity block can.[1][2]
| Condition | Consequence |
|---|---|
| Laser power or pass count set for a smooth cavity wall is carried over onto an EDM-textured or vapor-honed surface.[1],[2] | The texture pattern flattens or streaks, so molded parts lose the intended surface finish and the cavity needs re-texturing before the mold runs again. |
| A laser pass runs at full power over chrome-plated, nickel-plated, or DLC-coated cavity surfaces without confirming the coating first.[1],[2] | The plating thins or lifts at the edges, exposing base steel that corrodes and wears faster than the coated surface did. |
| A laser beam dwells too long on thin ejector pins, small core pins, or fine rib detail instead of the thicker cavity block around them.[1],[2] | Localized heat softens or distorts the pin, so it binds in its bore or wears out of tolerance faster than the surrounding tool steel. |
| Narrow vents and gate lands are cleaned quickly along with open cavity surfaces instead of being checked on their own.[1],[2] | Leftover carbon film in a vent blocks gas escape, and trapped gas burns the resin at that spot on the next shot, a defect shops call the diesel effect. |
| A single cleaning pass is expected to clear release agent residue that has built up in fine ribs, undercuts, or textured corners.[1],[2] | Residue trapped in tight geometry keeps transferring into molded parts, causing sticking, short shots, or a hazy finish that a quick visual check misses. |
| A cleaned mold is closed up or put into storage while cooling channels, vents, or cavity surfaces are still damp from the cleaning process.[1],[2] | Trapped moisture flash-rusts the bare steel overnight, and the next parts run shows corrosion pitting transferred onto the cavity finish. |
Injection mold tooling requires precise cleaning between production runs because carbon deposits, off-gassing residue, and light rust build up on vents, parting lines, and ejector pin bores. A single mold can cost more than $100,000 and run over a million parts before replacement, so a laser cleaning pass has to strip that buildup without touching the polished or textured cavity surface underneath it. The energy stays low enough to leave hardened steel and chrome plating unmarked, which matters most on vents and thin ejector pin channels where a single overheated pass can round a sharp edge that took weeks to cut. Shops can run this cleaning on a hot mold right on the press, skipping the cooldown a chemical soak would need, and checking cavity depth and vent width after each pass instead of guessing how many passes a given residue layer needs.[1][2]
Formaldehyde governs the compliance picture whenever leftover acetal or POM resin scorches on a hot mold cavity surface, because Cal/OSHA regulates that vapor under a rule written specifically for formaldehyde, not a generic contaminant table. A laser pass that heats resin residue before it vaporizes can release the same compound, so the shop treats it as a hazardous substance under federal hazard communication rules and tracks other airborne byproducts under Cal/OSHA's general contaminants table. ANSI's laser safety standard covers the beam side of that same cleaning pass, setting eyewear and enclosure rules independent of what the resin gives off. Together these rules define the exposure, labeling, and beam safety a mold cleaning cell needs before the laser starts on residue-coated tooling.[1][2][3][4][5]
Requires labels and safety data sheets for mold release agents and resin additives so shop staff know what fumes a laser pass on residue-coated tooling could release.[1]
Classifies the laser hazard and sets the eyewear, enclosure, and access-control rules a shop follows while cleaning mold cavities in place.[2]
Governs formaldehyde exposure specifically, the vapor released when leftover acetal or POM resin scorches on a hot mold cavity during cleaning.[3]
Sets the airborne contaminant limits that cover other fumes from overheated release agents and resin residue during cleanup.[4]
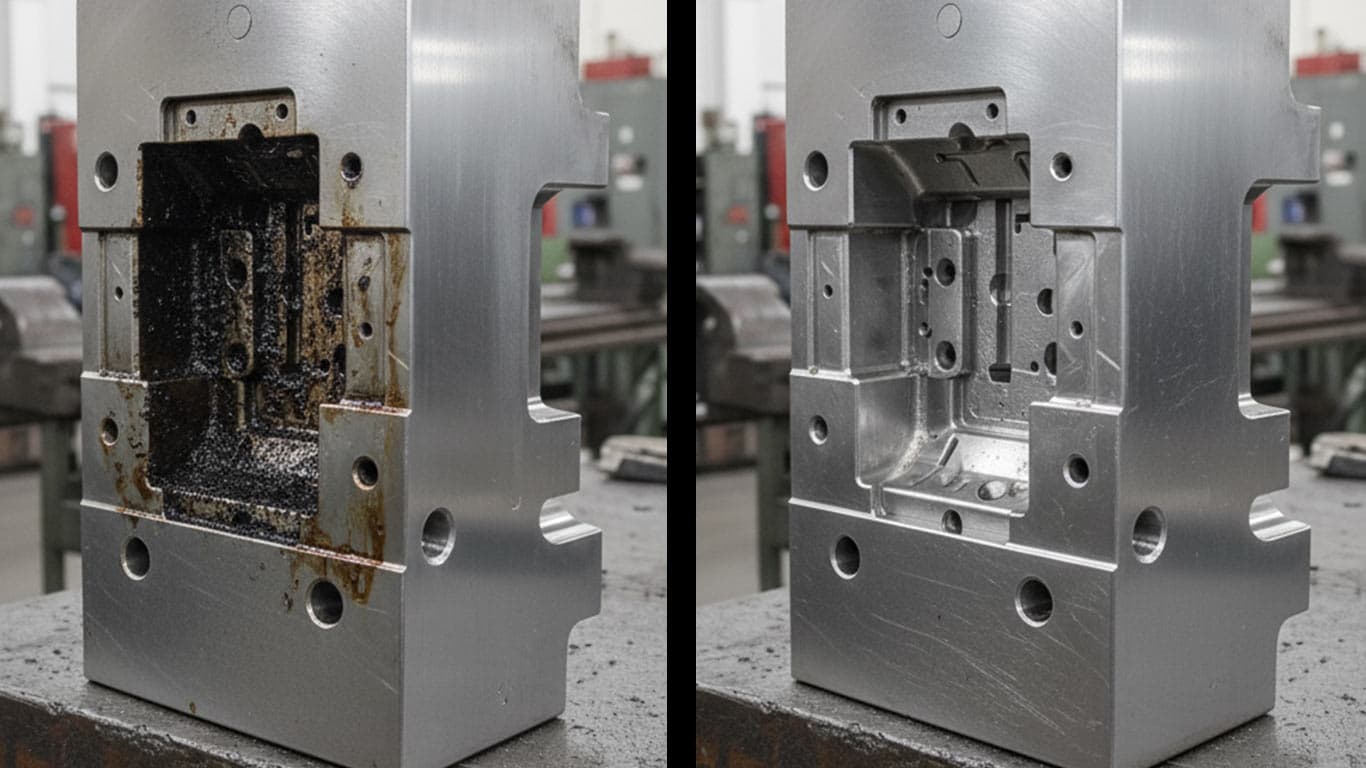
Removing release film and oxide from tool steel works when a pulsed laser stays below the point that draws temper or marks the working face. Hot-work and cold-work grades do not share the same heat limit, so the die steel itself decides the map. Hard PVD skins need their own pass plan. Alloy dust capture stays on for the whole dry job.
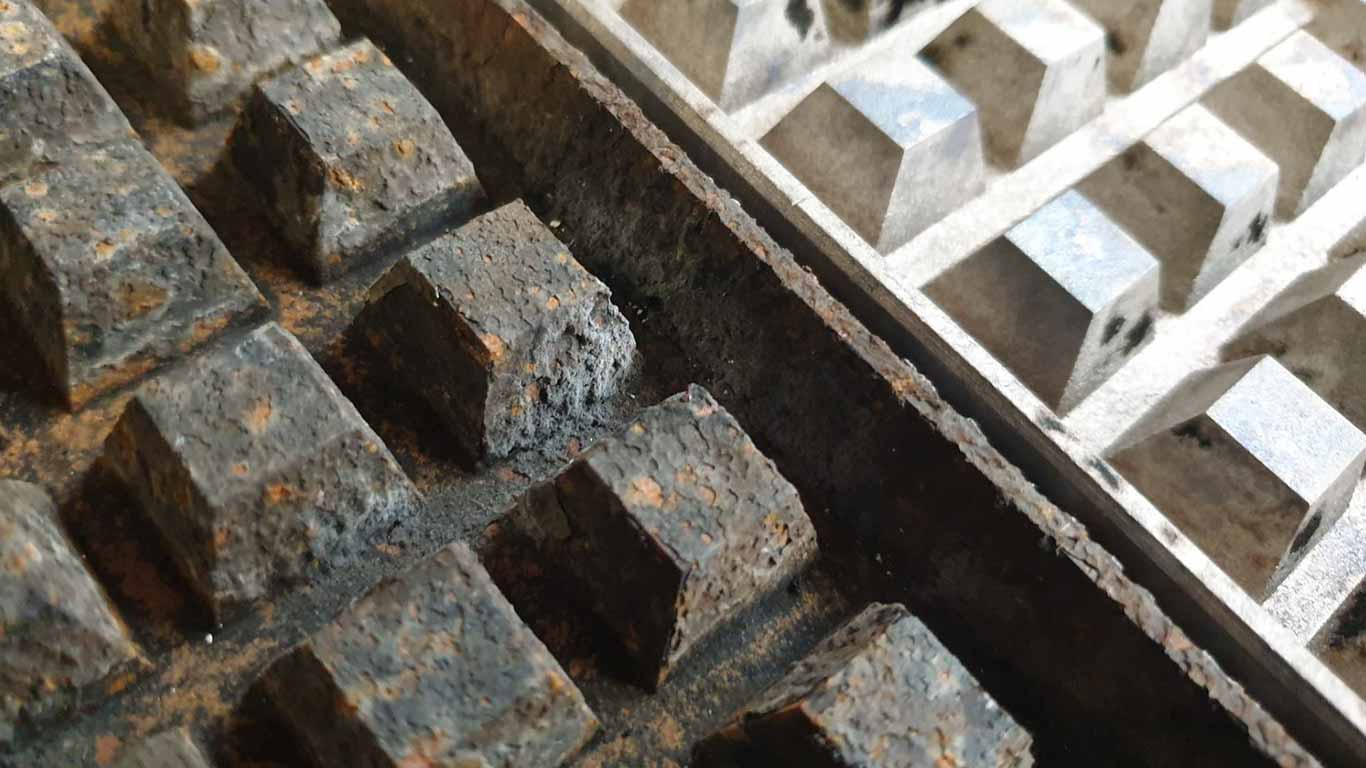
Laser cleaning removes rust, mill scale, and weld discoloration from steel without media, holding fluence near a 1.5 J/cm² cleaning floor and stopping short of the 4.5 J/cm² mark that scars bare metal. Intact mill scale still needs mechanical pre-treatment under AMPP SP21511-1 first. Compare with [stainless steel](/materials/stainless-steel-laser-cleaning) or [cast iron](/materials/cast-iron-laser-cleaning) laser cleaning when the substrate is mixed, and see [weld prep](/applications/weld-prep-laser-cleaning-applications) for the fabrication step this feeds.
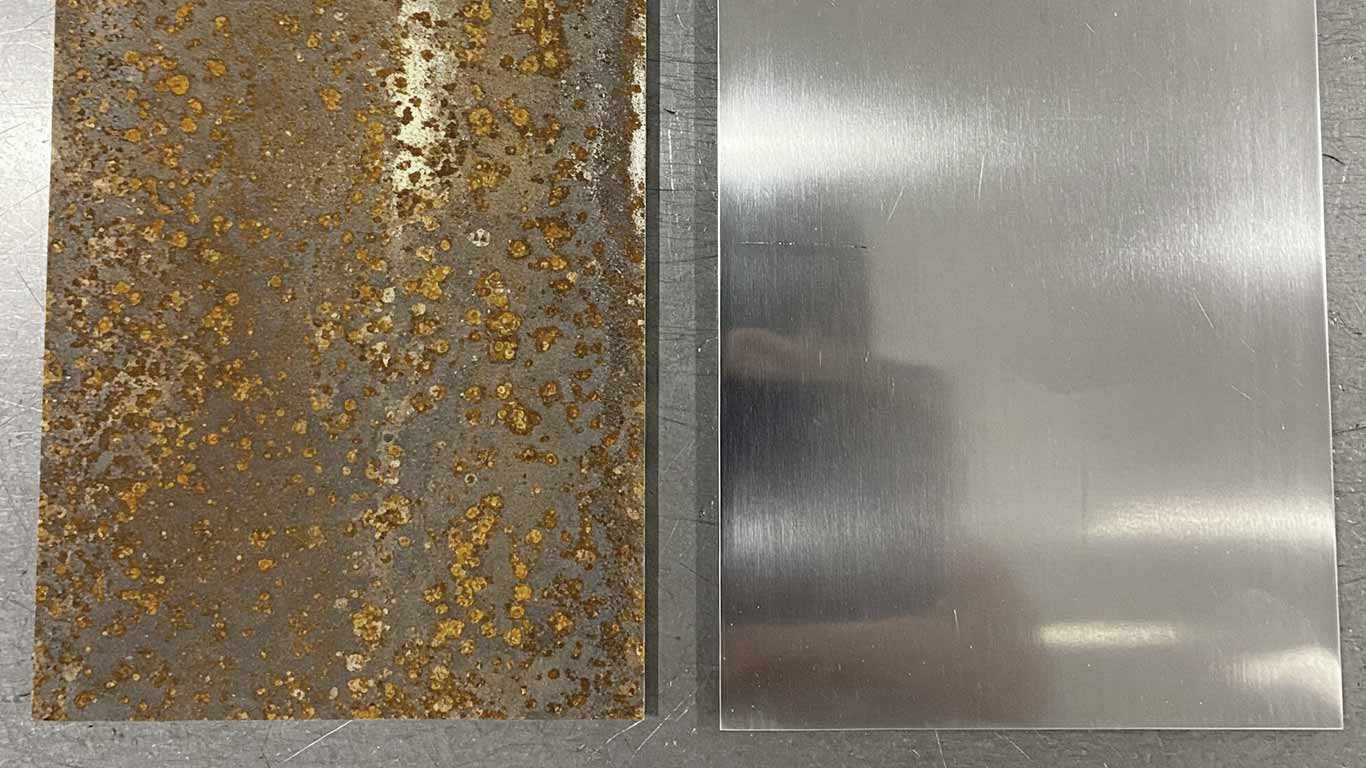
Stainless steel begins to ablate surface films near 0.41 J/cm² at 1064 nm, and that onset is far below where the base metal itself takes damage. The damage threshold runs 5 to 12 J/cm², so the wide margin between those two numbers hides a lot of room for a setting that looks clean but is still wrong for the job. A fabricator cleaning 304L before welding can hit a fluence inside that margin that looks clean to the eye while still stripping chromium from the surface layer, leaving a passive film that forms slower and corrodes sooner than an undamaged one. This page covers the shared ablation and thermal behavior across the austenitic, ferritic, and duplex families, and routes grade-specific parameters to [304 stainless](/materials/stainless-steel-304-laser-cleaning) and [316 stainless](/materials/stainless-steel-316-laser-cleaning), since those two see the most pre-weld and marine-service cleaning. It does not set one fluence for the whole family; molybdenum content, surface finish, and the operation (passivation, weld prep, or scale removal) each shift where that safe range sits. Readers doing weld prep should also check the [weld passivation](/applications/stainless-steel-weld-passivation-laser-cleaning) page for the chromium-depletion risk in more depth.

A hot runner keeps molten plastic flowing through heated manifolds and nozzles inside an [injection mold](/applications/injection-mold-tooling-laser-cleaning), and carbon deposits from degraded resin collect on nozzle tips, gate inserts, and manifold bores over repeated cycles. Laser cleaning removes that carbonized buildup from [tool steel](/materials/tool-steel-laser-cleaning) and [copper](/materials/copper-laser-cleaning) components without abrasive media or solvent soak, so gate tolerances and heater channel clearances stay within the tolerances the mold was cut to. The method strips residue layer by layer and exposes base metal for inspection, but it does not repair a worn gate insert, replace a heater band, or restore a nozzle tip that has eroded past dimension. Technicians still pull the tooling stack apart, mask thermocouple ports, and check continuity before and after each pass. What laser cleaning will not fix is a plugged gate caused by a mechanical defect or a heater that already runs outside its set point; those failures need diagnosis first, not a cleaning pass.
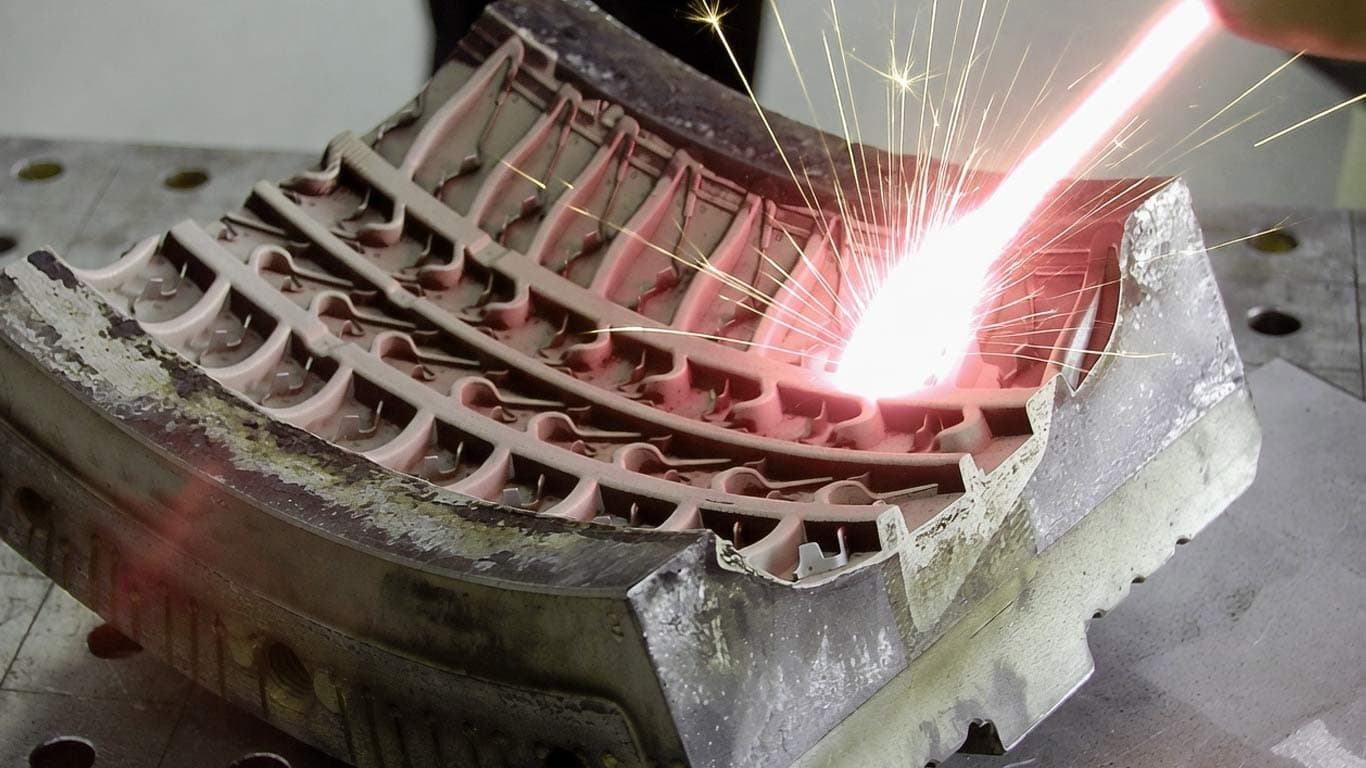
High-pressure die-casting tooling fails for a different reason than an [injection mold](/applications/injection-mold-tooling-laser-cleaning): molten [aluminum](/materials/aluminum-laser-cleaning) reacts with iron in [H13 cavity steel](/materials/tool-steel-laser-cleaning) to form a hard Fe-Al intermetallic layer that raises cavity roughness and locks a shot in place long before surface dirt alone would cause a reject. OSHA Table Z-1 caps total nuisance dust at 15 milligrams per cubic meter in an enclosed die-casting cell, and laser cleaning strips that intermetallic film and the carbonized release residue around it without the abrasive media that would raise roughness further. The process also leaves PVD and nitride anti-soldering coatings intact, where abrasive blasting cuts through them in one pass. It does not recoat a worn insert or re-cut a soldered cavity back to print dimensions.

A compression mold cure film is sulfur bound to the cavity surface during vulcanization, a different residue than the release wax on top of it, and clearing it from [tool steel](/materials/tool-steel-laser-cleaning) cavities needs a narrower fluence band than an [injection mold](/applications/injection-mold-tooling-laser-cleaning) cavity does. Laser cleaning removes the [cured rubber](/materials/rubber-laser-cleaning) film and the wax layer together while holding cavity texture at ARPM Class A1 tolerance near 0.10 millimeter, where an abrasive blast would round the vent lands that let trapped air escape mid-cure. An inert gas assist keeps sulfur vapor from recombining on the warm steel behind the beam path. This does not reset a mold that has already lost its vent geometry to wear, and it does not replace a scheduled repolish once the cavity surface itself has pitted.
Teardown labor extended each chemical soak cycle well past the actual time the mold cavity spent in the tank, since techs still had to pull inserts, ejector pins, and vents before dipping them. Hand scraping cut into hardened cavity surfaces after enough passes, and a pitted mold face called for costly re-polishing or early replacement. Dry ice blasting worked on the press without disassembly, yet it depended on a steady supply of CO2 pellets, a consumable cost that never stopped. Laser cleaning removed carbon buildup and mold release residue from vents and parting lines without contact media, so material spend dropped along with the risk of scratching fine tool steel. Some shops ran that laser process through robotic work cells built into the existing line, which trimmed the hands-on labor that soak tanks and blast cabinets still needed. The equipment tradeoff stayed real: a laser system asked for a bigger upfront investment than a blast cabinet or solvent tank, though it kept running without buying more abrasive or chemical stock.[1][2][3][4][5][6][7][8][9]
| Method | Cost per 100 sq ft | Hourly Rate | Consumables/hr | Setup Cost | Cleaning rate | Surface damage |
|---|---|---|---|---|---|---|
| Sandblasting / Abrasive Blast | 425 USD | 145 USD/hr | 55 USD/hr[3] | 200 USD | 150 sq ft/hr[2],[3],[4] | High: Abrasive action creates measurable surface profile (1.5–4 mils anchor pattern on steel). Causes pitting, warping, or erosion on softer or delicate materials.[8] |
| Soda Blasting | 329 USD | 155 USD/hr | 90 USD/hr | 175 USD | 200 sq ft/hr | Low to moderate: Softer than sand or grit at Mohs 2.5. Does not create significant surface profile on steel. Can etch soft metals (aluminum, copper) or sensitize wood grain. |
| Dry Ice Blasting | 750 USD | 350 USD/hr | 150 USD/hr | 550 USD | 200 sq ft/hr[5] | Low to minimal: Non-abrasive thermal shock mechanism; dry ice sublimates on impact with no surface profile or residue. Some thermal stress risk on heat-sensitive substrates. |
| Dustless Blasting | 641 USD | 375 USD/hr | 80 USD/hr | 250 USD | 130 sq ft/hr | Moderate: Water suppression reduces abrasion heat and dust, but abrasive media still creates surface profile.[8] |
| Laser Cleaning | 500 USD | 400 USD/hr[7] | 0 USD/hr | 0 USD | 80 sq ft/hr[6],[7] | Minimal to none: Non-contact ablation vaporizes contaminants without abrading or mechanically stressing the substrate. Parameter-controlled at 300W (Netalux Kamino class).[9] |


