

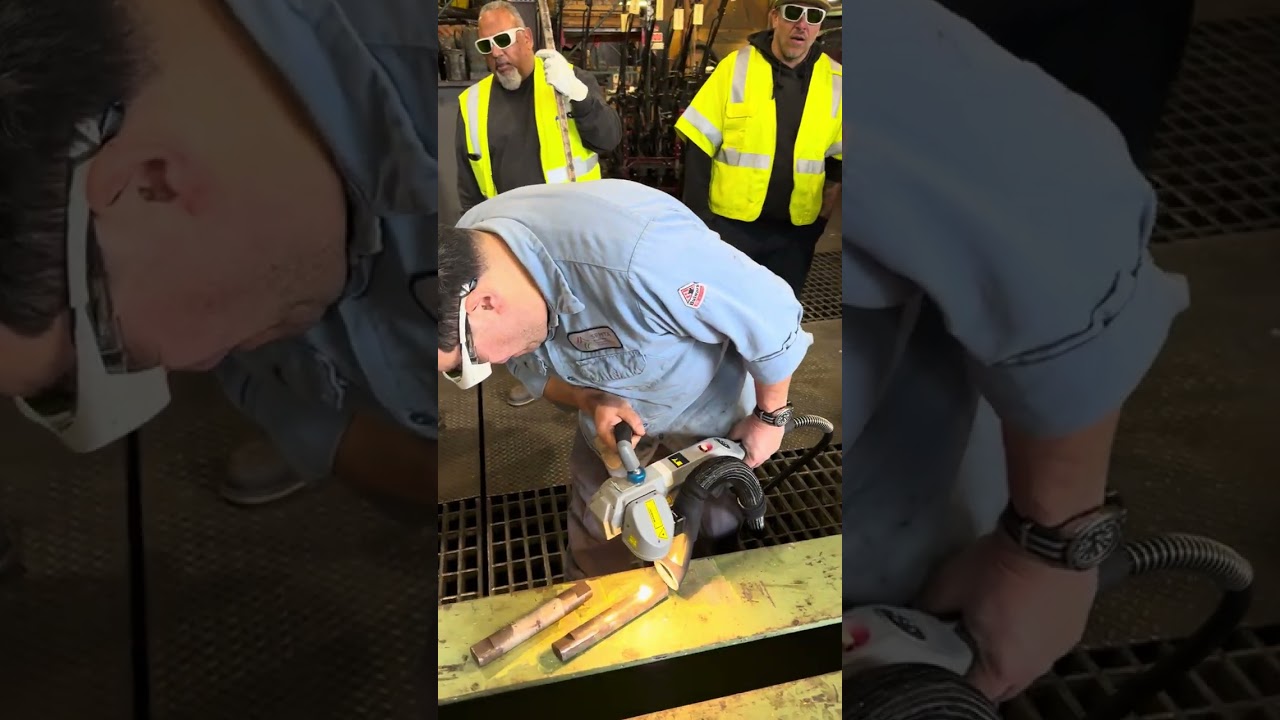

Steel Laser Cleaning
Laser cleaning removes rust, mill scale, and weld discoloration from steel without media, holding fluence near a 1.5 J/cm² cleaning floor and stopping short of the 4.5 J/cm² mark t...


Laser cleaning removes rust and old paint from the iron and steel grip mechanisms, cable channels, and running gear that keep San Francisco's cable cars moving, the work covered by laser rust removal and laser paint and coating removal in the Bay Area. The beam handles these parts the way it handles other steel and cast iron components: it strips corrosion and coatings down to sound metal without grinding, sandblasting, or chemical stripping. It does not repair cracked castings, replace worn brake shoes, or restore the redwood body panels and wood framing, which need carpentry and refinishing, not a laser. On a heritage fleet like this one, the cosmetic and corrosion work on metal parts stays a separate job from any structural or wood restoration.
Short Fv8Monhux-c shows pulsed laser clearing soils from San Francisco cable car steel while hardware stays readable.
Laser cleaning removes iron oxide rust from steel down to bare metal without grinding wheels, abrasive blasting, or chemical strippers. The beam ablates the oxide layer while leaving sound steel underneath intact, so a part keeps its original dimension and surface finish through the pass. It will not reverse pitting the rust already caused, repair corrosion damage done to the substrate, or clear a part in one blanket setting; rust depth and iron oxide type both change how many passes a shop needs before the surface is ready for inspection.
Requires matching the paint system and substrate pairing before setting energy, because a thin single topcoat on [steel](/materials/steel-laser-cleaning) clears at a fraction of the fluence a multilayer primer stack on [aluminum](/materials/aluminum-laser-cleaning) needs, and the substrate sets its own ceiling once the coating is gone. Paint sits as an applied, cross-linked polymer film bonded by mechanical keying and resin adhesion, not a corrosion product, so pigment load and binder chemistry decide more of the setting than the substrate alone. A surface-integrity study on laser-cleaned aluminum alloy carrying a paint layer documents that a visually bare finish does not by itself confirm the metal underneath escaped the pass undamaged (Applied Optics, 2024).
Laser cleaning removes the chromium-oxide and titanium-oxide scale that post-weld and post-anneal heat treatment grows on stainless steel, titanium, and Inconel, clearing the film without a chemical pickling bath. It will not rebuild the chromium that heat already pulled out of the grain boundaries beneath a dark heat-treated color, will not fix titanium alpha case that has already let oxygen diffuse deep into the metal, and will not stop the bare surface from re-oxidizing once it goes back into service heat.
Laser cleaning decomposes mineral oil, synthetic lubricant, and machine grease off steel, aluminum, and stainless steel through fast thermal breakdown of the hydrocarbon film, the same damage-threshold logic that broader laser-cleaning threshold research has documented across very different host materials (Journal of Cultural Heritage, 2000). It is not a substitute for a wet alkaline line degreasing a full rack of parts at once, and it will not clear a bonded hard coating or a thick paint stack sitting on top of the oil.
Laser cleaning fractures the bluish-black magnetite laminate off carbon steel in repeated passes, because mill scale runs roughly four times harder than the plate underneath it. A hot-rolled plate carrying this scale typically needs four or more passes to reach bare metal, while a lighter rust bloom on the same yard stock can clear in one or two. It will not strip in a single rust-grade pass, will not raise the surface to a deep abrasive-blast anchor profile some coating specs still call for, and will not reverse pitting that was already hiding under the scale.

Salt air, not the hourly rate, decides a Bay Area rust job. Laser cleaning takes field [rust](/contaminants/iron-oxide-rust-laser-cleaning) off [steel](/materials/steel-laser-clean...

A Bay Area body shop stripping failed epoxy or polyurethane before recoat runs into a VOC cap near 50 grams per liter on solvent surface prep and spray-line cleanup, and older meth...


