OSHA
View official documentation (opens in new tab)OSHA chemical data entry 205 frames wood dust exposure limits that apply when birch laser cleaning liberates hardwood particulate at the head.[1]
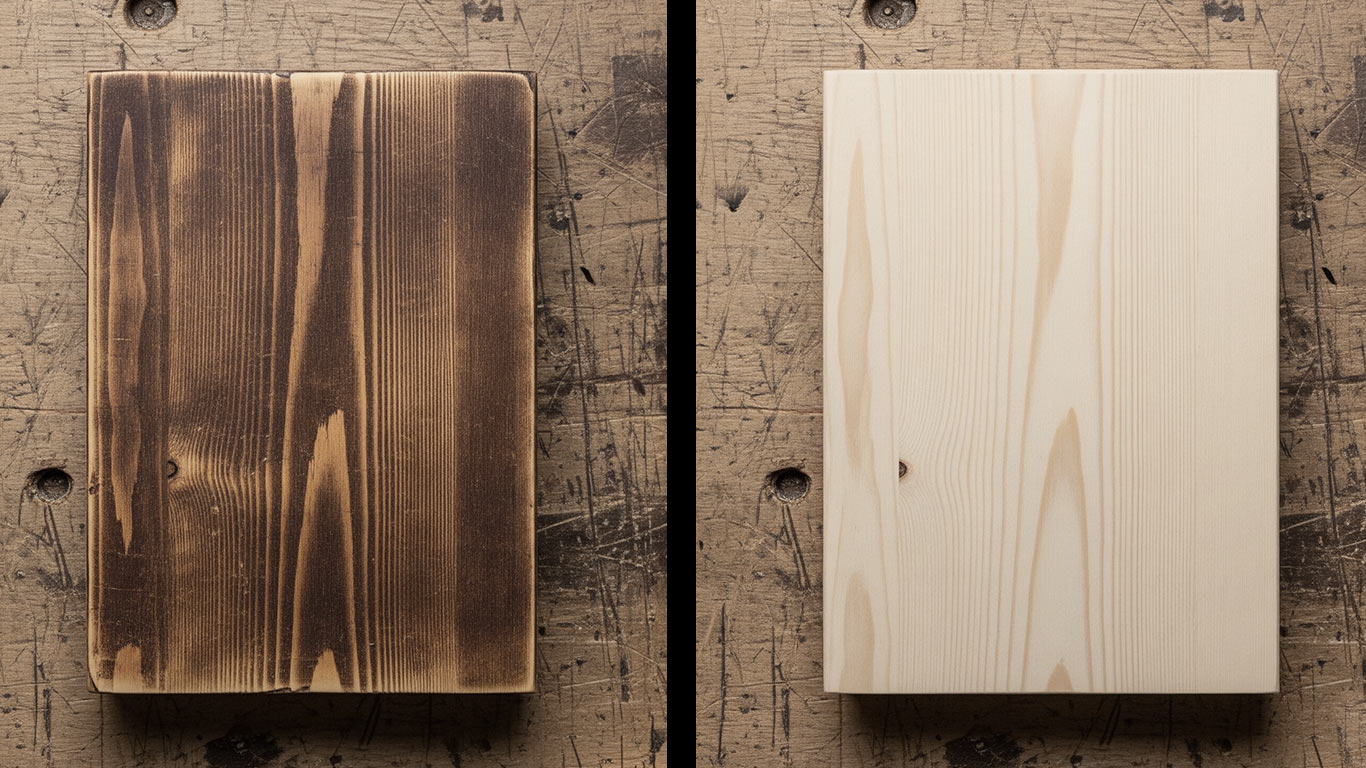
Laser cleaning removes finish and grime from birch furniture without abrasive media or added moisture. Its pale, tight grain scorches more easily than ash's darker, coarser surface or oak's open pores, so cleaning stays gentler and takes more passes rather than fewer, hotter ones. Birch often serves as a face veneer over plywood cores, so cleaning has to stop at that thin surface layer instead of digging toward the substrate. Furniture, cabinetry, and flooring built from birch come out even because its fine pores hold shellac and old finish closer to the top layer than either ash or oak's coarser grain does. It does not reverse UV graying already set into the fibers, and it does not substitute for sanding when the goal is a dimensional cut.
| Final results | Paint, fire char, grease and oil, and atmospheric soiling are off the tight face, and a veneer ply is still continuous. |
| Speed and ease | The duration is not known, but the laser clears the finish without the legacy grit-progression sanding. |
| Contaminants | Paint, soot, grease and oil, and black crust. |
| Methods | Sanding by hand or machine is slow on a tight-grained hardwood like birch. |
| Challenges | Oversanding birch veneer can round over a crisp edge, burn through the thin surface layer, or leave a blotchy, uneven stain. |
Birch absorbs a large share of 1064 nanometer energy and holds heat in pale hardwood stock, so film lifts happen close to the grain. Charted damage for this page sits at 1.5–4.0 J/cm², and hardwood cleaning onset for finish trials lands near 1.0–1.8 J/cm² before char risk rises (Song & Lin 2024) (Aligizaki et al. 2008) (MatWeb material property data).
Birch laser cleaning on this page targets pale hardwood furniture and millwork where finish films must leave without char. Density is about 650 kg/m³ and 1064 nanometer light absorption is about 0.58 on the hardwood property set used for peers (MatWeb material property data).
| Parameter | Value |
|---|---|
| Canonical substrate | Wood — hardwood (birch) |
| Density | 650 kg/m³ |
| Tensile strength | 130 MPa |
| Absorptivity at 1064 nm | 0.58 |
Pale birch can brown when the head dwells too long or when energy outruns the film on the face. Stop at the first brown edge on a coupon, then rebuild the map only after the grain stays light under the same settings.
Start on scrap birch beside the finished piece, not on the show face. Climb energy in short steps while the finish lifts, and freeze the recipe at the first sign of raised fiber or gloss loss before any full-area pass.
Hardwood particulate leaves the head during continuous birch passes, so local exhaust belongs on the tool before production faces run (OSHA Wood Dust Hazards).
Birch sits with oak and maple as a hardwood peer, but pale grain shows browning earlier than darker oaks. Use the hardwood chart band and coupon pale faces more carefully than softwood pine recipes allow.
Name the birch stock before the first pulse, because pale furniture, veneer, and millwork each show char at different dwell budgets. Ladder pulsed 1064 nanometer energy on scrap inside 1.5–4.0 joules per square centimeter, begin finish coupons near the hardwood cleaning onset, and refuse continuous maps once brown edges appear (Aligizaki et al. 2008).
Hardwood dust and visible particulate from birch laser cleaning need capture before production maps. Federal wood-dust chemical data, California airborne contaminant tables, and Bay Area particulate rules set the exposure frame for furniture and millwork booths (OSHA Wood Dust PEL) (Cal/OSHA Title 8 §5155) (BAAQMD Regulation 6 particulate matter).
OSHA chemical data entry 205 frames wood dust exposure limits that apply when birch laser cleaning liberates hardwood particulate at the head.[1]
Title 8 section 5155 lists airborne contaminant limits used for wood dust control during California birch laser cleaning jobs.[2]
Regulation 6 particulate rules still apply to visible plumes from outdoor or bay-door birch laser cleaning on furniture and millwork.[3]
On this chart, common short-pulse 1064 nanometer work on birch stays between about 1.5–4.0 joules per square centimeter with oak and maple peers. That band is the production floor and ceiling for pale hardwood faces on this page, so operators coupon finish lifts before any full-face map and stop when grain browns (Song & Lin 2024).
Birch cleaning fails when pale grain chars under too much energy. It also fails when softwood recipes are copied onto hardwood stock or when wood dust leaves the head without capture. Heritage wood laser work shows why coupon checks belong before continuous faces (Wiedemann laser cleaning wood Pirna).
| Condition | Consequence |
|---|---|
| Fluence above the 4.0 J/cm² hardwood ceiling on pale birch[1] | Char lines, grain darkening, and rejected furniture faces |
| Softwood pine recipe copied onto birch hardwood[1] | Wrong dwell and early char on denser pale stock |
| Continuous passes without wood-dust capture[1] | Airborne hardwood particulate and visible plume risk |
Landmark facade work requires a hidden test patch before pulsed laser cleaning touches any visible elevation. The pass removes soot, pollution crust, and graffiti from [brick](/materials/brick-laser-cleaning) and [limestone](/materials/limestone-laser-cleaning) without the abrasive contact that rounds tooling marks, and it suits [historic masonry](/applications/historic-masonry-restoration-laser-cleaning) jobs that have to stay the gentlest means that still meets the cleaning goal. It will not replace repointing, structural repair, or treatment for deep-rooted growth, and it will not strip [lead paint](/applications/lead-paint-laser-removal-bay-area) from ornamental iron in one pass without a separate low-energy setting and a capture plan. Wet, crumbling, or gilded surfaces stay off the schedule until a conservator says the fabric can take the work.
A Bay Area body shop stripping failed epoxy or polyurethane before recoat runs into a VOC cap near 50 grams per liter on solvent surface prep and spray-line cleanup, and older methylene-chloride paint strippers are barred from sale to industrial users after state toxics regulators listed the chemical as a priority product. A pulsed near-infrared laser removes the coating layer through thermal stress rather than solvent action, so shops can strip [aluminum](/materials/aluminum-laser-cleaning) panels and [steel](/materials/steel-laser-cleaning) frames without touching that VOC limit or generating stripped-paint waste. The exception is thick marine-grade epoxy built up over several coats, where repeated passes near rivets and seams can discolor the substrate unless the operator drops pulse energy and adds a cooling pause between rows. Shops already running [rust](/applications/laser-rust-removal-bay-area) or [lead paint](/applications/lead-paint-laser-removal-bay-area) removal on the same line can cover all three [paint coating](/contaminants/paint-coatings-laser-cleaning#substrateMatrix) jobs from one machine instead of separate chemical-stripping stations.
Precision surface work requires contact-free cleaning because gauge faces, optical flats, and polished tooling scratch under abrasive pads or chemical baths. Pulsed fiber sources remove fingerprint films, particulates, and thin oxide from these finishes without touching the substrate, but a continuous-wave fiber laser is not treated as a safe default here until a peer-reviewed study backs that claim. Semiconductor wafer chambers keep their own class-rated rules on [semiconductor cleanroom tooling laser cleaning](/applications/semiconductor-cleanroom-tooling-laser-cleaning), and release-layer mold work belongs on [mold and die laser cleaning](/applications/mold-die-laser-cleaning-applications) rather than here. Titanium implants and [stainless steel](/materials/stainless-steel-laser-cleaning) precision parts each need a shop-tested cleaning limit, since no single particulate count works across every polished substrate.
Requires matching the paint system and substrate pairing before setting energy, because a thin single topcoat on [steel](/materials/steel-laser-cleaning) clears at a fraction of the fluence a multilayer primer stack on [aluminum](/materials/aluminum-laser-cleaning) needs, and the substrate sets its own ceiling once the coating is gone. Paint sits as an applied, cross-linked polymer film bonded by mechanical keying and resin adhesion, not a corrosion product, so pigment load and binder chemistry decide more of the setting than the substrate alone. A surface-integrity study on laser-cleaned aluminum alloy carrying a paint layer documents that a visually bare finish does not by itself confirm the metal underneath escaped the pass undamaged (Applied Optics, 2024).
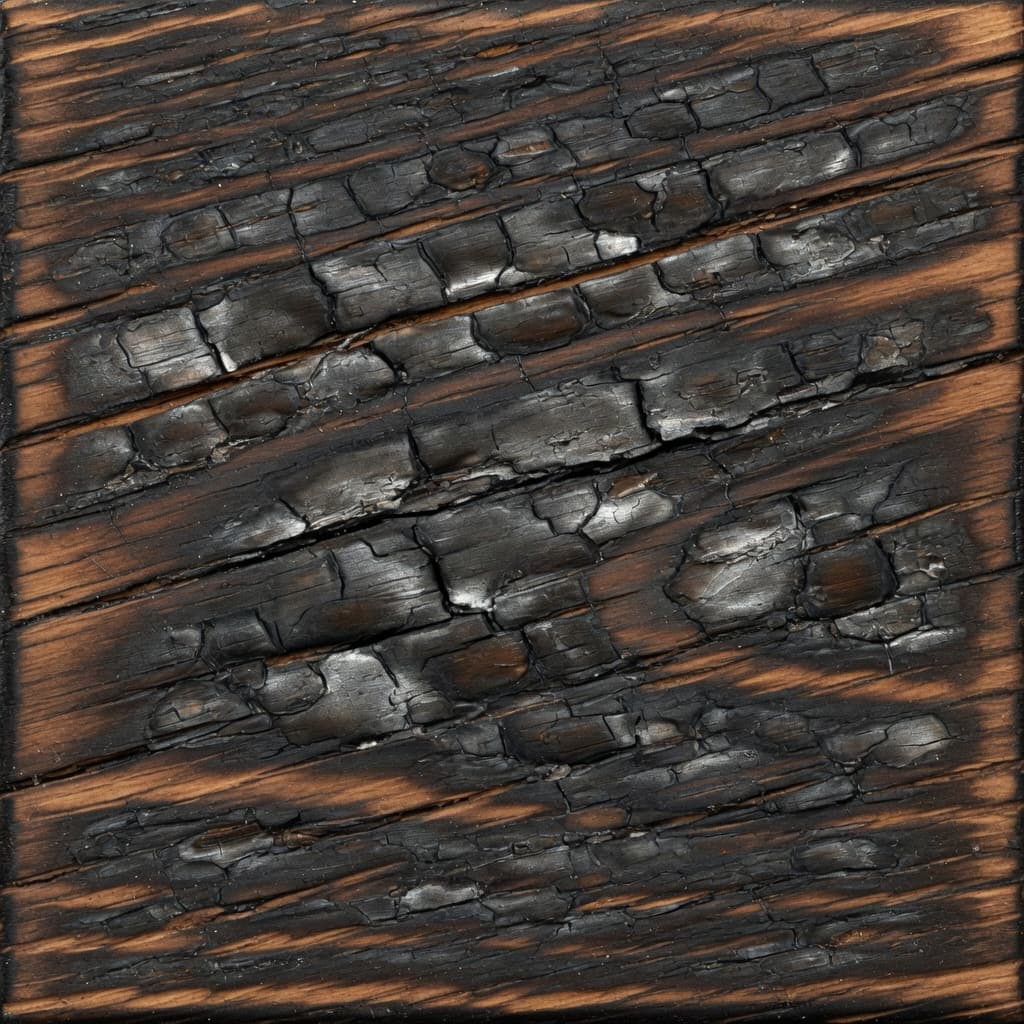
Loose soot and bonded char leave brick, concrete, and painted exterior trim under a dry pulsed near-infrared pass that replaces water, chemical sponges, and grit. Burned drywall paper and timber that already lost structural backing stay outside this page, and any wood still needs a scrap coupon before production settings.
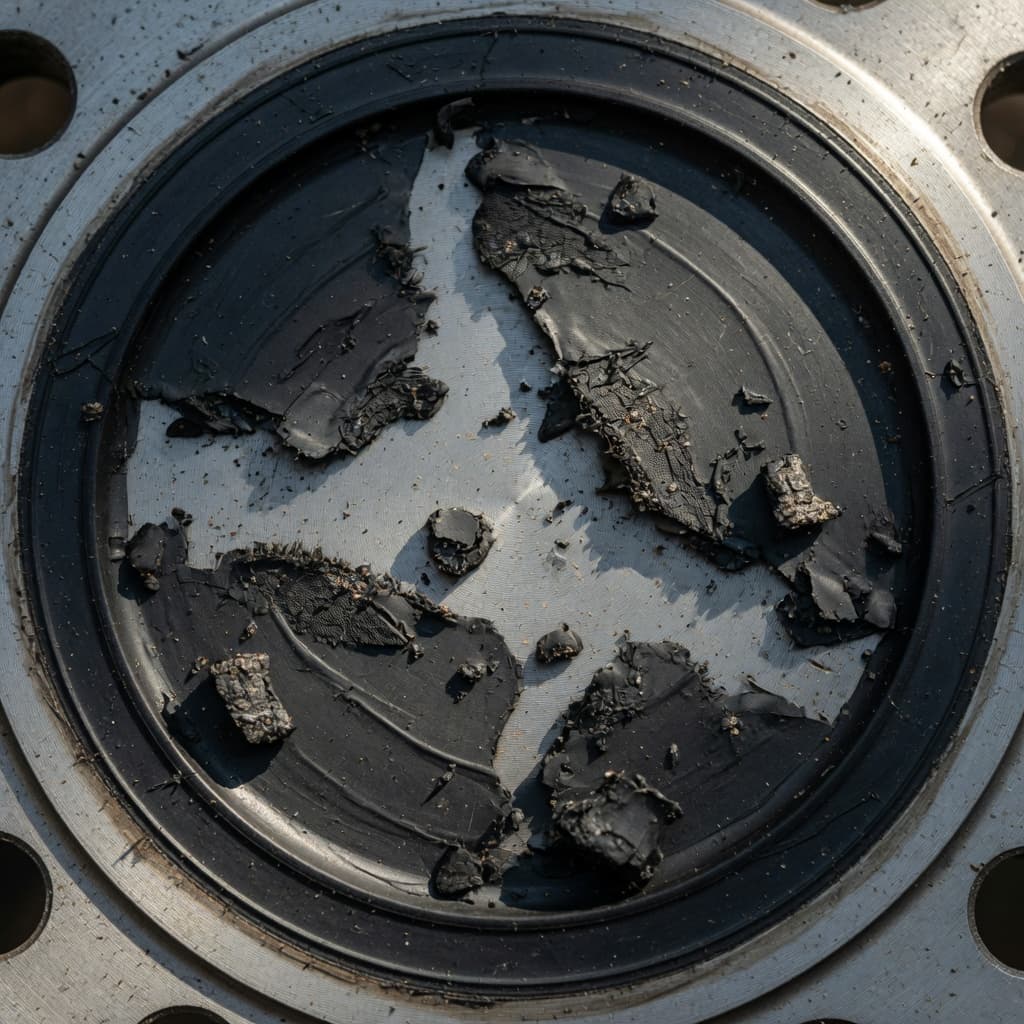
Laser cleaning decomposes mineral oil, synthetic lubricant, and machine grease off steel, aluminum, and stainless steel through fast thermal breakdown of the hydrocarbon film, the same damage-threshold logic that broader laser-cleaning threshold research has documented across very different host materials (Journal of Cultural Heritage, 2000). It is not a substitute for a wet alkaline line degreasing a full rack of parts at once, and it will not clear a bonded hard coating or a thick paint stack sitting on top of the oil.
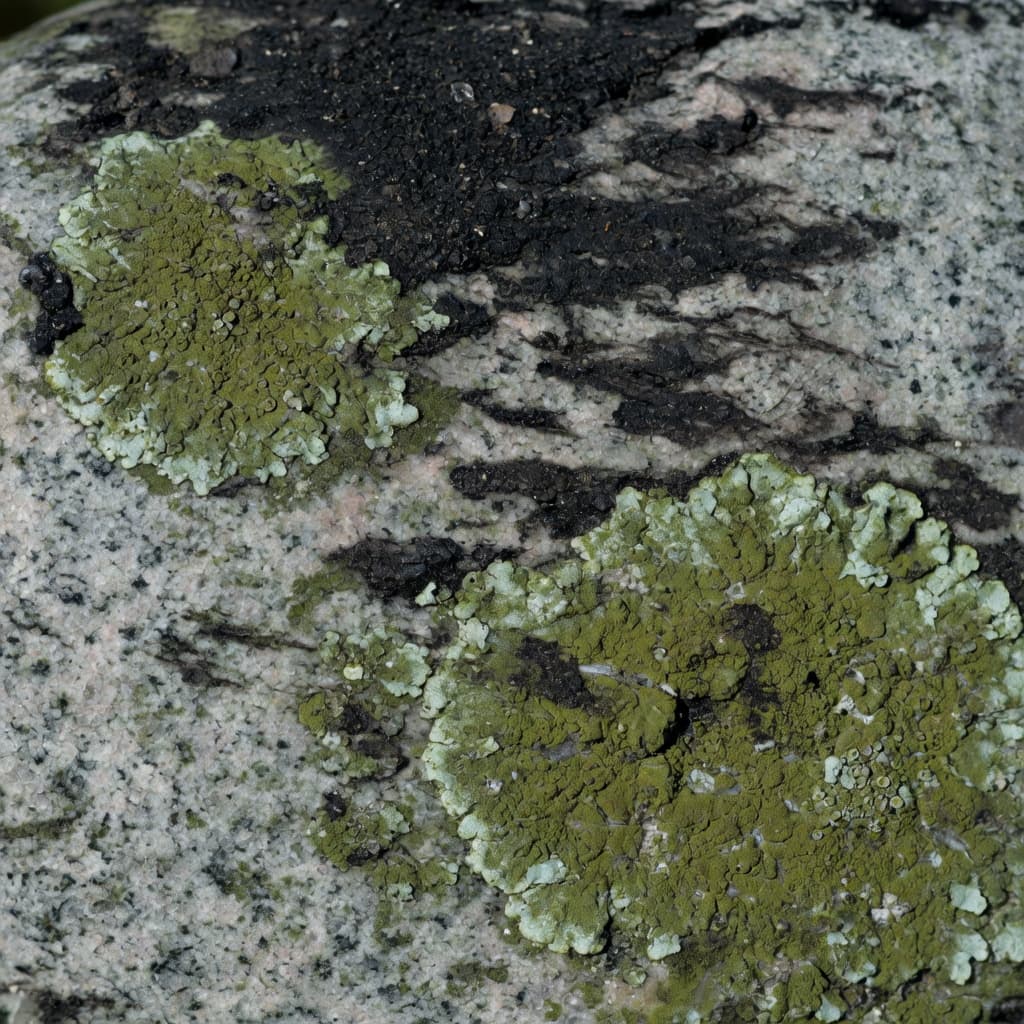
Black crust on marble, limestone, sandstone, and granite is a gypsum-soot film that absorbs far more pulsed-laser energy than the pale stone underneath it, which is what lets a pulsed pass remove the deposit before the parent stone takes damage. Sandstone carries the tightest margin between crust removal and surface damage of the stones on this page, so a labeled offcut test matters there even when a wider marble coupon already cleared.

