
OSHA
View official documentation (opens in new tab)OSHA annotated Table Z-1 frames particulate exposure when dry laser cleaning of soda-lime glass raises glass dust into the breathing zone.[1]
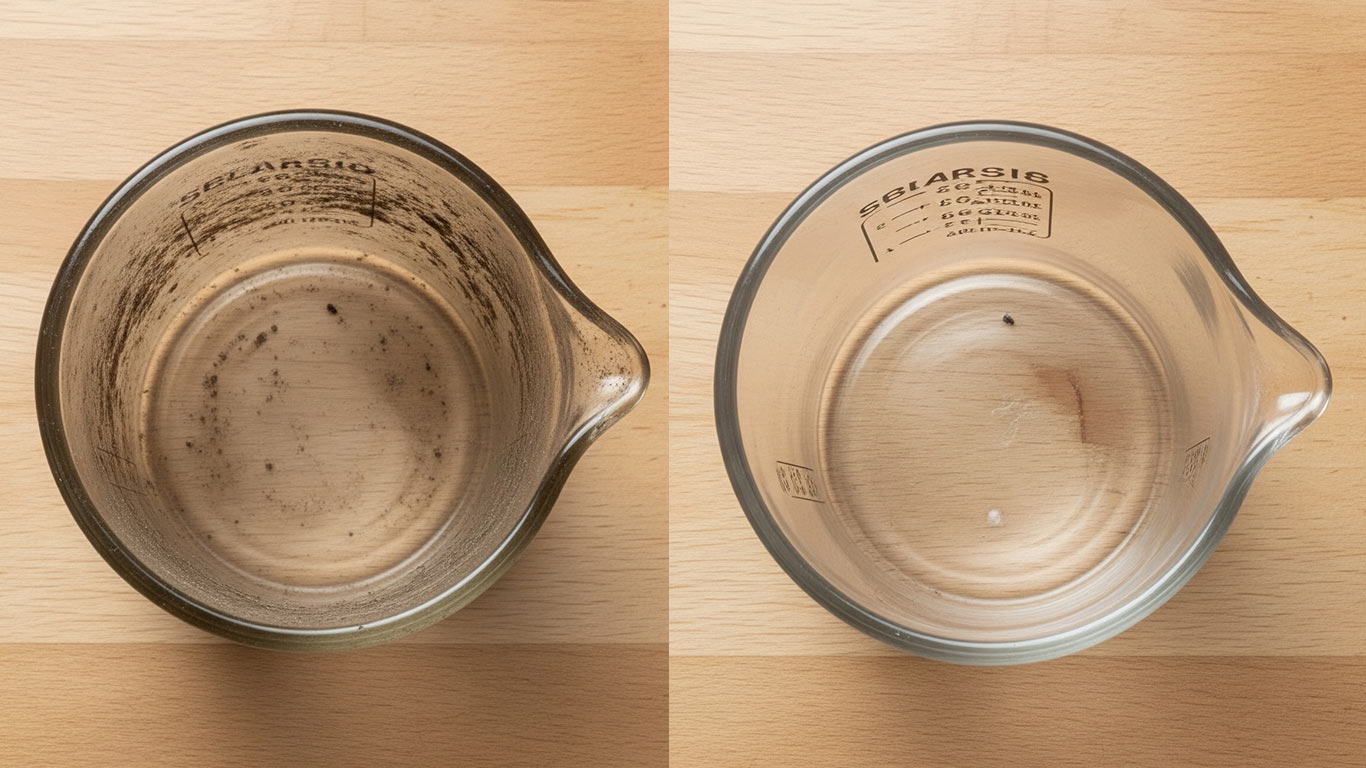
Everyday window and storefront glass can take a pulsed laser pass that removes paint, soot, and surface soil where the film absorbs energy and the pane stays mostly clear. Thin annealed stock can check if heat builds in one spot. Scratch and haze on the glass body are the usual failure. A scrap pane from the same lot maps the pass before a full elevation. Settings meant for metal stay off architectural glass.
| Final results | Paint, atmospheric soiling, grease and oil, and fire char are off the pane, and the glass is not scratched or hazed. |
| Speed and ease | The laser clears the etch mark without the 12-to-15-minute-per-square-foot abrasion-and-polish the legacy fix needs. |
| Contaminants | Paint, black crust, grease and oil, and soot. |
| Methods | Acid-etch damage permanently alters the glass, and regular cleaning cannot remove the resulting foggy, streaky look. |
| Challenges | The pre-polish and polish steps remove a thin layer of glass to erase the etch mark, so an overworked spot can leave a shallow low area or a slight distortion right where it was repaired. |
Soda-lime glass is the everyday architectural glazing stock in windows, storefronts, and curtain-wall panels. Near-infrared pulses mostly pass through the bulk, so cleaning depends on soil absorbing the beam at the face. Name the glass family, stage dust capture, then raise energy on a scrap pane until film lifts without edge checking before any production pass (Research Progress and Challenges in Laser-Controlled Coating Removal).
Soda-lime glass laser interaction is soil-led at 1064 nanometers. Charted light absorption near two percent lets most near-infrared energy pass the bulk while contamination at the face absorbs the cleaning load. Cleaning onset near 10 joules per square centimeter and an upper mark near 18.5 joules per square centimeter frame the production band, and expansion near 9×10⁻⁶ per kelvin still limits thin architectural panes before bulk injury (Sage MST 2025 nanosecond laser review).
Bulk soda-lime glass transmits most near-infrared energy, so the beam mainly heats the contamination layer rather than the glass volume. That is why cleaning works on soiled architectural panes while a bare clear face barely loads heat until energy climbs too high.
Thin architectural glass can crack when heat builds faster than the pane can spread it. Soda-lime has a high expansion coefficient near 9×10⁻⁶ per kelvin, so thin annealed panels need slow energy steps and pauses between overlapping passes before any full job on storefront or curtain-wall glass.
Dry laser work can raise glass particulate into the breathing zone. California Title 8 section 5155 still covers those airborne contaminants on shop and field jobs, so crews stage local exhaust before the first coupon (Cal/OSHA Title 8 §5155 airborne contaminants).
Soda-lime is the common architectural composition with a tighter thermal margin than borosilicate. Borosilicate expands less under the same heat load, so soda-lime coupons usually stop earlier and need more careful overlap control on thin glazing.
Soda-lime glass is the common architectural composition behind float windows and storefront glazing. Charted density sits near 2.5 grams per cubic centimeter with tensile strength around 50 megapascals and thermal conductivity near 1.06 watts per meter-kelvin. Near-infrared light absorption near two percent means soil must carry the cleaning load while the bulk stays mostly clear (MatWeb material property data).
| Parameter | Value |
|---|---|
| Common architectural role | Windows, storefronts, and curtain-wall annealed glazing |
| Density | ~2.5 g/cm³ |
| Thermal expansion | ~9×10⁻⁶ K⁻¹ |
| Near-IR absorptivity | ~0.02 at 1064 nm |
Dry soda-lime glass cleaning needs capture under three named programs. Federal Table Z-1 frames particulate exposure for glass dust in the breathing zone. California Title 8 section 5155 covers airborne contaminants on shop floors. Bay Area outdoor plumes still sit under BAAQMD Regulation 6 visible-emission limits (OSHA Table Z-1) (BAAQMD Regulation 6 particulate matter).[3]
OSHA annotated Table Z-1 frames particulate exposure when dry laser cleaning of soda-lime glass raises glass dust into the breathing zone.[1]
Title 8 section 5155 airborne contaminant tables still govern shop exposure when soda-lime laser cleaning throws glass dust into occupied air.[3]
Regulation 6 limits visible emissions when dry laser cleaning of architectural soda-lime glass creates a plume outside a controlled enclosure.[2]
Soda-lime glass holds a charted production band between cleaning onset at 10 joules per square centimeter and an upper mark at 18.5 joules per square centimeter. That 8.5 joule per square centimeter working width is wider than several tempered peers on the same specialty-glass chart. Thin architectural panes still need scrap coupons because gradient stress can arrive before the upper mark is reached (Appl. Opt. soda-lime ablation thresholds (Nieto 2015)).
Landmark facade work requires a hidden test patch before pulsed laser cleaning touches any visible elevation. The pass removes soot, pollution crust, and graffiti from [brick](/materials/brick-laser-cleaning) and [limestone](/materials/limestone-laser-cleaning) without the abrasive contact that rounds tooling marks, and it suits [historic masonry](/applications/historic-masonry-restoration-laser-cleaning) jobs that have to stay the gentlest means that still meets the cleaning goal. It will not replace repointing, structural repair, or treatment for deep-rooted growth, and it will not strip [lead paint](/applications/lead-paint-laser-removal-bay-area) from ornamental iron in one pass without a separate low-energy setting and a capture plan. Wet, crumbling, or gilded surfaces stay off the schedule until a conservator says the fabric can take the work.
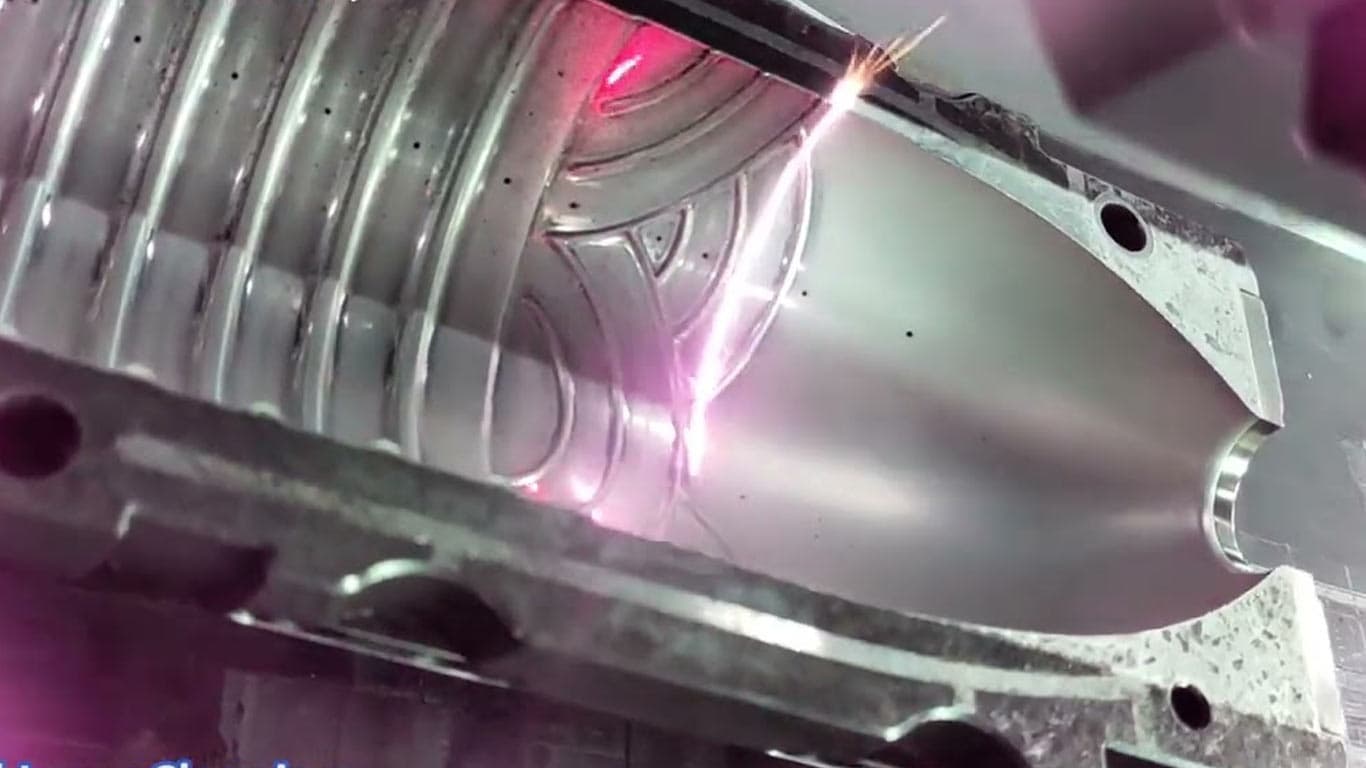
Precision surface work requires contact-free cleaning because gauge faces, optical flats, and polished tooling scratch under abrasive pads or chemical baths. Pulsed fiber sources remove fingerprint films, particulates, and thin oxide from these finishes without touching the substrate, but a continuous-wave fiber laser is not treated as a safe default here until a peer-reviewed study backs that claim. Semiconductor wafer chambers keep their own class-rated rules on [semiconductor cleanroom tooling laser cleaning](/applications/semiconductor-cleanroom-tooling-laser-cleaning), and release-layer mold work belongs on [mold and die laser cleaning](/applications/mold-die-laser-cleaning-applications) rather than here. Titanium implants and [stainless steel](/materials/stainless-steel-laser-cleaning) precision parts each need a shop-tested cleaning limit, since no single particulate count works across every polished substrate.
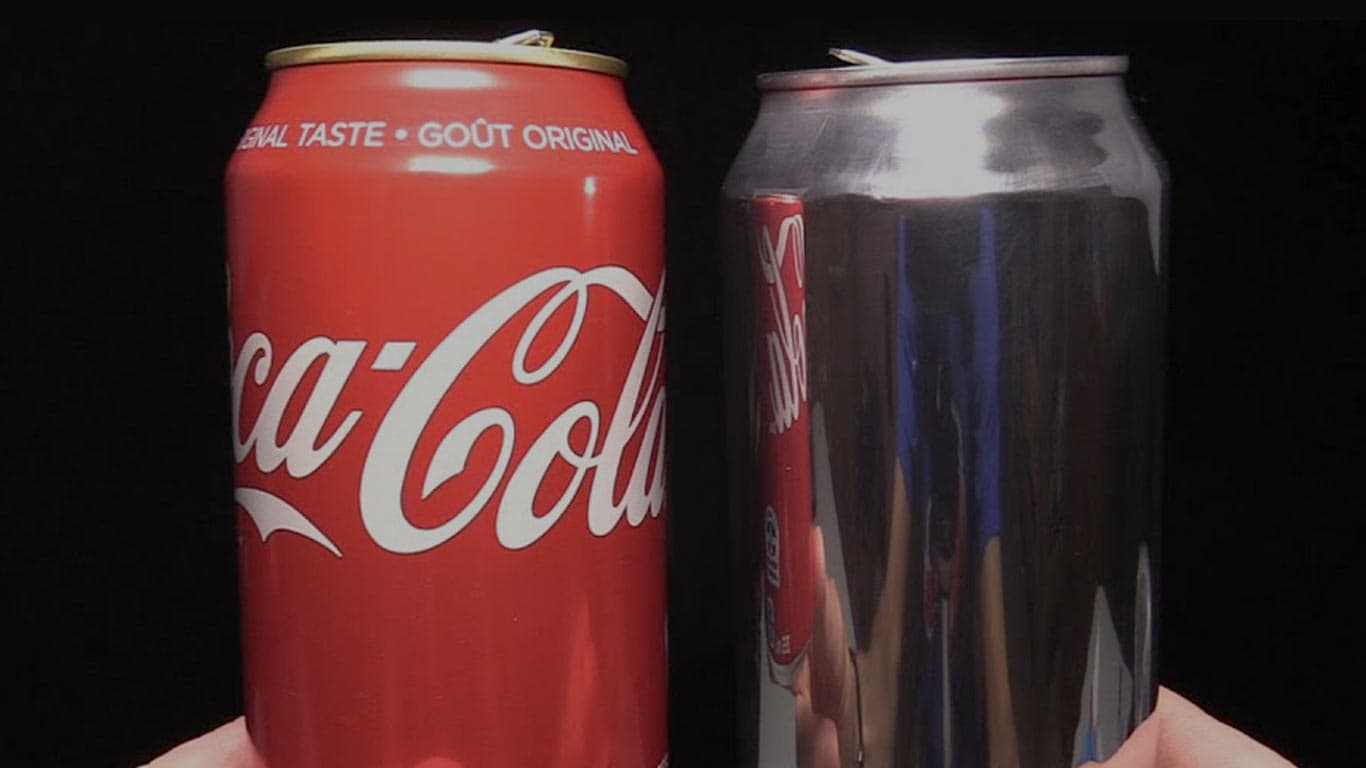
Laser paint removal in the Bay Area is a technician on the job. The day rate is $800/day on [services](/services). A Bay Area body shop stripping failed epoxy or polyurethane before recoat runs into a VOC cap near 50 grams per liter on solvent surface prep and spray-line cleanup, and older methylene-chloride paint strippers are barred from sale to industrial users after state toxics regulators listed the chemical as a priority product. A pulsed near-infrared laser removes the coating layer through thermal stress rather than solvent action, so shops can strip [aluminum](/materials/aluminum-laser-cleaning) panels and [steel](/materials/steel-laser-cleaning) frames without touching that VOC limit or generating stripped-paint waste. The exception is thick marine-grade epoxy built up over several coats, where repeated passes near rivets and seams can discolor the substrate unless the operator drops pulse energy and adds a cooling pause between rows. Shops already running [rust](/applications/laser-rust-removal-bay-area) or [lead paint](/applications/lead-paint-laser-removal-bay-area) removal on the same line can cover all three [paint coating](/contaminants/paint-coatings-laser-cleaning#substrateMatrix) jobs from one machine instead of separate chemical-stripping stations.
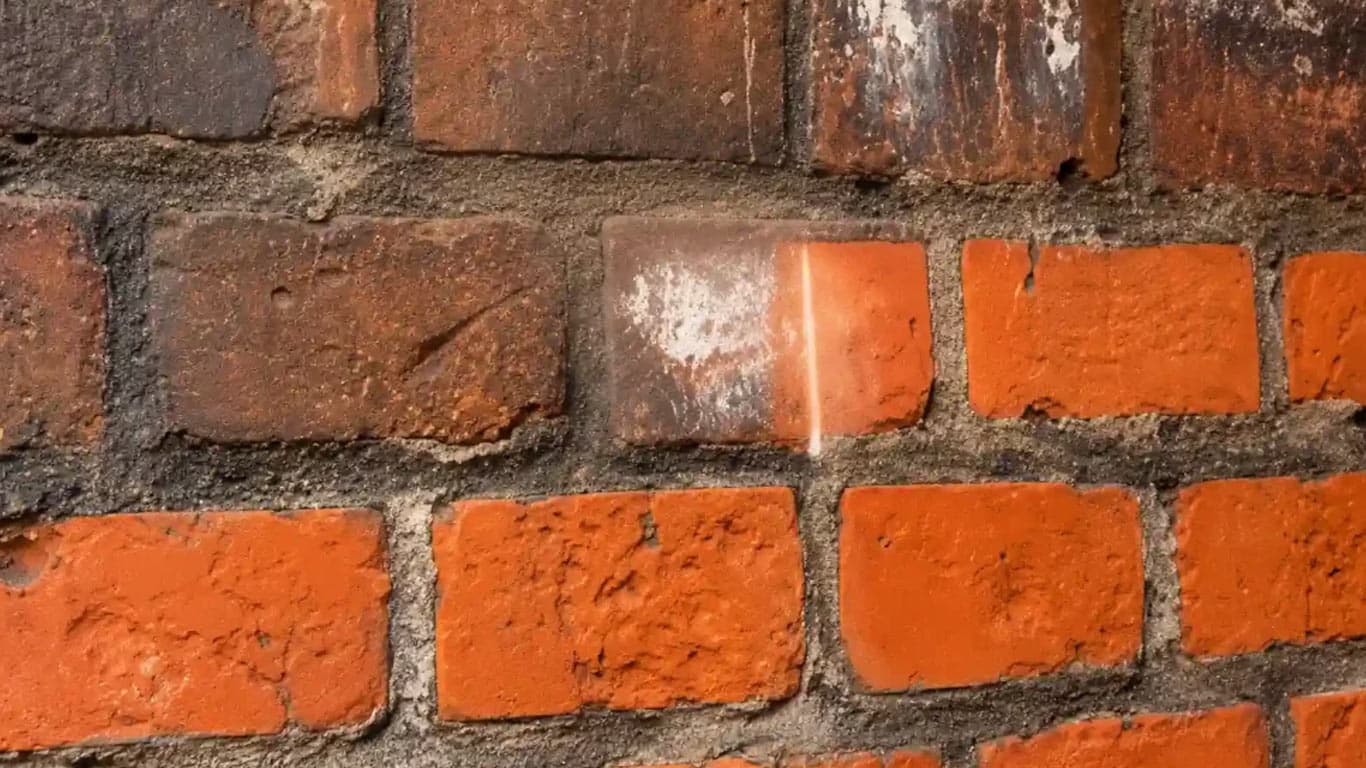
On a brick, limestone, or sandstone wall, this job removes centuries of soot, biological growth, and pollution crusts from [brick](/materials/brick-laser-cleaning), [limestone](/materials/limestone-laser-cleaning), and [sandstone](/materials/sandstone-laser-cleaning) facades without the abrasive media that etches carved detail or grinds away original tooling marks. A calibrated beam lifts surface deposits layer by layer, leaving the substrate's patina and fine ornamental relief intact where sandblasting or dry-ice methods would round edges or drive moisture into porous stone. The process will not repoint failed mortar, consolidate spalling stone, or reverse decades of weathering already beneath the crust; those repairs still need a mason. Conservators pair the cleaning with condition surveys before touching any protected facade, and the same equipment scales from single relief panels to full elevations on [heritage architectural work](/applications/heritage-architectural-laser-cleaning-applications) where soda-blasting alternatives risk salt contamination in soft masonry.
Architectural soda-lime jobs break when crews copy metal energy maps onto clear panes. They also break when dust capture is missing while glass particulate rises. Thin annealed stock checks when heat piles up from tight nanosecond overlap before the coupon map is frozen (Sage MST 2025 nanosecond laser review).

