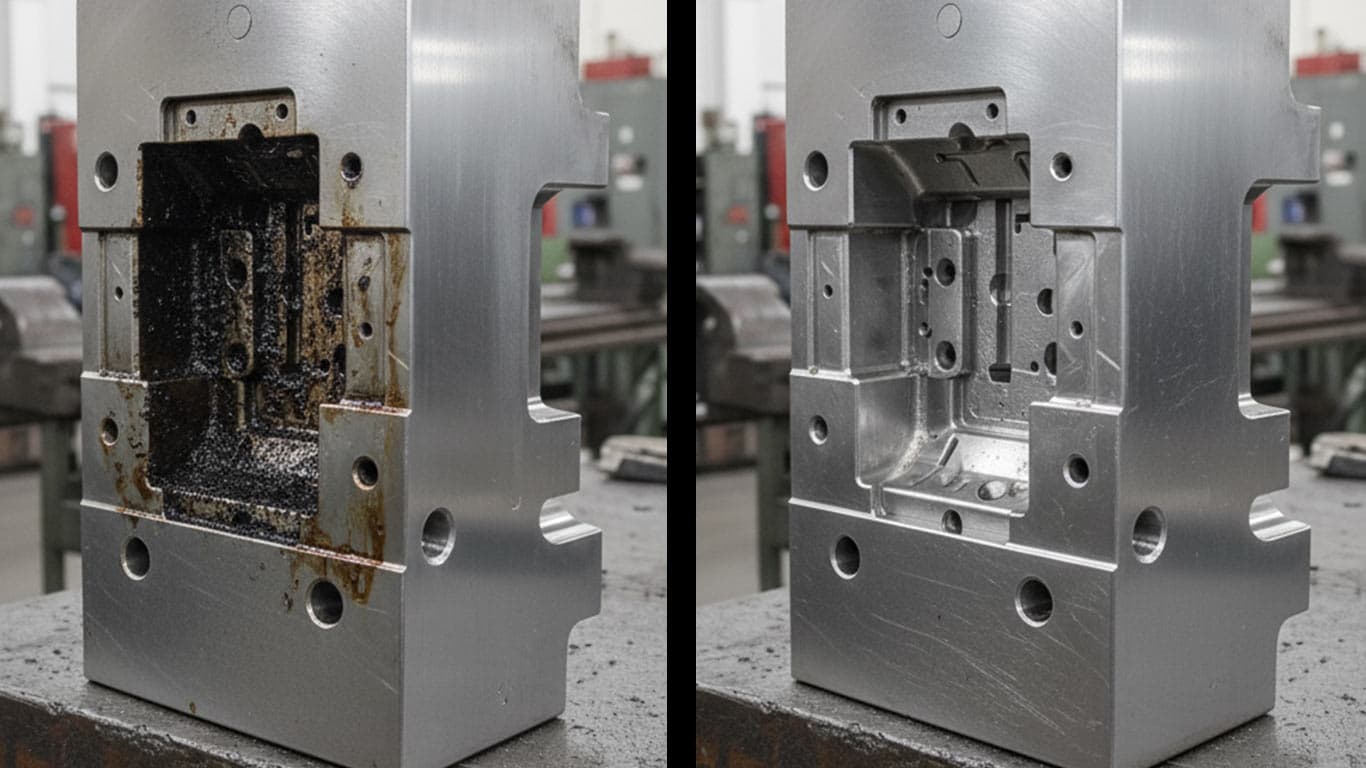
Tool Steel Laser Cleaning
Removing release film and oxide from tool steel works when a pulsed laser stays below the point that draws temper or marks the working face. Hot-work and cold-work grades do not sh...
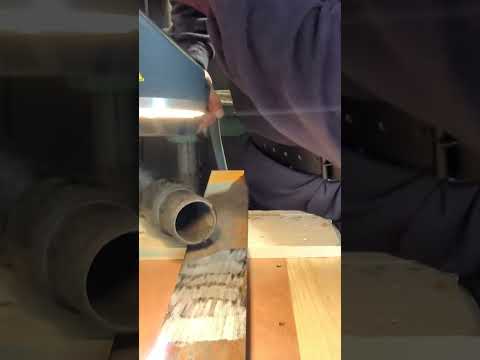
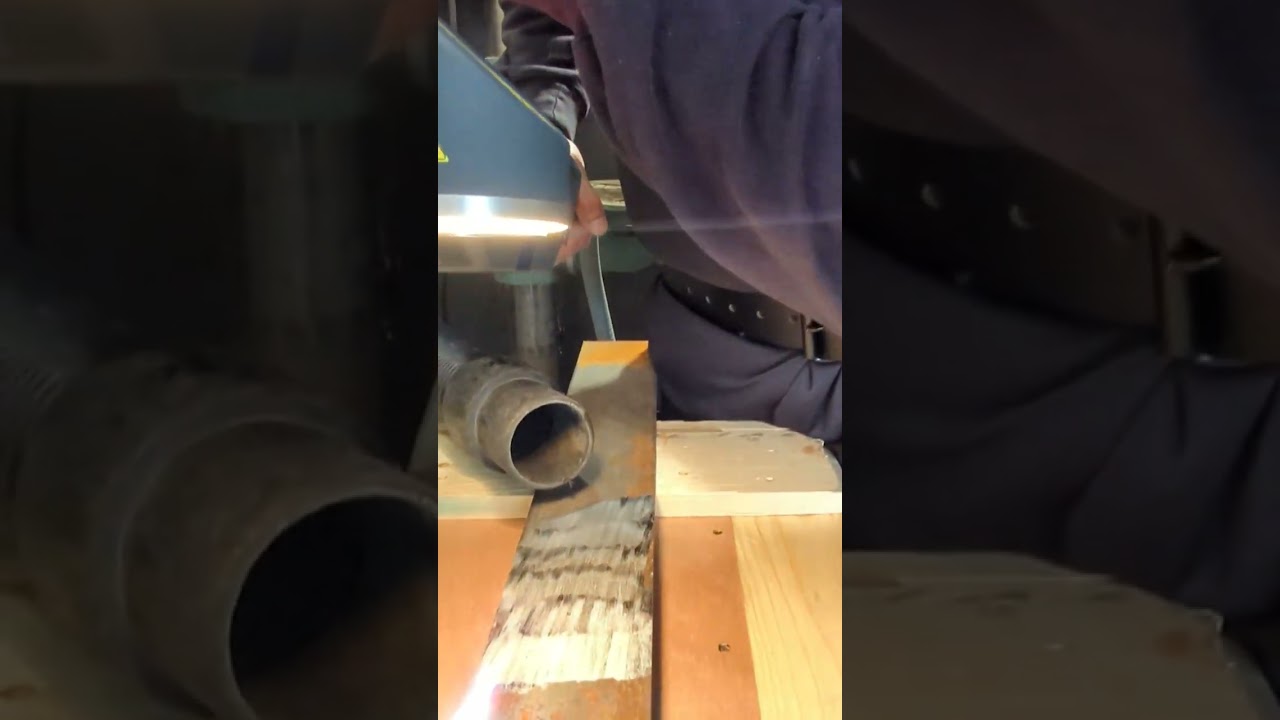
This 24-second clip keeps heavy rust on a cold-finished steel bar in frame and stops short of a finished-part inspection. The bar carries a thick oxide stack, not a thin surface stain, so a single pass will not leave a mill-bright finish in this short segment. Readers who want the chemistry behind that oxide layer can check the iron oxide rust overview and the general steel reference data alongside this footage. Shops weighing rust removal work in the Bay Area should treat the clip as a starting point rather than a full case study, since heavy rust on round bar stock behaves differently than rust on flat plate or weld-affected steel.
Short -qRJsbft4Yg shows pulsed laser clearing heavy rust from a cold steel bar in 24 seconds without grit.
Removing release film and oxide from tool steel works when a pulsed laser stays below the point that draws temper or marks the working face. Hot-work and cold-work grades do not sh...

Laser cleaning removes weld heat tint and surface oxide from 316 stainless using fluence between about 0.41 and 2.0 J/cm², with visible damage starting near 2.0 J/cm² on bare 316L....
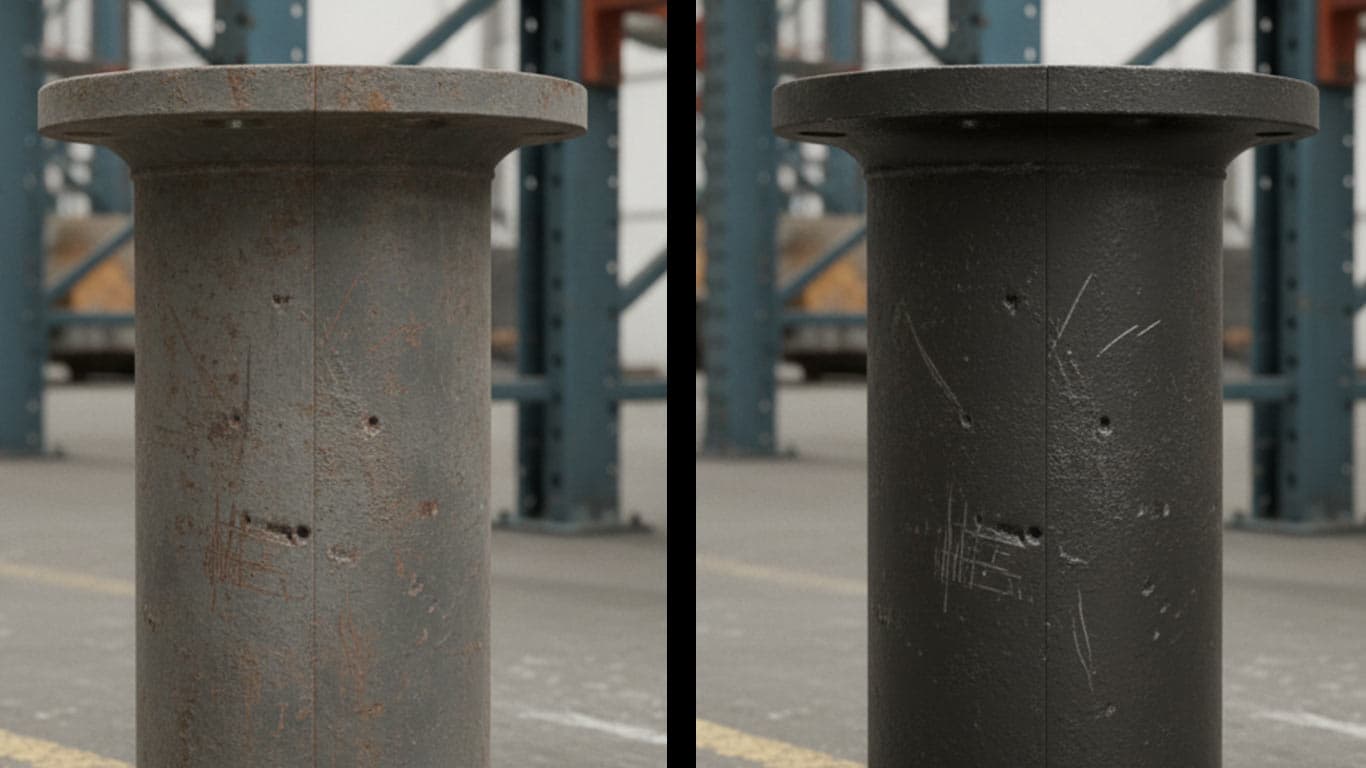
Gray and ductile cast iron keep graphite in the matrix. That graphite is supposed to stay there. Rust and foundry scale can come off with a dry laser pass when a copied steel setti...
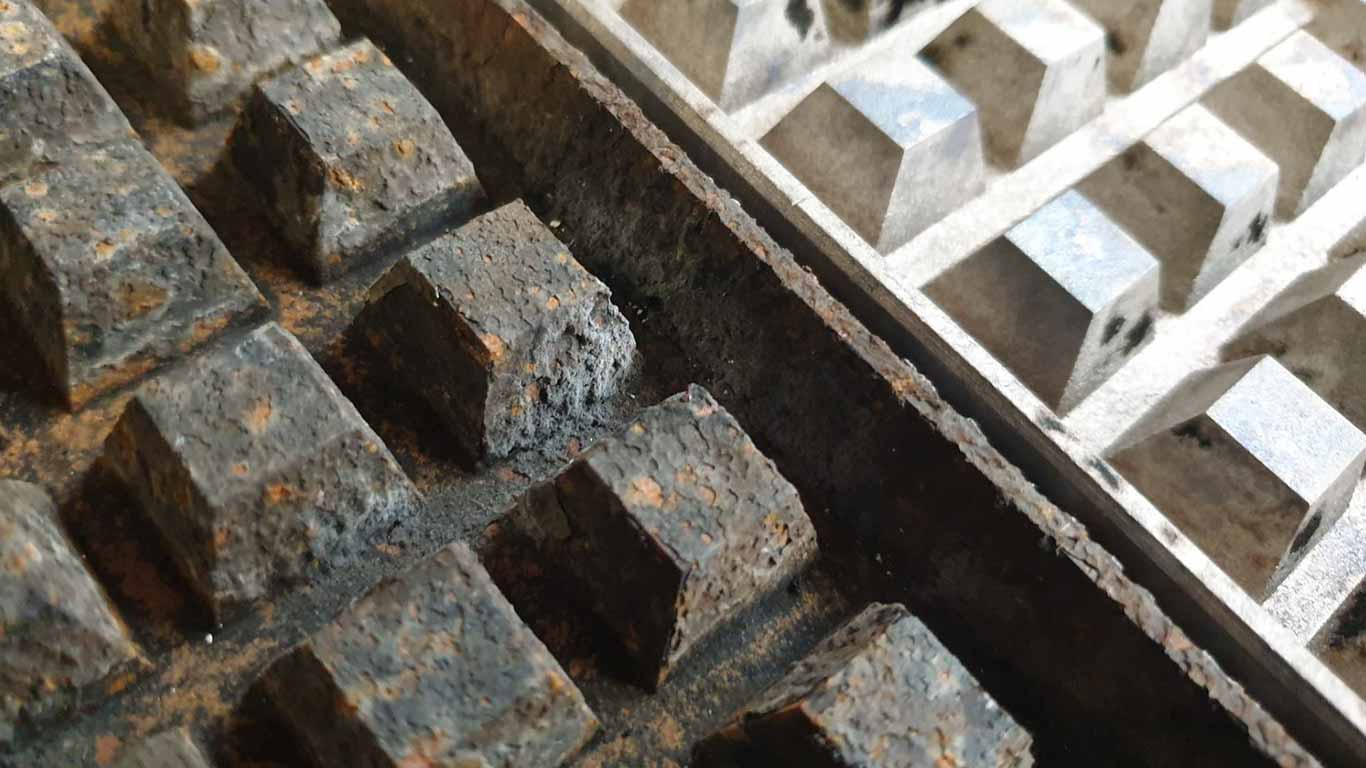
Laser cleaning removes rust, mill scale, and weld discoloration from steel without media, holding fluence near a 1.5 J/cm² cleaning floor and stopping short of the 4.5 J/cm² mark t...
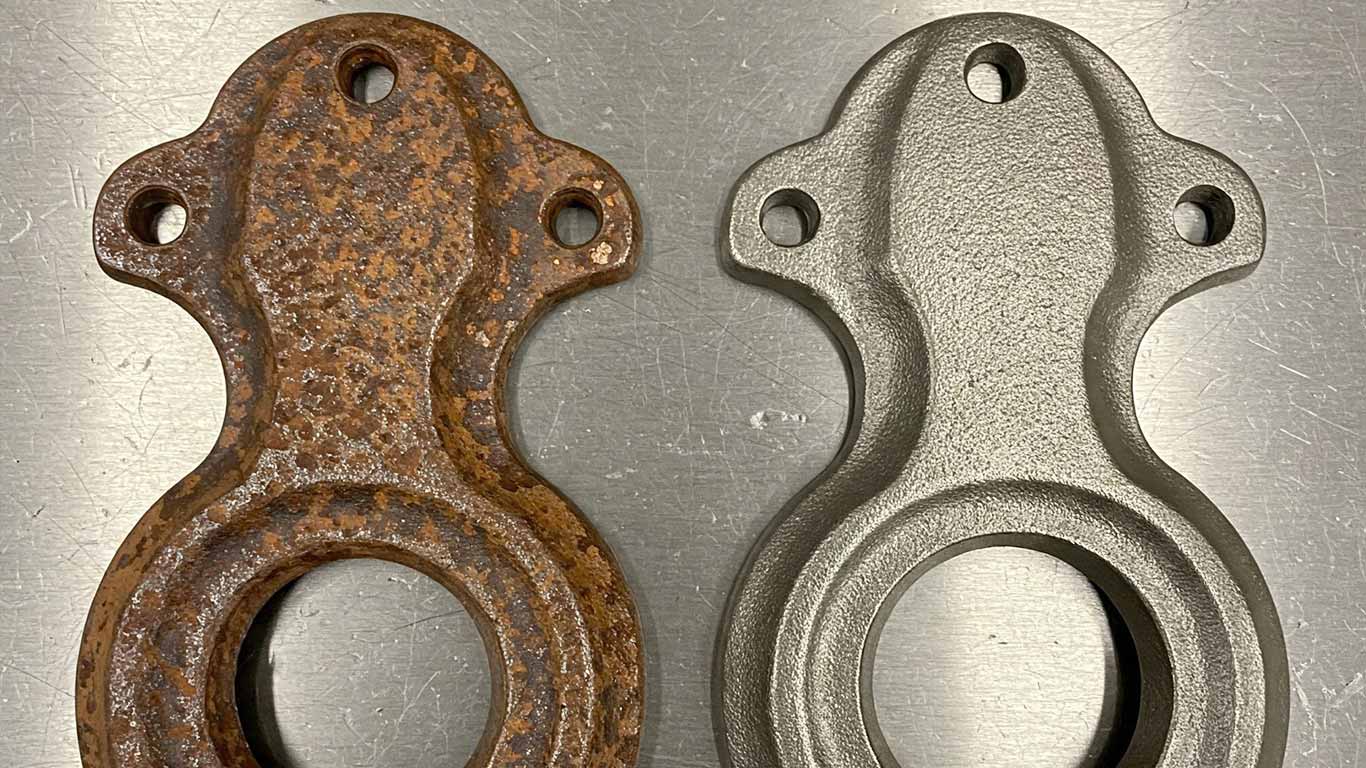
Rust and mill scale come off iron without abrasive blasting the face. Thickness and moisture in that rust change the job. Cast iron with graphite at the surface does not behave lik...

Laser cleaning removes rust, oxide, and residue from 304 stainless without damaging the base metal, using fluence between 0.41 and 2.0 J/cm² while staying below the damage limit at...
Laser cleaning removes iron oxide rust from steel down to bare metal without grinding wheels, abrasive blasting, or chemical strippers. The beam ablates the oxide layer while leaving sound steel underneath intact, so a part keeps its original dimension and surface finish through cleaning. It will not reverse pitting the rust already caused, repair corrosion damage done to the substrate, or clear a part in one blanket setting; rust depth and iron oxide type both change how many passes the surface needs before it is ready for inspection.
Requires matching the paint system and substrate pairing before setting energy, because a thin single topcoat on [steel](/materials/steel-laser-cleaning) clears at a fraction of the fluence a multilayer primer stack on [aluminum](/materials/aluminum-laser-cleaning) needs, and the substrate sets its own ceiling once the coating is gone. Paint sits as an applied, cross-linked polymer film bonded by mechanical keying and resin adhesion, not a corrosion product, so pigment load and binder chemistry decide more of the setting than the substrate alone. A surface-integrity study on laser-cleaned aluminum alloy carrying a paint layer documents that a visually bare finish does not by itself confirm the metal underneath escaped the pass undamaged (Applied Optics, 2024).
Laser cleaning fractures the bluish-black magnetite laminate off carbon steel in repeated passes, because mill scale runs roughly four times harder than the plate underneath it. A hot-rolled plate carrying this scale typically needs four or more passes to reach bare metal, while a lighter rust bloom on the same yard stock can clear in one or two. It will not strip in a single rust-grade pass, will not raise the surface to a deep abrasive-blast anchor profile some coating specs still call for, and will not reverse pitting that was already hiding under the scale.
Laser cleaning decomposes mineral oil, synthetic lubricant, and machine grease off steel, aluminum, and stainless steel through fast thermal breakdown of the hydrocarbon film, the same damage-threshold logic that broader laser-cleaning threshold research has documented across very different host materials (Journal of Cultural Heritage, 2000). It is not a substitute for a wet alkaline line degreasing a full rack of parts at once, and it will not clear a bonded hard coating or a thick paint stack sitting on top of the oil.
Requires a material call before a setting, since carbon-filled EPDM and nitrile gasket residue absorb a 1064 nanometer beam efficiently while Viton and other FKM compounds carry the same dark filler but decompose above roughly 200°C into hydrogen fluoride gas. [Carbon steel](/materials/steel-laser-cleaning) flange faces clear this residue between about 1 and 3 J/cm2, well under the 8 to 15 J/cm2 point where the metal itself starts to take damage, so the margin stays wide once the gasket type is confirmed on a coupon. Peer-reviewed laser surface-prep work on bonding faces shows the same selective-lift pattern a flange land needs when the rubber film must leave and the metal underneath must stay ready for the next gasket.
Laser cleaning removes the chromium-oxide and titanium-oxide scale that post-weld and post-anneal heat treatment grows on stainless steel, titanium, and Inconel, clearing the film without a chemical pickling bath. It will not rebuild the chromium that heat already pulled out of the grain boundaries beneath a dark heat-treated color, will not fix titanium alpha case that has already let oxygen diffuse deep into the metal, and will not stop the bare surface from re-oxidizing once it goes back into service heat.

Laser cleaning removes mill scale, oxide layers, and weld residue from fabricated metal parts without abrasive media or chemical strippers. Shops handling [steel](/materials/steel-...

Automotive and EV production lines use pulsed fiber lasers to strip mill scale from stamped [steel](/materials/steel-laser-cleaning) body panels, clear weld-seam oxide ahead of res...
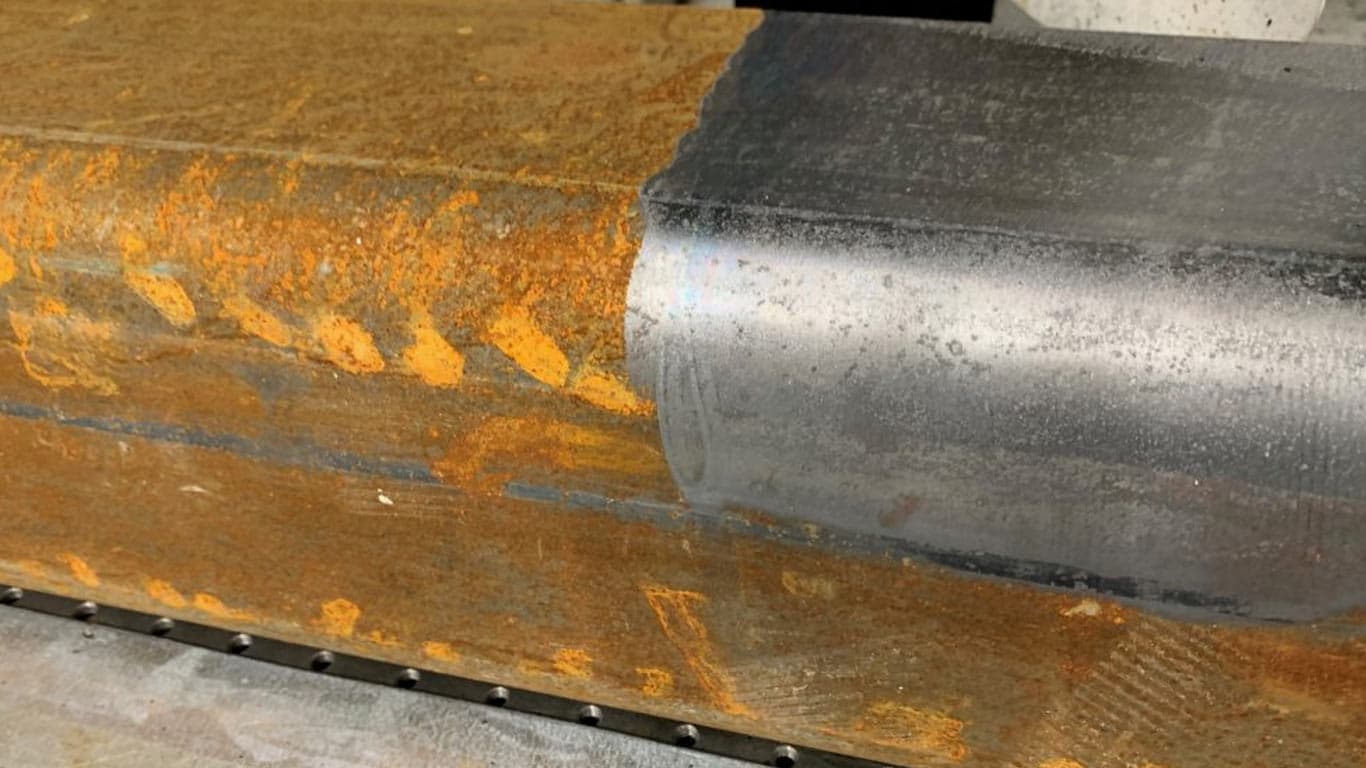
Laser rust removal in the Bay Area is a technician on the job. The day rate is $800/day on [services](/services). Laser cleaning removes field [rust](/contaminants/iron-oxide-rust-...
Laser cleaning removes the blue-brown heat tint that forms along a weld seam on [stainless steel](/materials/stainless-steel-laser-cleaning) during [weld prep](/applications/weld-p...
Weld preparation laser cleaning removes rust, mill scale, oil, and drawing compound from a joint face right before the arc or beam strikes, so the fitter is not grinding or wire-br...

Laser cleaning removes rust, cured rubber buildup, and adhesive film from conveyor belt rollers without solvents or abrasive media that can pit bearings and seals. The process stri...