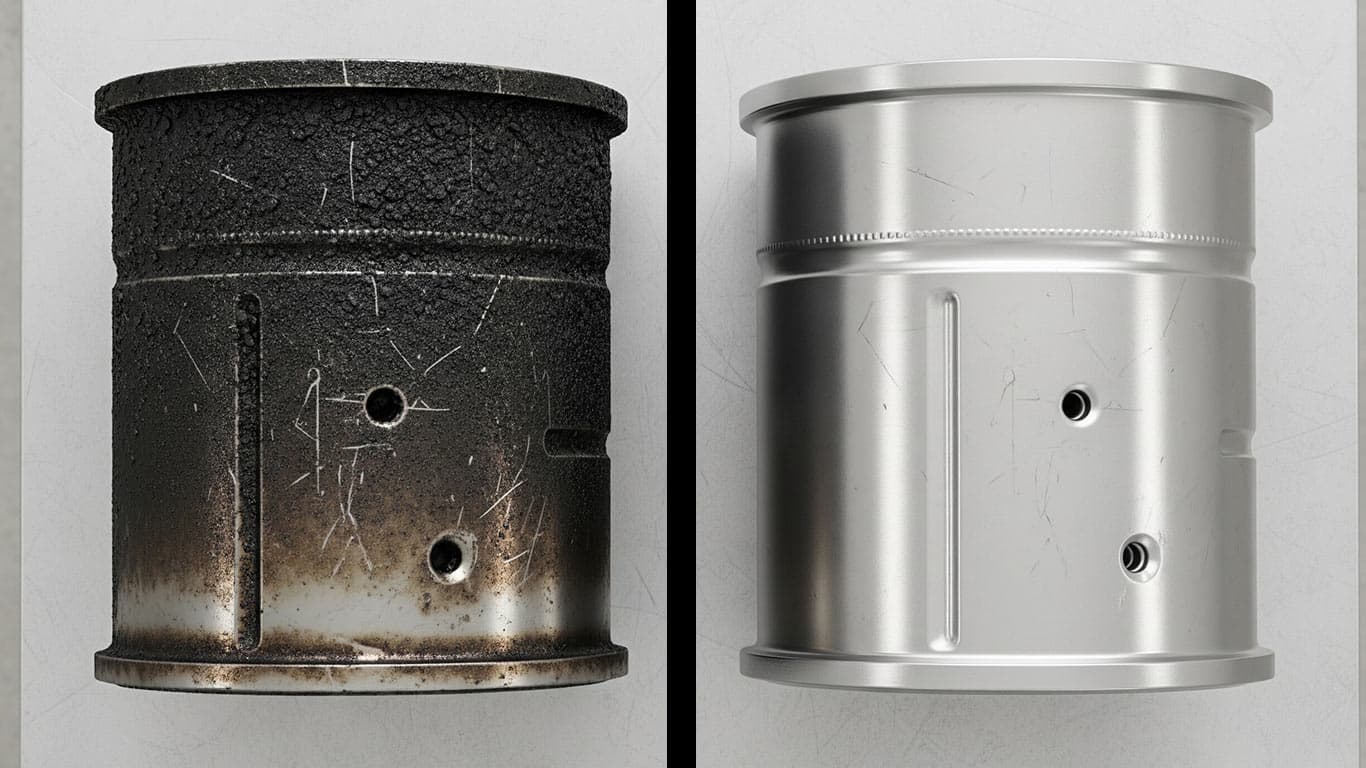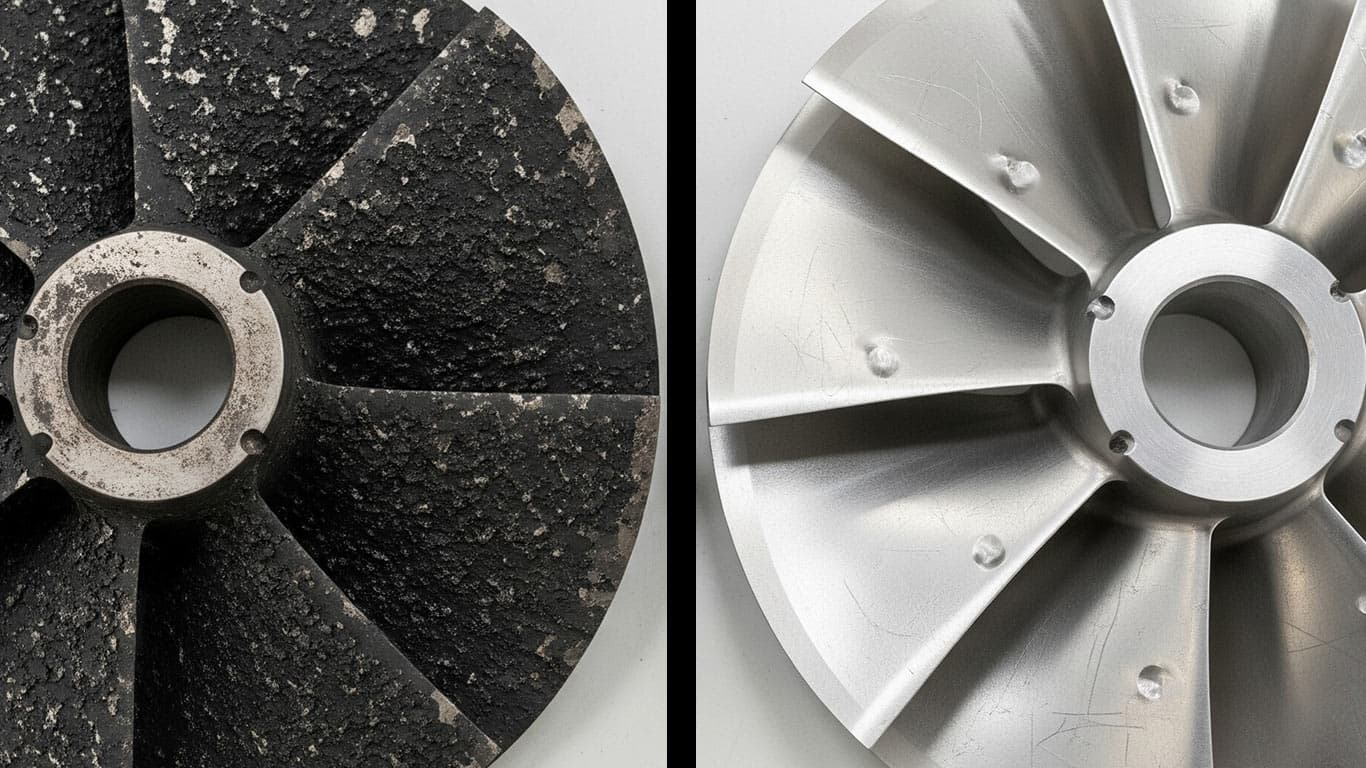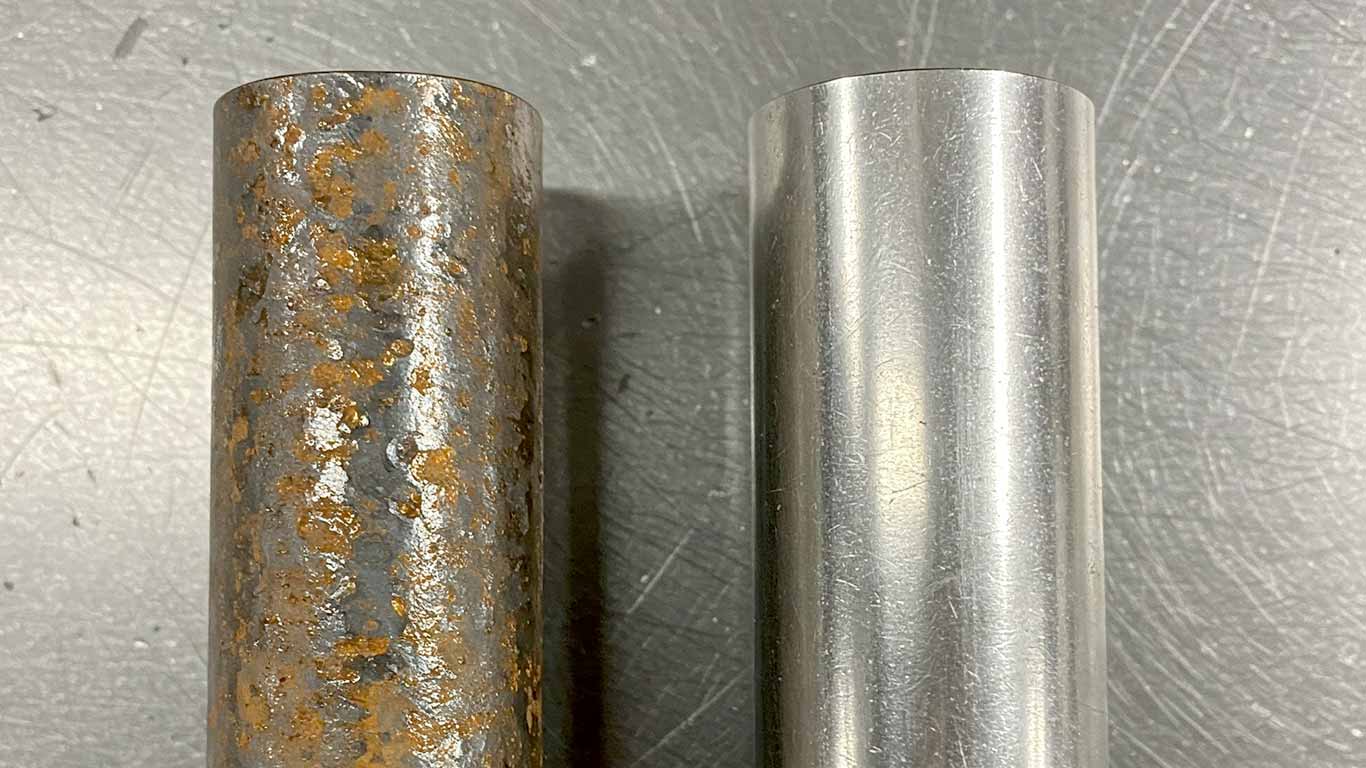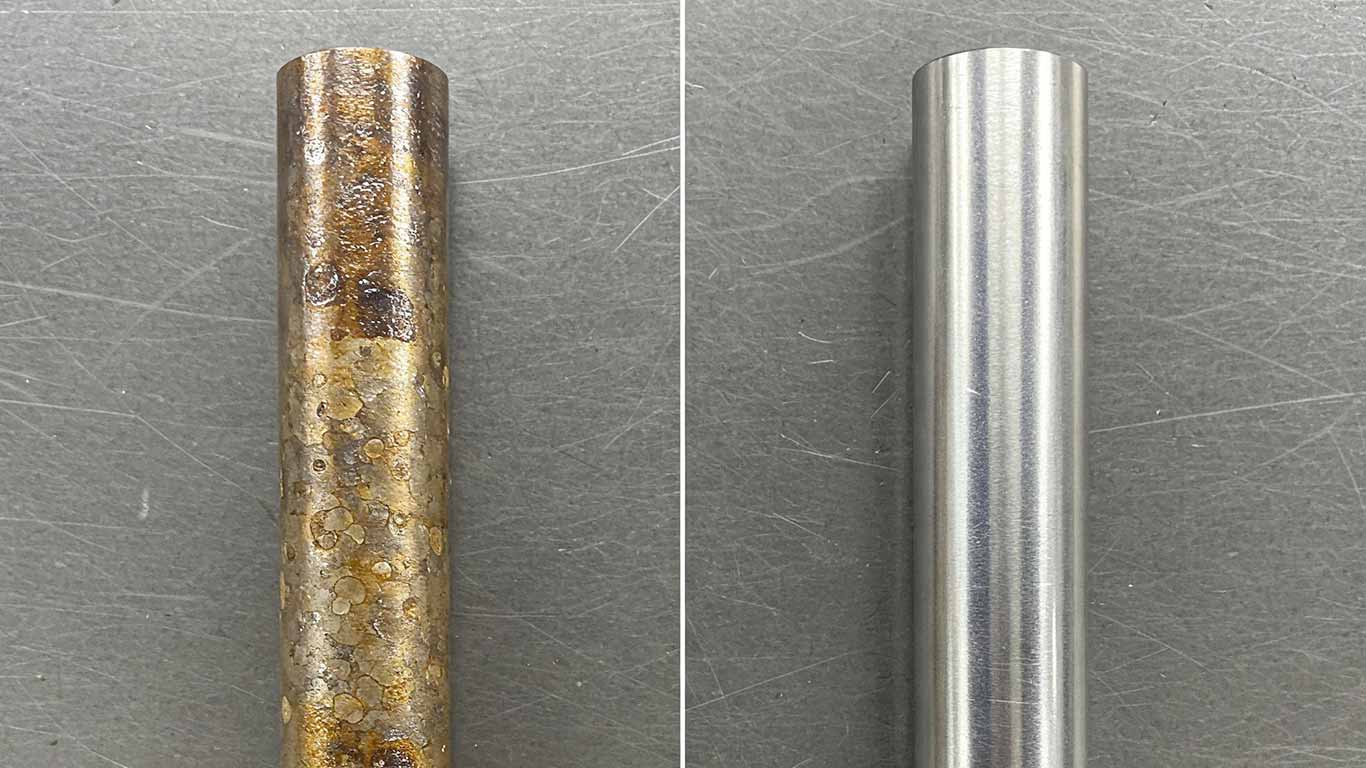
Metal Laser Cleaning Materials

Technical parameters and best practices for laser cleaning ferrous, non-ferrous, and alloy metals, including stainless steel, aluminum, and titanium.

Alloy

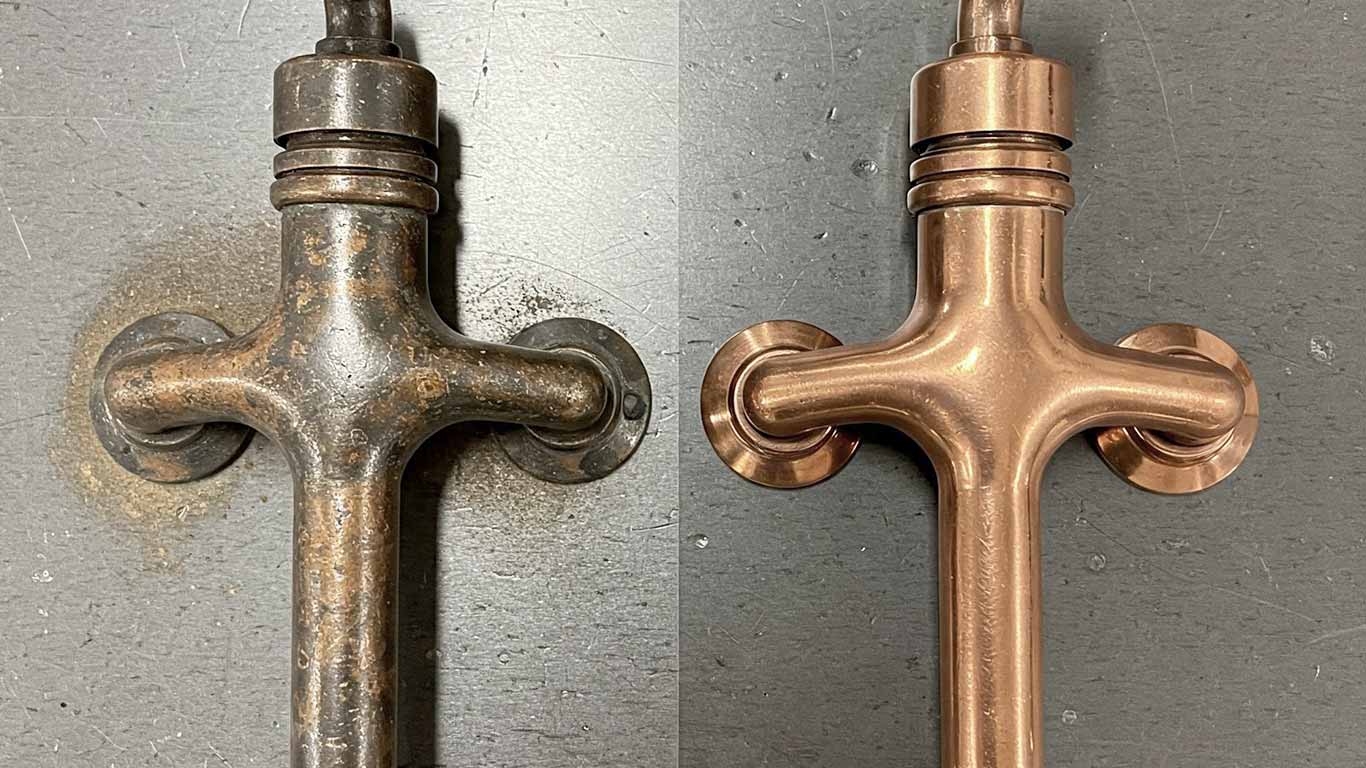
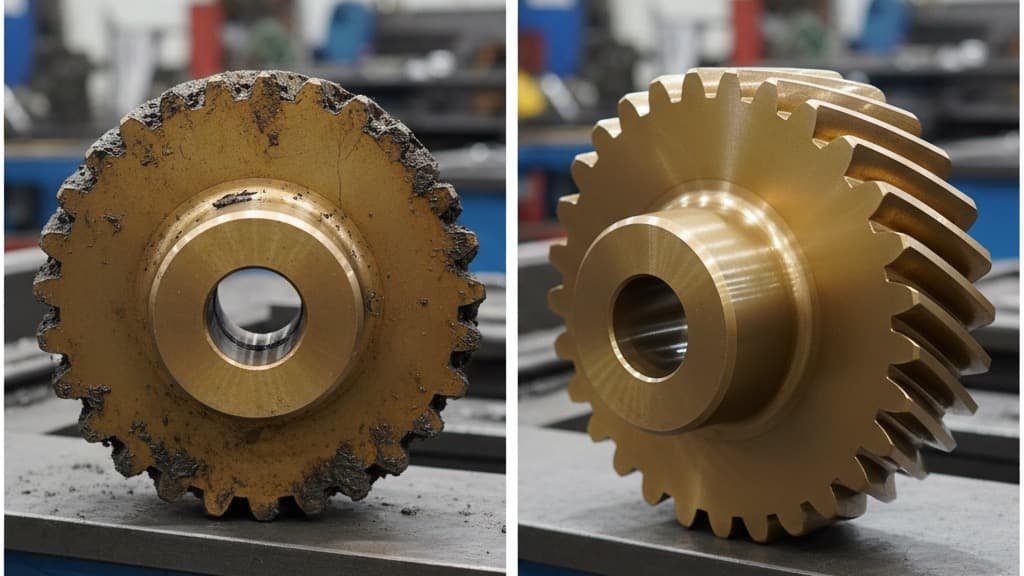
Aluminum Bronze surface prepared by laser cleaning

Aluminum Bronze

View details: Aluminum Bronze. Category: metal. Subcategory: Alloy.

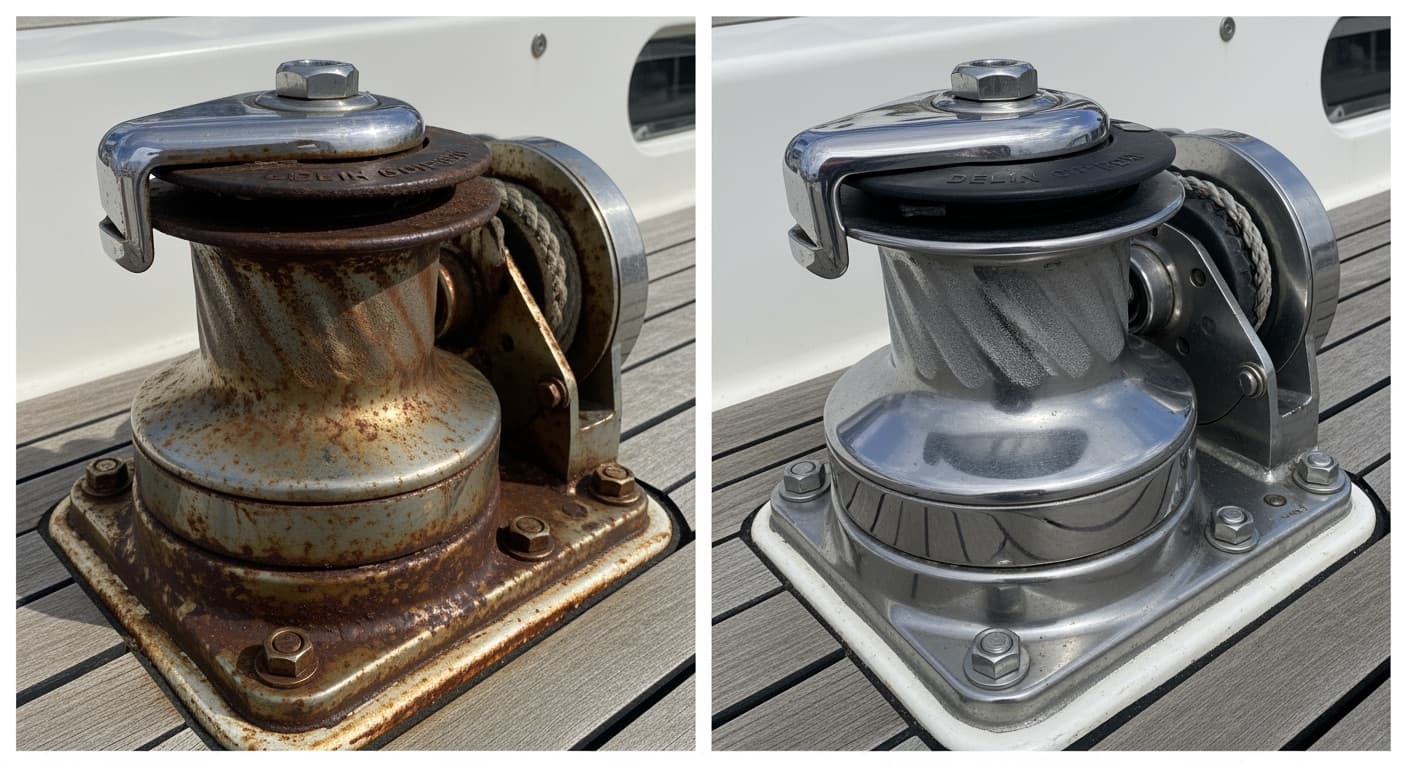
Marine hardware and pumps in aluminum bronze are a copper-aluminum alloy, not a tin bronze and not a structural aluminum. A dry laser pass can take off biofouling and handling soil when the grade is confirmed and copper-bearing dust is captured at the head. The thin oxide film that helps the alloy resist seawater should stay on the metal. Strip that film and the face is brighter and less protected. Trials on the actual casting come before any production schedule.
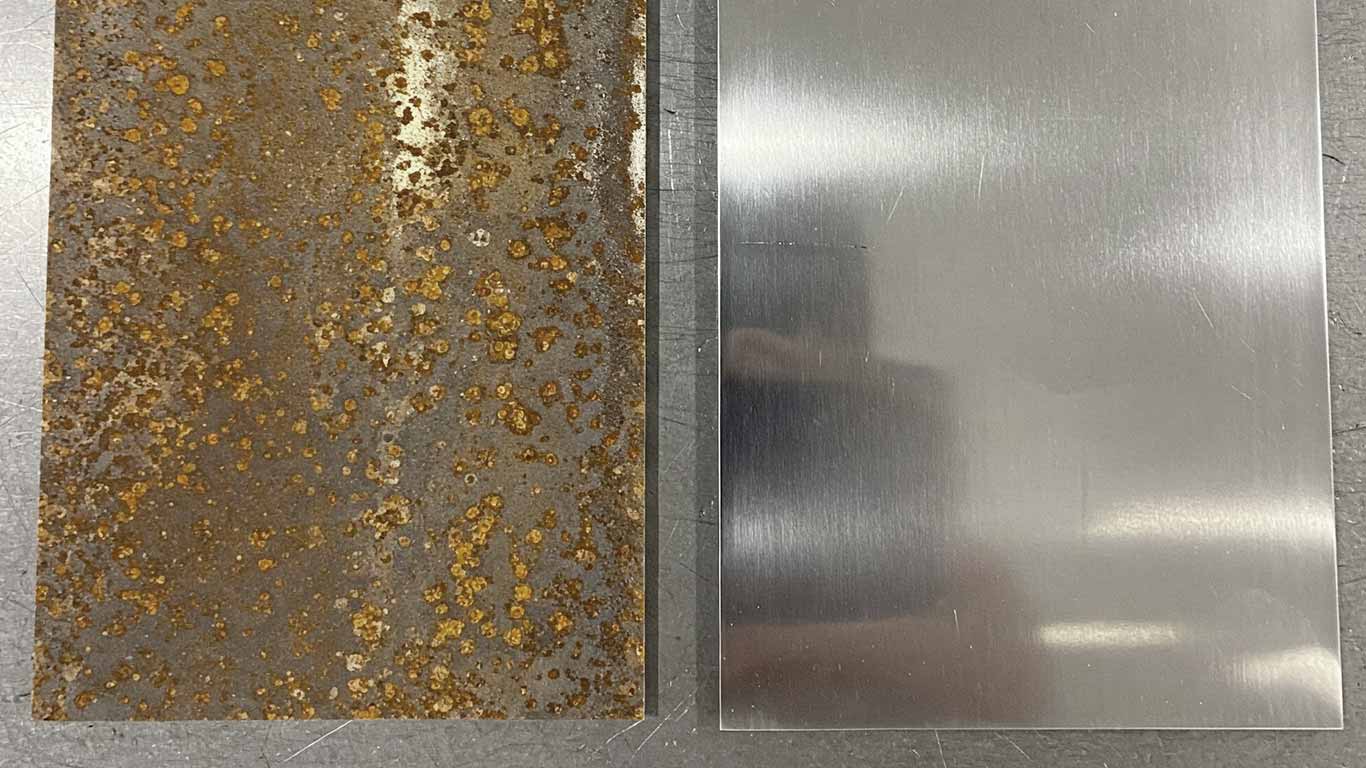
Stainless Steel surface prepared by laser cleaning

Stainless Steel

View details: Stainless Steel. Category: metal. Subcategory: Alloy.

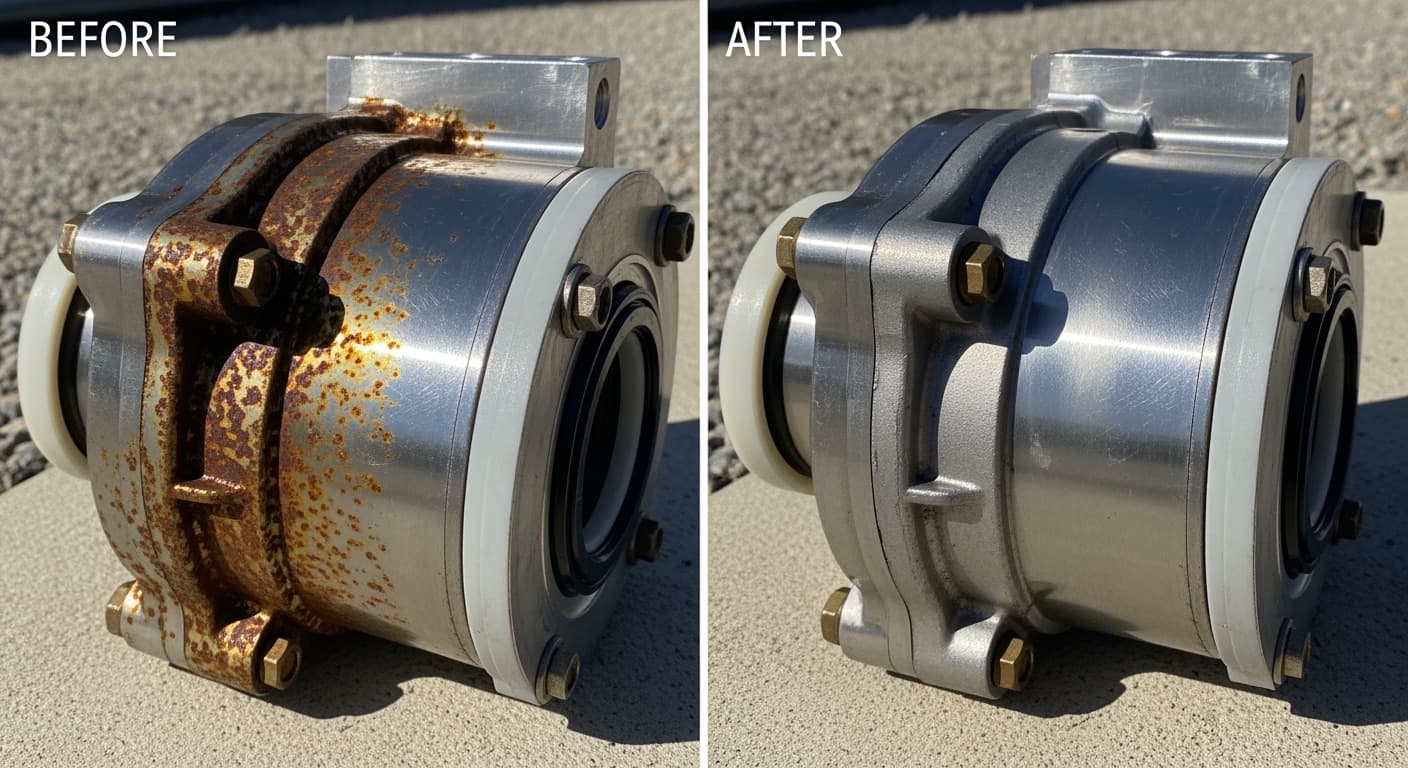
Stainless steel begins to ablate surface films near 0.41 J/cm² at 1064 nm, and that onset is far below where the base metal itself takes damage. The damage threshold runs 5 to 12 J/cm², so the wide margin between those two numbers hides a lot of room for a setting that looks clean but is still wrong for the job. A fabricator cleaning 304L before welding can hit a fluence inside that margin that looks clean to the eye while still stripping chromium from the surface layer, leaving a passive film that forms slower and corrodes sooner than an undamaged one. This page covers the shared ablation and thermal behavior across the austenitic, ferritic, and duplex families, and routes grade-specific parameters to [304 stainless](/materials/stainless-steel-304-laser-cleaning) and [316 stainless](/materials/stainless-steel-316-laser-cleaning), since those two see the most pre-weld and marine-service cleaning. It does not set one fluence for the whole family; molybdenum content, surface finish, and the operation (passivation, weld prep, or scale removal) each shift where that safe range sits. Readers doing weld prep should also check the [weld passivation](/applications/stainless-steel-weld-passivation-laser-cleaning) page for the chromium-depletion risk in more depth.

Stainless Steel 304 surface prepared by laser cleaning

Stainless Steel 304

View details: Stainless Steel 304. Category: metal. Subcategory: Alloy.

Laser cleaning removes rust, oxide, and residue from 304 stainless without damaging the base metal, using fluence between 0.41 and 2.0 J/cm² while staying below the damage limit at 1064 nm. That damage limit runs 5 to 12 J/cm², and 304 won't match 316's resistance to saltwater, since it fits everyday tanks and sinks instead of marine exposure.

Stainless Steel 316 surface prepared by laser cleaning

Stainless Steel 316

View details: Stainless Steel 316. Category: metal. Subcategory: Alloy.

Bay Area [stainless steel](/materials/stainless-steel-laser-cleaning) 316 work requires its own acceptance path rather than a bid as AMPP laser prep, because inside-diameter [weld heat tint](/contaminants/weld-heat-tint-laser-cleaning) fails color inspection after the bead already passed a visual check, and a spec borrowed from [304](/materials/stainless-steel-304-laser-cleaning) does not cover that bore.

Tin surface prepared by laser cleaning

Tin

View details: Tin. Category: metal. Subcategory: Alloy.

Taking oxide and light films off tin with a pulsed laser works when energy stays inside a gentle range for soft alloys, because this metal melts at a low temperature. Grade and plating thickness decide the map, including tin on [copper](/materials/copper-laser-cleaning). Inorganic tin dust needs capture for the whole dry pass. Melt beads or new roughness mean the pass has gone too far.

Titanium Alloy Ti 6Al 4V surface prepared by laser cleaning

Titanium Alloy (Ti-6Al-4V)

View details: Titanium Alloy (Ti-6Al-4V). Category: metal. Subcategory: Alloy.

Ti-6Al-4V is the common aerospace and implant titanium alloy. A pulsed laser can take oxide and heat tint off Grade 5 stock when energy stays high enough to work the film and low enough not to mark the alloy. Heat stays near the surface because this alloy conducts heat poorly, so coupon proof matters more than a copied commercially-pure titanium setting. Titanium dust capture belongs on. The thin native oxide will reform after the pass.

Tool Steel surface prepared by laser cleaning

Tool Steel

View details: Tool Steel. Category: metal. Subcategory: Alloy.

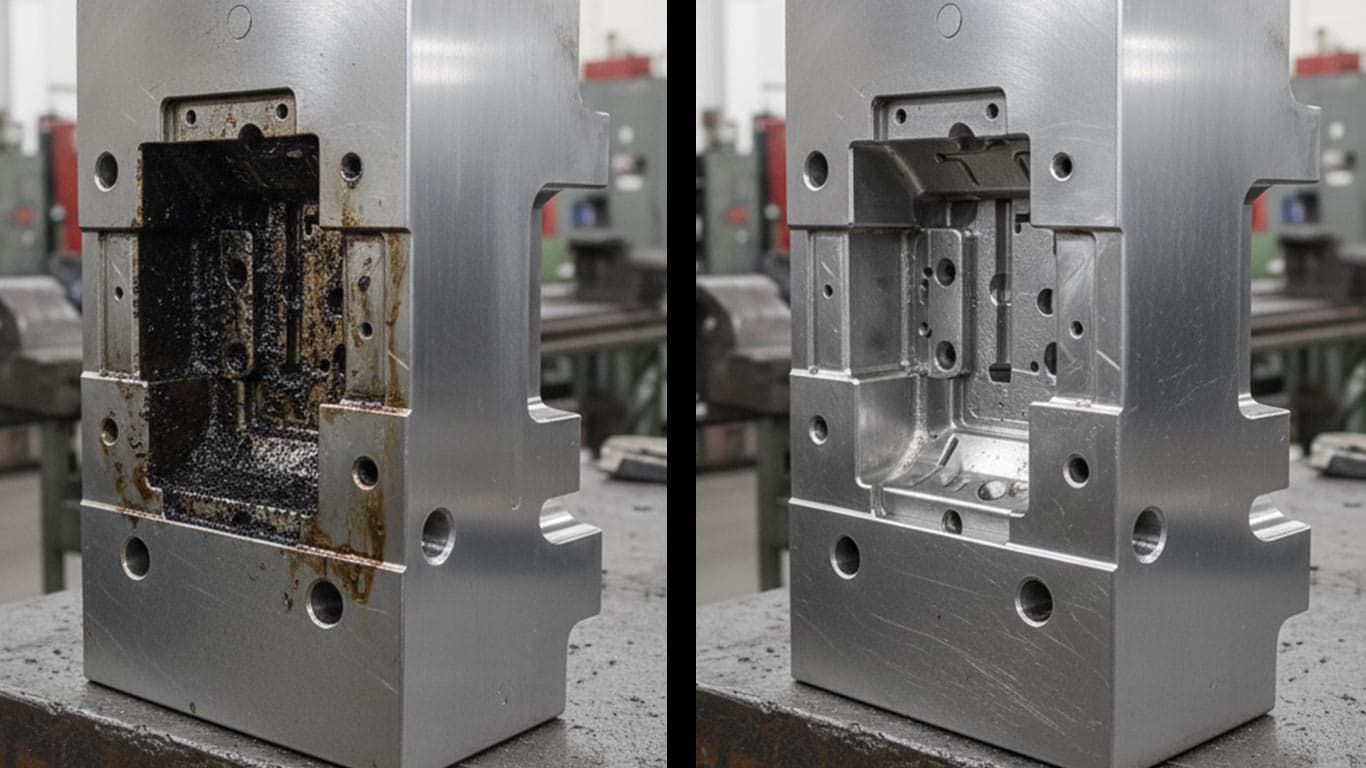
Removing release film and oxide from tool steel works when a pulsed laser stays below the point that draws temper or marks the working face. Hot-work and cold-work grades do not share the same heat limit, so the die steel itself decides the map. Hard PVD skins need their own pass plan. Alloy dust capture stays on for the whole dry job.

Zinc surface prepared by laser cleaning

Zinc

View details: Zinc. Category: metal. Subcategory: Alloy.

Zinc shows up as die-cast parts, rolled sheet, and galvanized coatings. A pulsed laser can take native oxide and white rust off the face when energy stays inside a gentle range for soft alloys and the job is scoped so the beam does not open bare steel under a coating. The zinc form decides the map. Zinc oxide fume needs capture at the head before weld prep or paint follows.

Non Ferrous

Aluminum surface prepared by laser cleaning

Aluminum

View details: Aluminum. Category: metal. Subcategory: Non-Ferrous.

A nanosecond fiber laser removes aluminum oxide film starting at 0.33 J/cm2 fluence, with the full removal range extending through 1.09 J/cm2. Within that band the mechanism shifts from spallation to sublimation, so the correct setting depends on alloy and film thickness rather than one fixed number. The same physics shows up in [weld prep](/applications/weld-prep-laser-cleaning-applications), on [anodized aluminum](/contaminants/anodized-aluminum-laser-cleaning), and in [suspension-arm cleaning](/videos/porsche-911-upper-suspension-arm-laser-cleaned-bGLki9u3). Aluminum's high thermal conductivity and low melting point near 660 C narrow the margin between stripping the oxide and marking the base metal, and ANSI Z136 beam safety practices apply at every fluence in that range.

Brass surface prepared by laser cleaning

Brass

View details: Brass. Category: metal. Subcategory: Non-Ferrous.

Brass hardware and fixtures can shed tarnish and old lacquer with a dry laser pass when energy stays on the soil and zinc is not driven out of the surface. Acid dips are the usual shop alternative. The laser job still needs a trial because the alloy couples unevenly. A hot pass can leave a pink zinc-poor face. Copper-bearing dust capture stays on for the dry job.

Bronze surface prepared by laser cleaning

Bronze

View details: Bronze. Category: metal. Subcategory: Non-Ferrous.

Outdoor sculpture and marine hardware in bronze can lose corrosion and later coatings with a dry laser pass when the grade is known and copper-bearing dust is captured at the head. Surface color often matters as much as cleanliness. Patina may be the finish the owner wants to keep. A hidden-face trial decides what leaves and what stays. A hot pass that strips that layer leaves a bright less stable face.

Copper surface prepared by laser cleaning

Copper

View details: Copper. Category: metal. Subcategory: Non-Ferrous.

A copper alloy laser cleaner needs the alloy class confirmed first, because the working window sits near 0.3–1.5 J/cm² on one class and 1.5–4 J/cm² on another, and [brass](/materials/brass-laser-cleaning) shows heat tint or an uneven film quickly when the wrong band is used. A [copper patina](/contaminants/copper-patina-laser-cleaning) adds a second risk: the noble cuprite layer can melt before the reactive crust clears, so heritage pieces call for Raman or cross-section review of the layers before energy rises. Production work such as [EV busbars](/applications/ev-battery-busbar-laser-cleaning) shifts the goal to a bare, conductive surface, which keeps the pass count and the oxide margin tied to the alloy you confirmed at the start.

Ferrous

Cast Iron surface prepared by laser cleaning

Cast Iron

View details: Cast Iron. Category: metal. Subcategory: Ferrous.

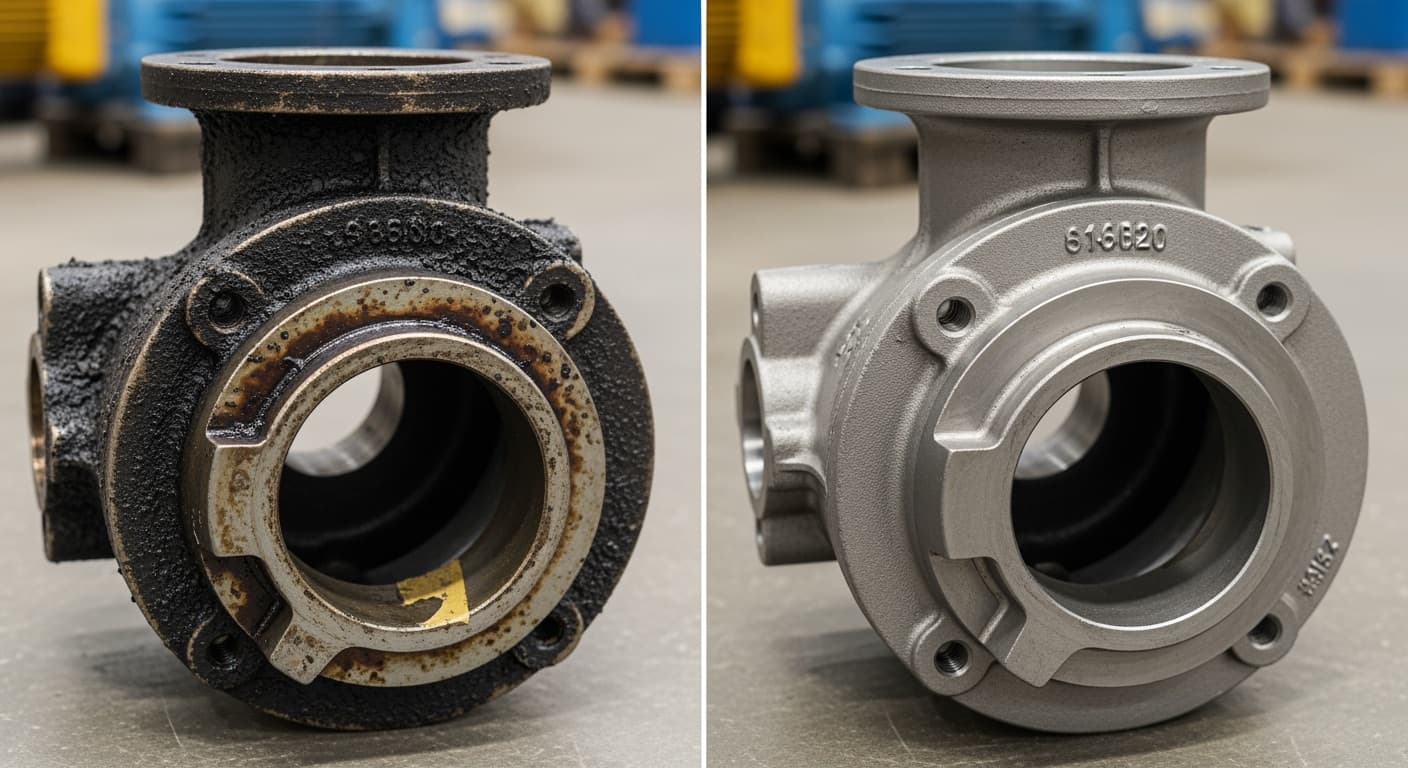
Gray and ductile cast iron keep graphite in the matrix. That graphite is supposed to stay there. Rust and foundry scale can come off with a dry laser pass when a copied steel setting is not used on a thin section or a porous face. Overheated porosity rusts faster once the job is done. Grade, a trial piece, and dust capture come before production on columns, brake parts, and fittings. Scrap of the same casting sets working energy because the usable range is tighter than on most other ferrous stock.

Iron surface prepared by laser cleaning

Iron

View details: Iron. Category: metal. Subcategory: Ferrous.

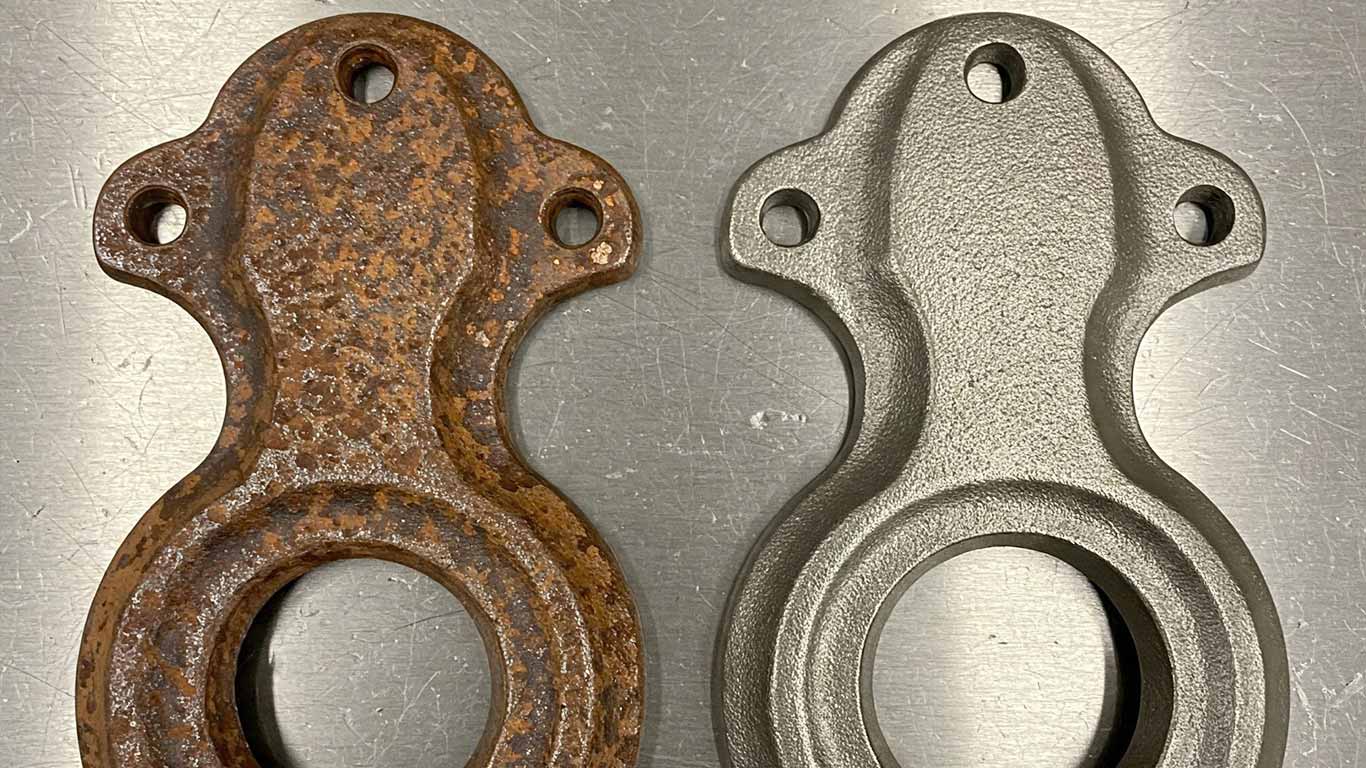
Rust and mill scale come off iron without abrasive blasting the face. Thickness and moisture in that rust change the job. Cast iron with graphite at the surface does not behave like wrought stock. A freshly cleaned face flash-rusts in damp air. Energy high enough to hurt the metal will melt peaks or leave a recast skin. Useful work removes the oxide and stops before the iron itself is cut. The next coat or oil has to go on before new rust starts.

Steel surface prepared by laser cleaning

Steel

View details: Steel. Category: metal. Subcategory: Ferrous.

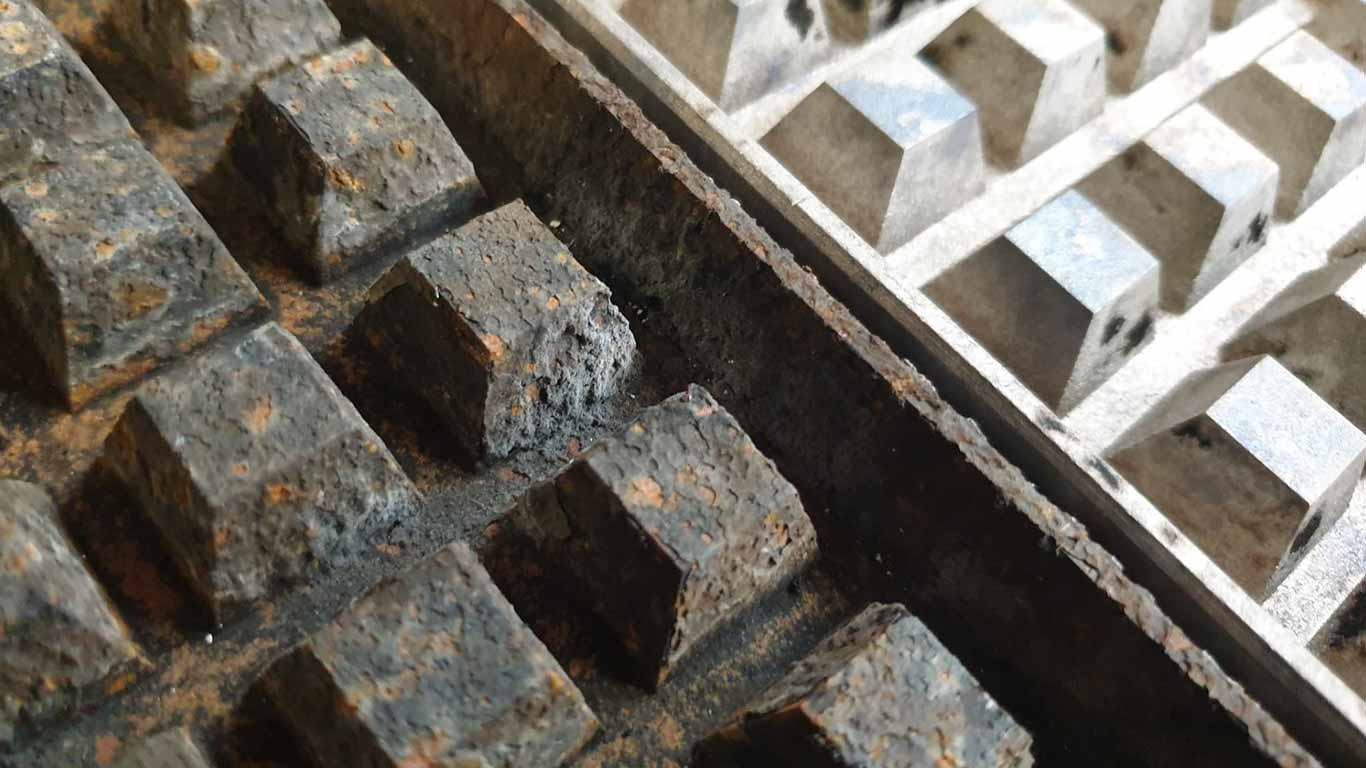
Laser cleaning removes rust, mill scale, and weld discoloration from steel without media, holding fluence near a 1.5 J/cm² cleaning floor and stopping short of the 4.5 J/cm² mark that scars bare metal. Intact mill scale still needs mechanical pre-treatment under AMPP SP21511-1 first. Compare with [stainless steel](/materials/stainless-steel-laser-cleaning) or [cast iron](/materials/cast-iron-laser-cleaning) laser cleaning when the substrate is mixed, and see [weld prep](/applications/weld-prep-laser-cleaning-applications) for the fabrication step this feeds.

Specialty

Hastelloy surface prepared by laser cleaning

Hastelloy

View details: Hastelloy. Category: metal. Subcategory: Specialty.

The beam removes weld heat tint and surface oxide from this nickel-chromium-molybdenum grade, clearing the coupon before acid pickling or media blasting would touch the corrosion-resistant surface. The Ni-Cr-Mo composition resists chloride and acid attack rather than forming the flaking [iron oxide](/contaminants/iron-oxide-rust-laser-cleaning) that builds on carbon steel, so cleaning targets a thin passivation layer, not a rust job. Hastelloy is not [Inconel](/materials/inconel-laser-cleaning): Inconel's nickel-chromium-iron makeup targets high-temperature oxidation resistance, while Hastelloy's molybdenum content is built for wet corrosive service, and each alloy carries a different heat-tint color and thickness that changes beam settings. The process also skips electroplated [nickel](/materials/nickel-laser-cleaning) finishes, since a plated layer sits on a different substrate and needs a plating-safe approach instead. Shops reach for it ahead of orbital welding or passivation testing, where residual [weld heat tint](/contaminants/weld-heat-tint-laser-cleaning) would compromise the corrosion resistance the alloy is specified for.

Inconel surface prepared by laser cleaning

Inconel

View details: Inconel. Category: metal. Subcategory: Specialty.

Inconel is cleaned of [oxide scale](/contaminants/oxide-scale-laser-cleaning) below a primary F_damage of 8–20 J/cm², but alloy grade and dust controls still require test coupons, so settings from [stainless steel](/materials/stainless-steel-laser-cleaning) or [titanium](/materials/titanium-laser-cleaning) jobs do not carry over.

Nickel surface prepared by laser cleaning

Nickel

View details: Nickel. Category: metal. Subcategory: Specialty.

Nickel in the shop is either solid stock or bar, or a thin plated layer bonded to steel for corrosion resistance. Laser cleaning removes oxide, tarnish, and surface contamination from either form without media blasting or chemical stripping. It is not a stand-in for cleaning [Hastelloy](/materials/hastelloy-laser-cleaning) or [Inconel](/materials/inconel-laser-cleaning): those are nickel-based superalloys with heavy chromium and molybdenum content that change how the surface absorbs and sheds heat, so parameters that clear plain nickel can underclean or overheat an alloy surface. Once the tarnish layer is gone, bare nickel reflects far more of the beam than the dulled surface did, so a pass that worked at the start can waste energy by the end. On plated parts over [steel](/materials/steel-laser-cleaning), the process has to stop at the plating and not cut through into the substrate, since that thin layer is the corrosion barrier the part depends on.

Titanium surface prepared by laser cleaning

Titanium

View details: Titanium. Category: metal. Subcategory: Specialty.

Commercially pure titanium carries a thin native oxide that a pulsed laser can take off without driving oxygen into the bulk. The issue that matters is staying below energy high enough to hurt the metal while still removing the oxide. Heat from short pulses stays at the surface. That is why this job is not the same as a long soak in a furnace. Commercially pure stock is not the same map as an alloy grade. Titanium dust capture belongs on.

Oxide Layer Dynamics in Metal Laser Cleaning

A fascinating little-known relationship exists in metals: the laser cleaning threshold of the oxide layer is often significantly lower than the base metal, creating a natural self-stopping mechanism that protects the surface, especially pronounced in stainless steel and titanium.

Thermal Conductivity Paradox in Metals

High thermal conductivity metals (copper, aluminum) require surprisingly different pulse strategies than low-conductivity ones. The rapid heat dissipation can actually make them harder to clean at low energy levels, leading to a counter-intuitive preference for higher peak power shorter pulses.

Alloying Elements & Laser Absorption Behavior

Chromium, nickel, and molybdenum content in alloys dramatically alters laser absorption and cleaning efficiency. For example, higher chromium stainless steels exhibit cleaner thresholds due to more uniform oxide layers, a metallurgical relationship rarely documented in laser cleaning guides.

Laser-Induced Passivation on Non-Ferrous Metals

Controlled laser cleaning can simultaneously remove contaminants and create a more stable passive oxide layer than chemical methods, often improving corrosion resistance, turning the cleaning process into a surface treatment step.